Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
Scale formation presents a continuous challenge in the oil and gas industry, leading to reduced production rates and increased operational costs. NINGBO INNO PHARMCHEM CO.,LTD. offers advanced chemical solutions, with chelating agents being key players in tackling this pervasive issue. These compounds are specifically designed to complex with metal ions responsible for scale deposition, thereby preventing or dissolving these unwanted mineral formations.
The effectiveness of chelating agents in inorganic scale removal oilfield applications is well-documented. Unlike traditional mineral acids that might be ineffective against certain scale types, such as barium sulfate, chelating agents like Ethylenediaminetetraacetic Acid (EDTA) and its derivatives can efficiently solubilize these deposits. This capability is critical for maintaining the integrity and flow efficiency of pipelines, wellbores, and surface facilities.
The mechanism behind this action involves the formation of stable coordination complexes between the chelating agent and the metal cations (e.g., Ca²⁺, Ba²⁺) that form the scale. This process effectively removes the ions from the scale lattice, leading to its dissolution. The choice of chelating agent, such as those offered by NINGBO INNO PHARMCHEM CO.,LTD., depends on the specific scale composition, temperature, and pH conditions of the reservoir.
In addition to their direct scale removal capabilities, chelating agents are also vital for preventing scale formation in the first place. They can be included in treatment fluids to sequester ions that would otherwise contribute to scaling, particularly in systems where incompatible water sources might mix or where temperature and pressure changes can induce precipitation. This proactive approach is essential for long-term asset protection.
The development of biodegradable and high-temperature stable chelating agents by companies like NINGBO INNO PHARMCHEM CO.,LTD. further enhances their utility in the demanding environments of oil and gas extraction. These advancements allow for more sustainable and effective scale management strategies, ensuring continuous and optimized production. By utilizing these advanced chemical auxiliaries, operators can significantly mitigate the impact of scale on their operations, reinforcing the importance of expert chemical supply in the sector.
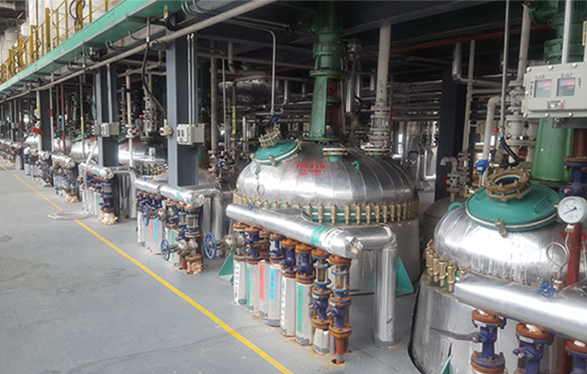
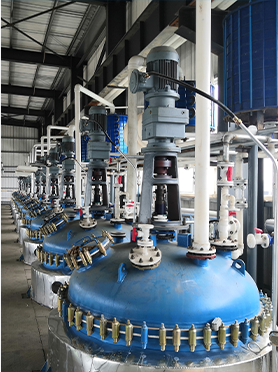
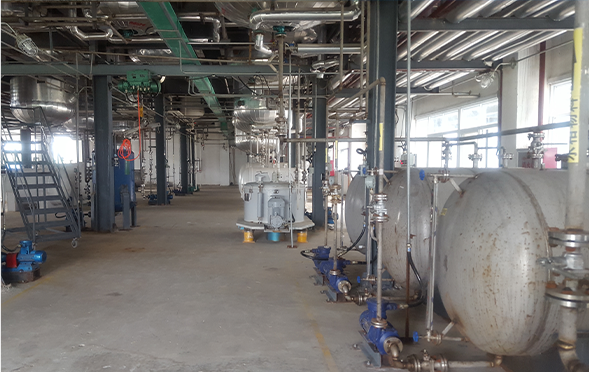
Manufacturing Facilities
Professional Export Experience
to Global Customers
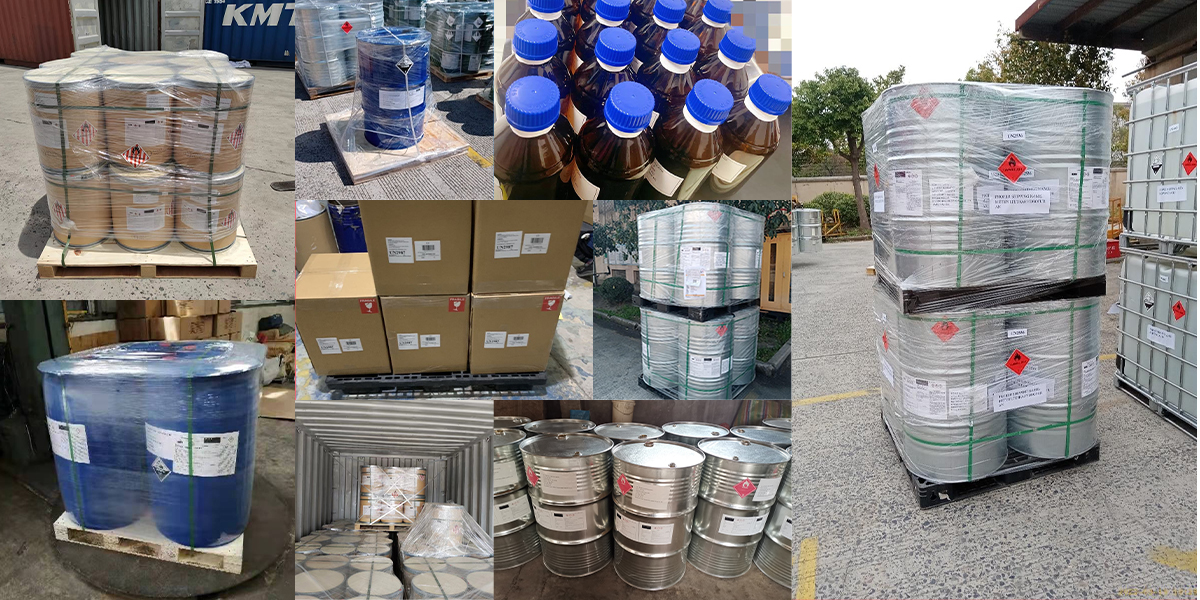
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.