Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
Pyridinium-based ionic liquids, such as 1-Ethylpyridinium Hexafluorophosphate (EtPy PF6), are increasingly recognized for their superior performance characteristics in a variety of industrial applications. As a chemical manufacturer and supplier, we are committed to highlighting the advantages that make these compounds indispensable for modern industries. Understanding these benefits is crucial for procurement managers and formulation chemists looking to optimize their processes and product quality.
The structural design of pyridinium cations offers inherent advantages over other ionic liquid families. Unlike imidazolium-based ionic liquids, the absence of a readily protonatable C2 carbon in pyridinium salts enhances their electrochemical stability, a critical factor for applications in batteries and supercapacitors. Furthermore, the planar, aromatic nature of the pyridinium ring promotes strong π-π interactions, which are beneficial in applications like fuel desulfurization and the selective separation of aromatic compounds. This structural attribute also contributes to their thermal stability and low volatility, aligning with green chemistry principles.
The hexafluorophosphate anion ([PF₆]⁻) further contributes to the desirable properties of compounds like EtPy PF6. It imparts excellent chemical inertness, broad electrochemical windows, and good thermal stability. These attributes make it an ideal candidate for use as an electrolyte in demanding electrochemical devices. For example, in lithium-ion batteries, the stability of the electrode-electrolyte interface is paramount for both performance and safety, and [PF₆]⁻-based ionic liquids often excel in this regard.
When considering industrial applications, the solubility and viscosity profiles of pyridinium hexafluorophosphates are also noteworthy. They typically exhibit good solubility in a range of organic solvents, facilitating their use in various formulations and reaction media. While their viscosity can be higher than some alternatives, this often translates to better handling characteristics and reduced evaporation. For businesses looking to buy these advanced materials, partnering with a reliable supplier in China provides access to high-quality products and competitive pricing, ensuring that these technological advantages can be effectively integrated into their operations.
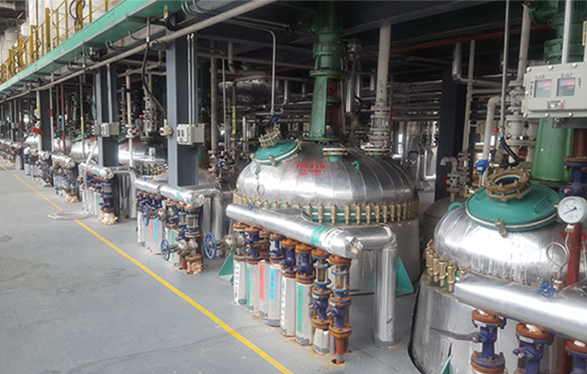
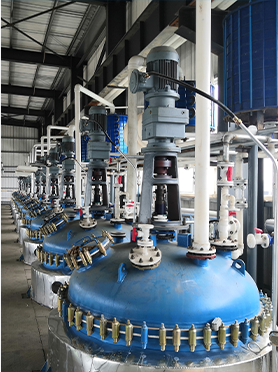
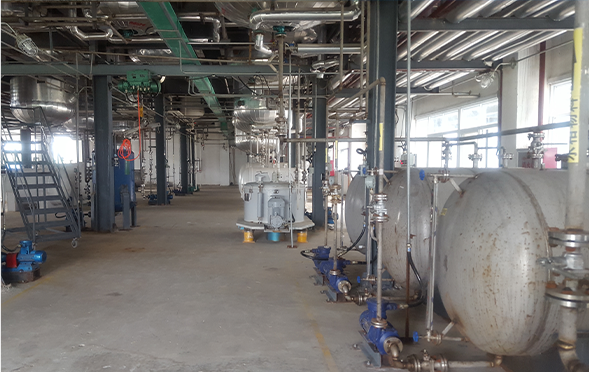
Manufacturing Facilities
Professional Export Experience
to Global Customers
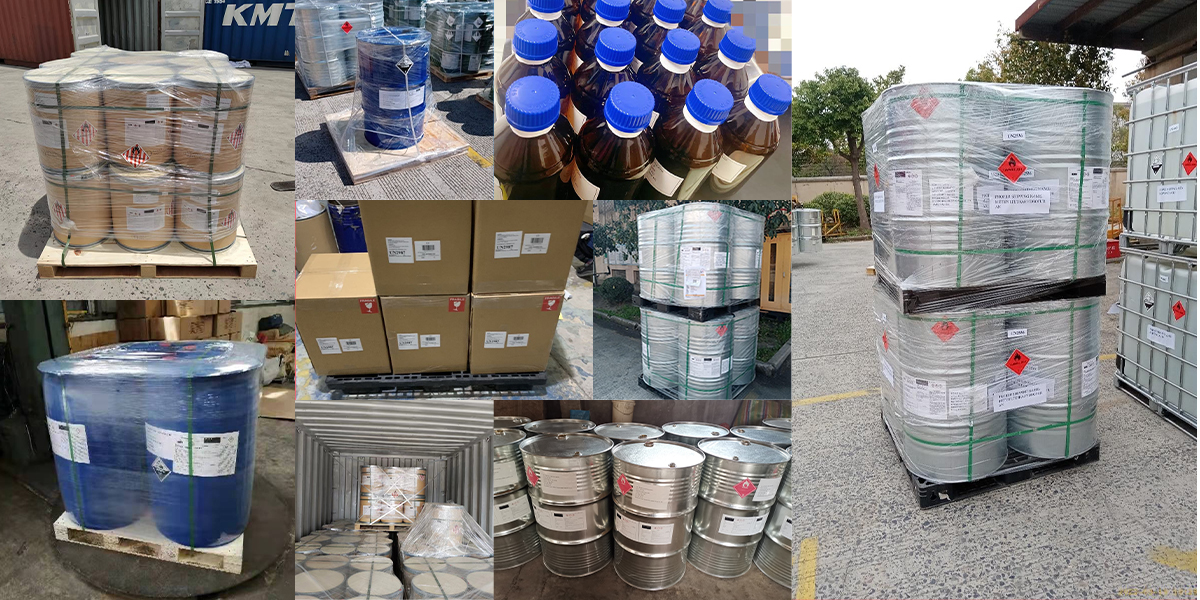
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.