Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
For professionals in the chemical and petrochemical industries, selecting the right catalyst support media is paramount to ensuring process efficiency, catalyst longevity, and overall operational success. Among the various options available, 99% high purity alumina ceramic balls stand out as a superior choice, offering a compelling combination of inertness, mechanical strength, and thermal stability. As a leading manufacturer and supplier, we understand the critical role these balls play in demanding applications.
The primary function of catalyst support media is to provide a stable and inert environment for catalytic reactions. This involves distributing process fluids (gases and liquids) evenly, preventing the catalyst from becoming fouled or poisoned, and protecting it from physical damage due to pressure or flow dynamics. Our 99% alumina ceramic balls excel in these areas due to their meticulously controlled composition and manufacturing process.
The high alumina content (≥99%) of these ceramic balls translates directly into exceptional chemical inertness. This means they are highly resistant to attack from strong acids, alkalis, and other corrosive chemicals commonly found in industrial processes. Unlike lower-purity materials, high-purity alumina minimizes the risk of leaching impurities that could deactivate the catalyst or contaminate the end product. This inertness is vital for applications where product purity is non-negotiable, making them an ideal buy for sensitive chemical synthesis.
In the harsh conditions of chemical reactors, materials must withstand significant mechanical stress and extreme temperatures. Our 99% alumina ceramic balls are engineered with high mechanical strength and excellent resistance to thermal shock. They can operate reliably at temperatures up to 1600°C, ensuring consistent performance even in the most demanding high-temperature services. This durability translates into fewer replacements and reduced operational downtime, offering a clear cost-benefit for purchasers seeking long-term value.
The spherical shape and uniform size of our alumina ceramic balls contribute to optimal bed voidage and flow distribution. This facilitates efficient contact between reactants and catalysts, maximizing conversion rates and productivity. Furthermore, their inert nature prevents them from participating in side reactions, ensuring that the focus remains on the desired catalytic process. As a dedicated supplier, we aim to provide solutions that directly enhance your operational efficiency.
These high-purity alumina ceramic balls are indispensable in a wide array of industries, including petroleum refining, chemical synthesis, fertilizer production, and natural gas processing. They are commonly used as catalyst support media, tower packing, and inert bed fillers in reactors, reformers, and separation columns. We are proud to offer these critical materials at competitive prices, with flexible ordering options for bulk purchases. Contact us today to request a quote and discuss your specific needs; as a trusted manufacturer, we are ready to supply you with the highest quality catalyst support solutions.
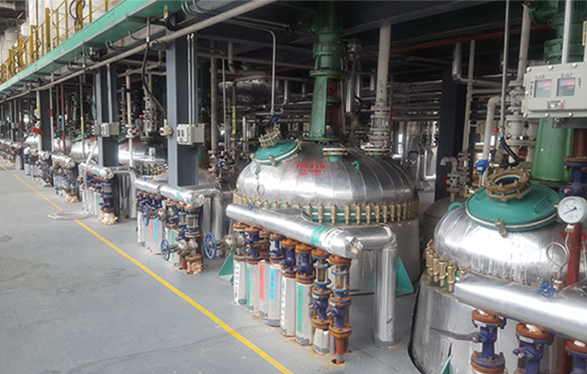
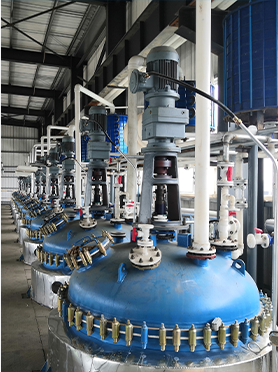
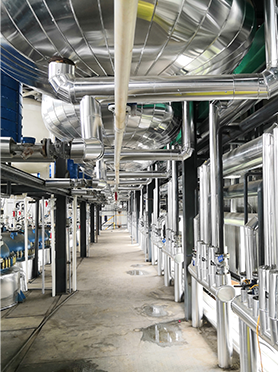
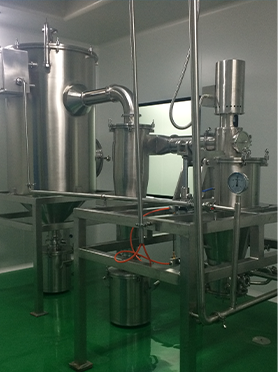
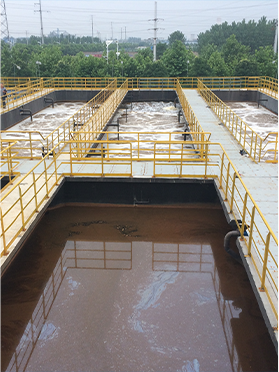
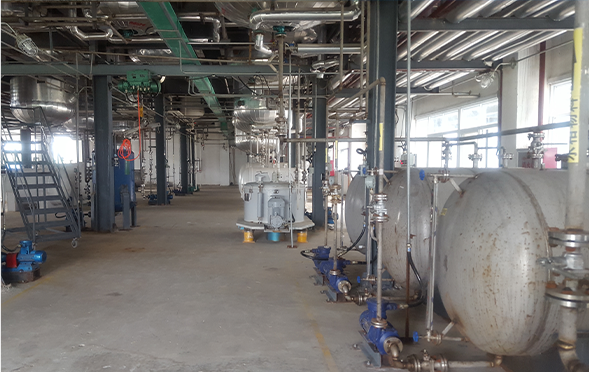
Manufacturing Facilities
Professional Export Experience
to Global Customers
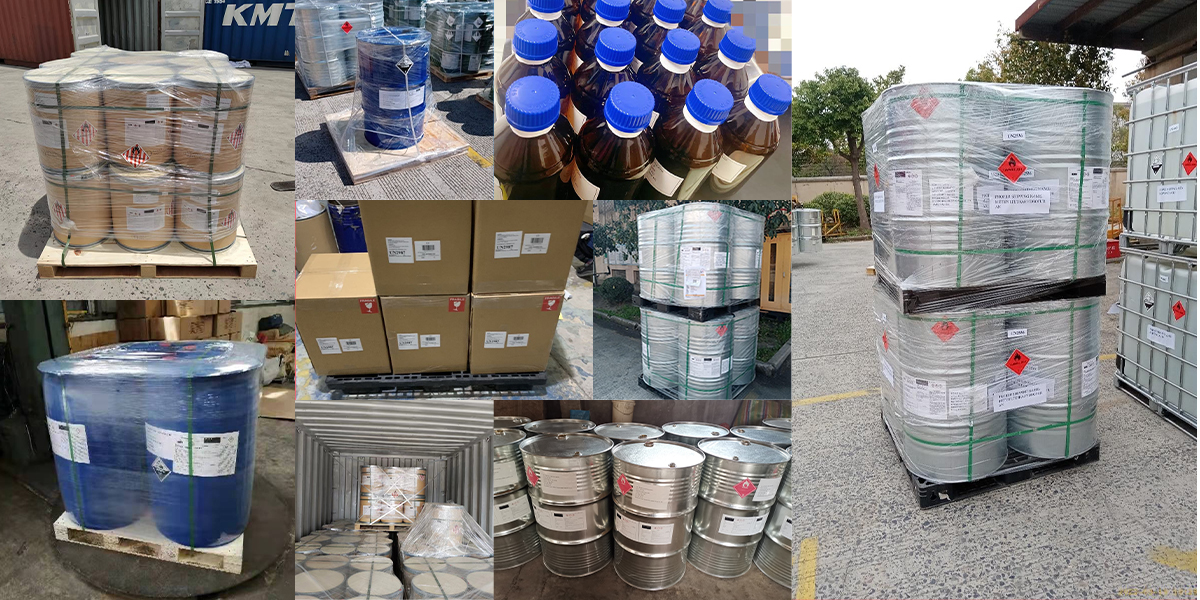
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.