Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
The selection of appropriate flame retardants is a critical decision for plastic manufacturers aiming to meet safety standards and market demands. For widely used polymers like polypropylene (PP) and polyethylene (PE), a range of flame retardant options exist. However, the increasing focus on environmental sustainability and health concerns has led to a re-evaluation of traditional chemistries and the emergence of advanced alternatives. Piperazine Pyrophosphate (PPAP) is a prime example of such an advancement, offering distinct advantages over older technologies.
Historically, halogenated flame retardants, particularly brominated compounds, were dominant due to their high efficacy and cost-effectiveness. These often worked by releasing halogen radicals in the gas phase, which scavenged highly reactive radicals initiating the combustion process. However, their drawbacks are significant: environmental persistence, bioaccumulation, and the potential release of toxic byproducts like dioxins and furans when burned. For PP and PE applications, the use of these compounds is increasingly restricted and phased out.
Another common flame retardant system for polyolefins involves ammonium polyphosphate (APP) combined with a carbonizing agent, such as pentaerythritol (PER) or melamine polyphosphate (MPP). While effective, APP-based systems can sometimes suffer from issues like migration, hydrolytic instability, and potential for blooming (surface crystallization). Furthermore, achieving stringent flame retardancy ratings like UL94 V-0 at thin sections might require high loading levels, which can negatively impact the mechanical properties and processability of PP and PE.
Piperazine Pyrophosphate (PPAP) offers a compelling alternative by addressing many of these limitations. As a halogen-free, nitrogen-phosphorus synergistic intumescent flame retardant, PPAP works by forming a stable, insulating char layer. Its advantages include:
While PPAP might have a higher initial cost per kilogram compared to some older, commodity flame retardants, its overall performance benefits often justify the investment. The ability to use lower loadings, reduce processing issues, meet stringent safety standards, and enhance the environmental profile of the final product makes PPAP a superior choice for many PP and PE applications. As the industry continues to prioritize safety and sustainability, PPAP is poised to become a more dominant flame retardant solution.
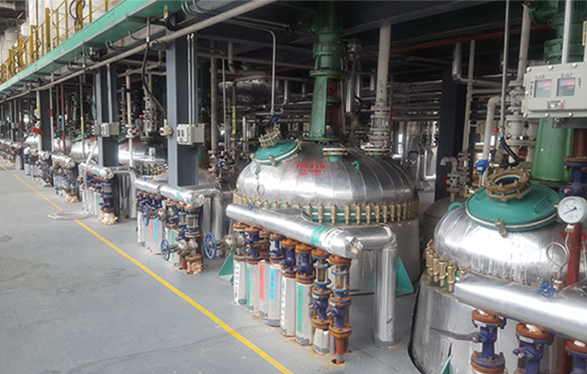
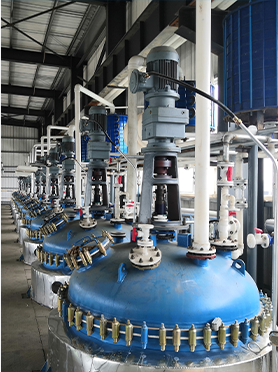
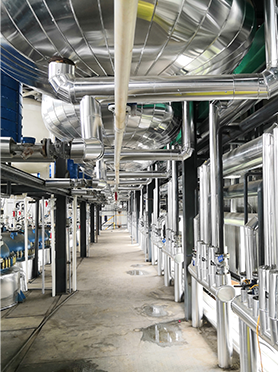
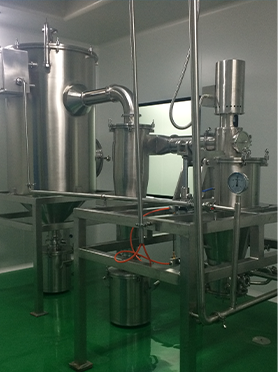
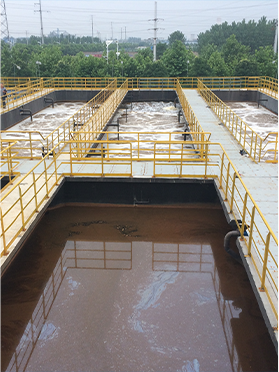
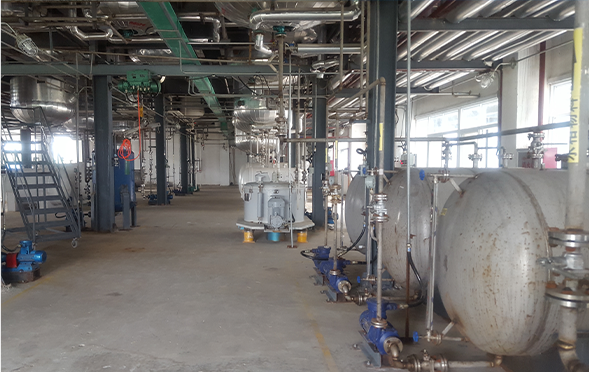
Manufacturing Facilities
Professional Export Experience
to Global Customers
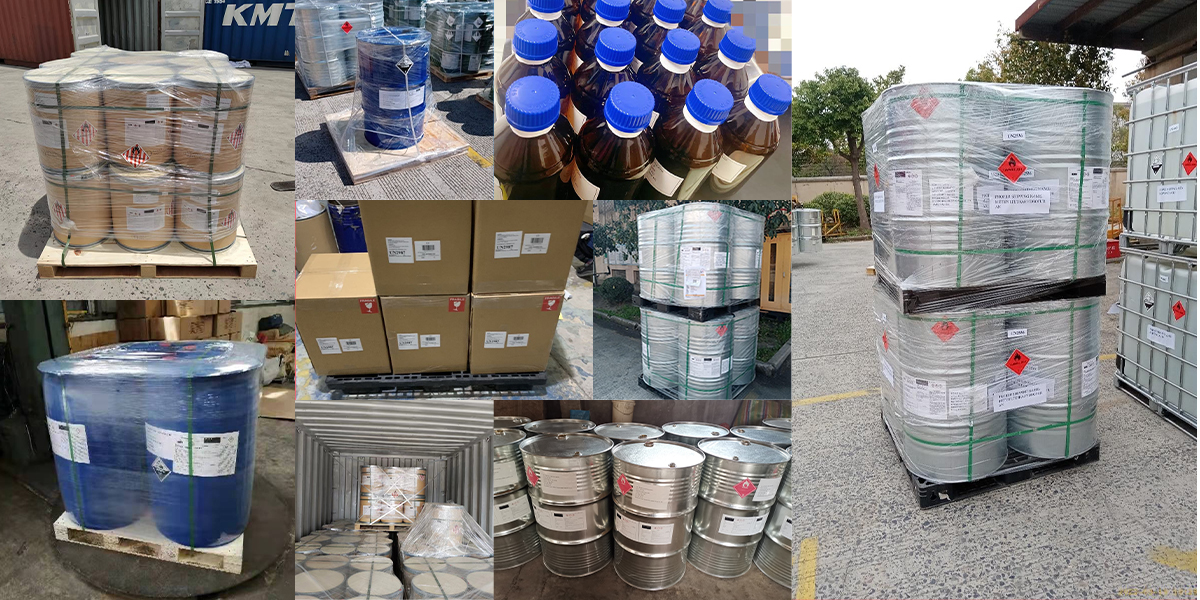
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.