Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
In today's industrial landscape, efficiency and cost-effectiveness are paramount, especially in critical areas like water treatment. For procurement professionals and plant managers, identifying solutions that offer both high performance and economic benefits is a constant pursuit. Coal-based activated carbon, especially in granular form, presents a compelling case as a smart purchase for a wide range of water purification needs. As a leading manufacturer and supplier of water treatment chemicals, we aim to shed light on why this product is an excellent investment.
The fundamental advantage of coal-based activated carbon lies in its inherent properties and production economics. Derived from high-quality anthracite, it undergoes advanced processing to create a material with a highly developed pore structure and a substantial specific surface area, often reaching 950 m²/g. This leads to high adsorption capacities, enabling it to effectively remove organic matter, chlorine, heavy metals, and other contaminants from water. When you are looking to buy activated carbon for water purification, its ability to handle diverse impurities efficiently translates directly into better treated water quality and potentially lower overall treatment costs.
Furthermore, the regenerability of coal-based granular activated carbon significantly enhances its cost-effectiveness. Unlike single-use filtration media, activated carbon can often be regenerated through thermal or chemical processes, restoring its adsorptive capacity. This reduces the frequency of replacement, leading to considerable savings in material costs and waste disposal. For industrial facilities such as power plants, food processing units, or pharmaceutical manufacturers, the ability to regenerate the activated carbon bed is a major advantage for long-term operational budgeting. Investing in a product from a reputable manufacturer ensures consistent quality for effective regeneration cycles.
The specific applications where coal-based activated carbon proves particularly economical are numerous. In municipal water treatment, it’s vital for enhancing taste and odor. In industrial circulating water systems, it helps prevent scaling and fouling, protecting expensive equipment. Even in specialized areas like seawater breeding or beverage production, its purification capabilities are indispensable. When considering bulk purchases, working with a China supplier known for competitive pricing and consistent quality can further amplify the cost savings. The pricing typically ranges from $780.00 to $1,750.00 per ton, offering excellent value for the performance delivered.
When selecting a supplier, it’s important to look for manufacturers who provide detailed specifications, such as iodine adsorption values (600-1100 mg/g), particle size distribution (e.g., 4-8 mesh, 8-30 mesh), moisture content (typically <5%), and ash content (<10%). These parameters are crucial indicators of product quality and performance. As a dedicated manufacturer, we ensure these standards are met, providing you with a reliable and cost-effective solution for your water treatment challenges.
In conclusion, coal-based activated carbon is a smart buy for businesses prioritizing both effective water treatment and cost management. Its high adsorption capacity, coupled with its regenerability and the competitive pricing available from manufacturers and suppliers in China, makes it an indispensable component for achieving efficient and economical water purification. For your next purchase, consider the long-term value that high-quality coal-based granular activated carbon can bring to your operations.
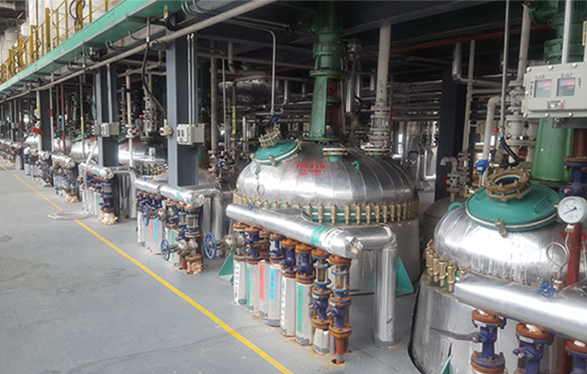
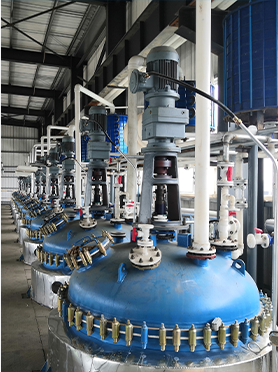
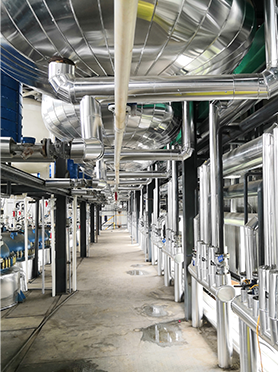
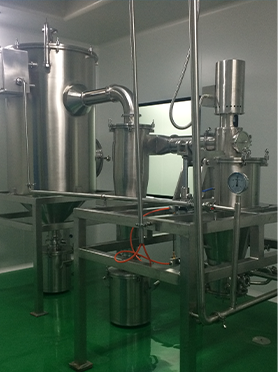
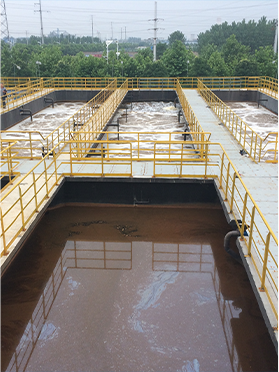
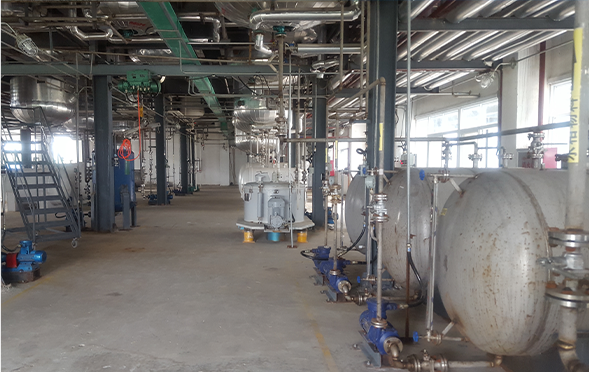
Manufacturing Facilities
Professional Export Experience
to Global Customers
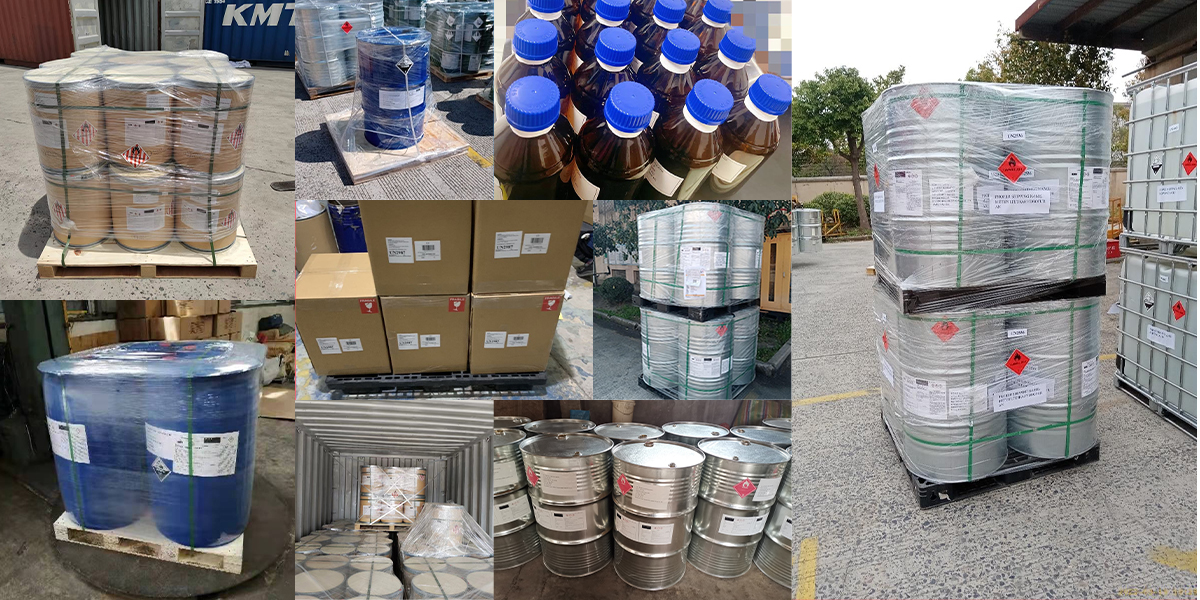
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.