Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
In an era increasingly defined by environmental consciousness and stringent regulatory frameworks, the chemical industry is undergoing a significant transformation. One of the most critical areas of this evolution is the development and adoption of safer, more sustainable materials. Flame retardants, essential for preventing the ignition and spread of fire in polymers and textiles, have been a particular focus. Traditional halogenated flame retardants, while effective, have come under scrutiny for their environmental persistence, potential toxicity, and the release of harmful byproducts during combustion. This has paved the way for the rise of halogen-free alternatives, with Piperazine Pyrophosphate (PPAP) leading the charge in offering environmentally superior flame retardancy.
The concerns surrounding halogenated flame retardants are multi-faceted. Many of these compounds, such as certain brominated flame retardants (BFRs), are bioaccumulative and persistent in the environment. Their breakdown products can be toxic, and during a fire, they can release hazardous gases like dioxins and furans. Regulatory bodies worldwide, including the EU with directives like RoHS (Restriction of Hazardous Substances) and REACH (Registration, Evaluation, Authorisation and Restriction of Chemicals), have actively sought to restrict or ban many of these substances. This has created a strong market pull for alternatives that meet performance requirements without posing undue risks to human health or the environment.
Piperazine Pyrophosphate emerges as a strong contender in the halogen-free segment. Its formulation, based on a synergistic combination of phosphorus and nitrogen, allows it to function as an intumescent flame retardant. This mechanism is inherently cleaner, as it promotes char formation rather than releasing potentially harmful volatile compounds. The char acts as a physical barrier, insulating the material and limiting the flow of heat and fuel to the flame. This process results in significantly reduced smoke generation and the absence of corrosive acidic gases often associated with halogenated compounds.
The environmental benefits extend beyond the combustion phase. PPAP itself is designed for minimal ecological impact. Its low moisture absorption and resistance to hydrolysis contribute to its stability, preventing leaching into soil and water systems. Furthermore, the production processes for such advanced materials are increasingly optimized for reduced environmental footprint, adhering to stricter chemical manufacturing standards. This holistic approach to sustainability makes PPAP a responsible choice for manufacturers aiming to reduce their environmental impact.
The transition to halogen-free flame retardants like PPAP is not just an environmental imperative; it also presents significant market opportunities. Consumers and businesses are increasingly demanding products that are both safe and eco-friendly. By incorporating PPAP into their polymer formulations, companies can enhance their brand image, meet evolving customer expectations, and gain a competitive edge in a market that is increasingly prioritizing sustainability. This includes applications in sensitive sectors like electronics, automotive interiors, and consumer goods, where material safety and environmental impact are closely scrutinized.
In conclusion, the move from halogenated to halogen-free flame retardants is a critical step towards a more sustainable chemical industry. Piperazine Pyrophosphate stands as a prime example of how innovation can deliver high performance without compromising environmental integrity. By understanding and adopting these advanced materials, industries can contribute to a safer, healthier planet while continuing to develop high-quality, fire-resistant products.
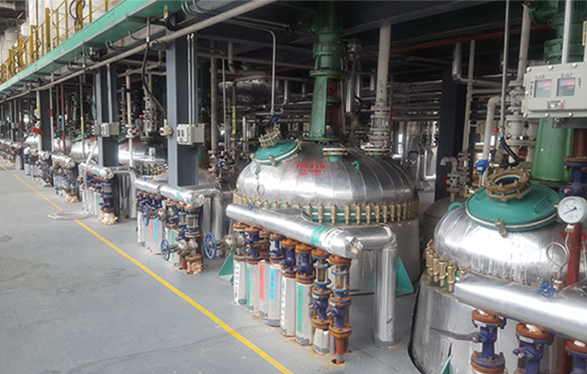
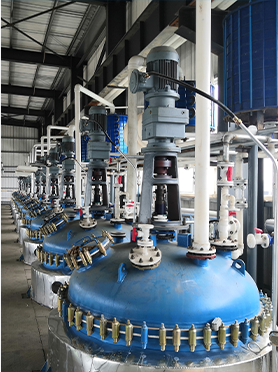
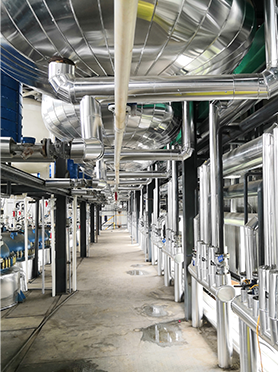
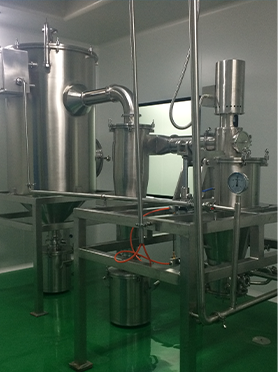
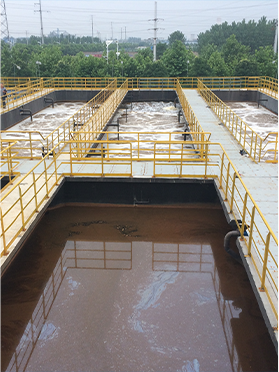
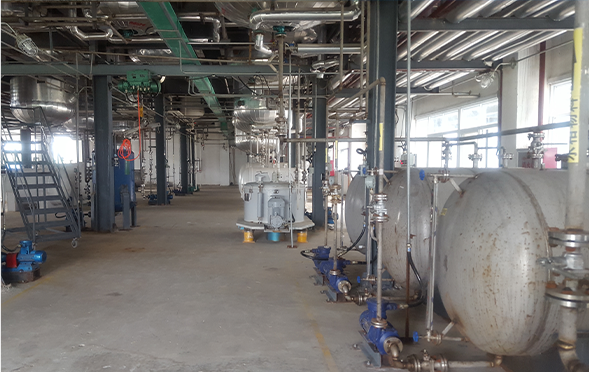
Manufacturing Facilities
Professional Export Experience
to Global Customers
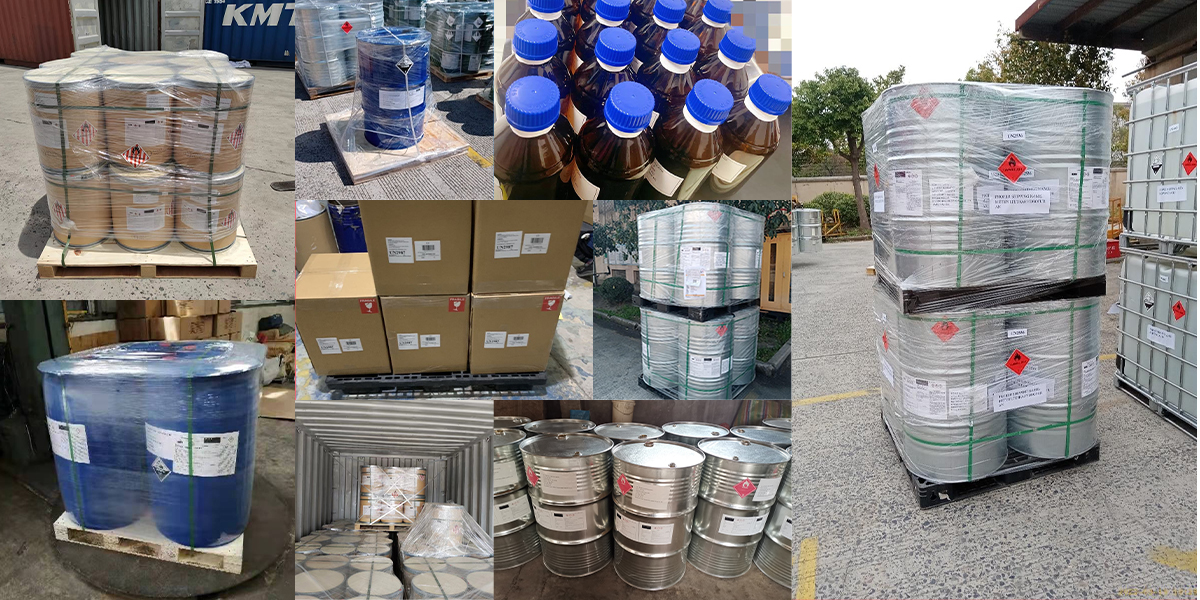
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.