Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
The pharmaceutical industry operates under exceptionally stringent quality and safety standards. Maintaining the efficacy and stability of medications is paramount, and even minute fluctuations in environmental conditions can have significant consequences. One of the most persistent challenges is controlling moisture, which can lead to the degradation of active pharmaceutical ingredients (APIs), excipients, and packaging materials. This is where high-quality silica gel plays an indispensable role. As a leading manufacturer and supplier, we provide pharmaceutical-grade silica gel that meets the rigorous demands of this sector.
Why is Moisture Control Crucial in Pharmaceuticals?
Many pharmaceutical formulations, whether solid dosage forms (tablets, capsules) or sensitive biologicals, are hygroscopic. This means they readily absorb moisture from the atmosphere. When exposed to humidity, these products can undergo a variety of detrimental changes:
To combat these issues, pharmaceutical manufacturers rely on desiccants like silica gel to maintain a stable, low-humidity internal environment within the product packaging. Purchasing reliable silica gel from a trusted supplier is a critical step in ensuring product quality and patient safety.
Our Silica Gel: Engineered for Pharmaceutical Excellence
As a dedicated silica gel manufacturer and supplier, we understand the unique requirements of the pharmaceutical industry. Our silica gel is produced under strict quality control protocols, ensuring:
Applications in Pharmaceutical Packaging
Our silica gel is widely used in:
Invest in Quality, Ensure Safety
For pharmaceutical companies, the choice of desiccant is not just about preventing moisture; it's about safeguarding patient health. By sourcing high-quality silica gel from a reputable manufacturer and supplier like us, you ensure the stability, efficacy, and safety of your pharmaceutical products. We invite you to inquire about our pharmaceutical-grade silica gel and discuss how our solutions can enhance your product's shelf life and market readiness. Partner with us to secure the best in moisture control for your vital medications.
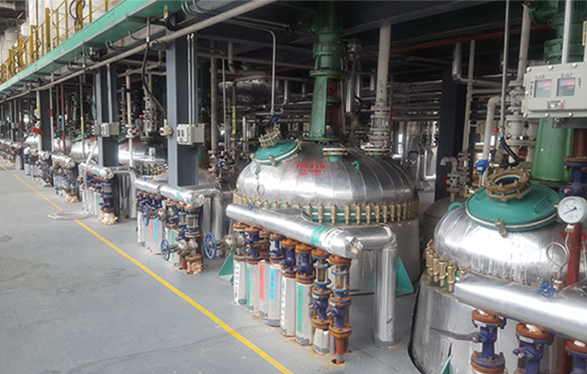
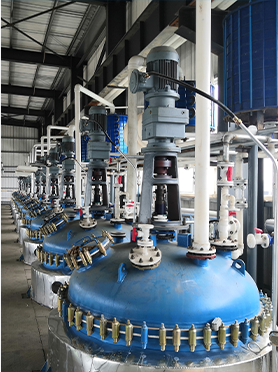
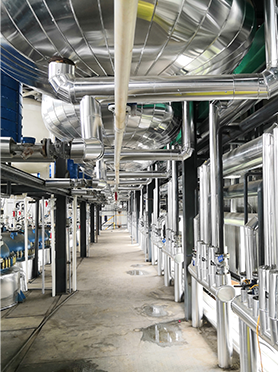
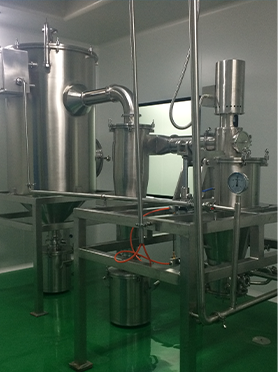
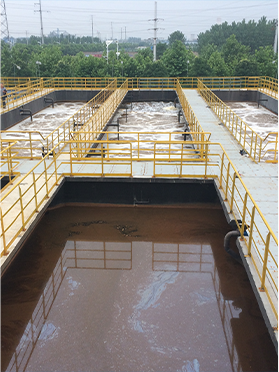
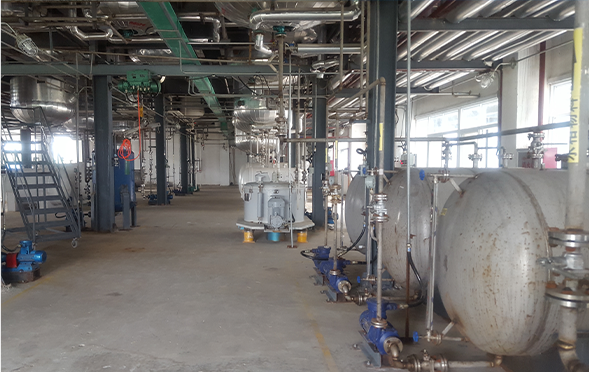
Manufacturing Facilities
Professional Export Experience
to Global Customers
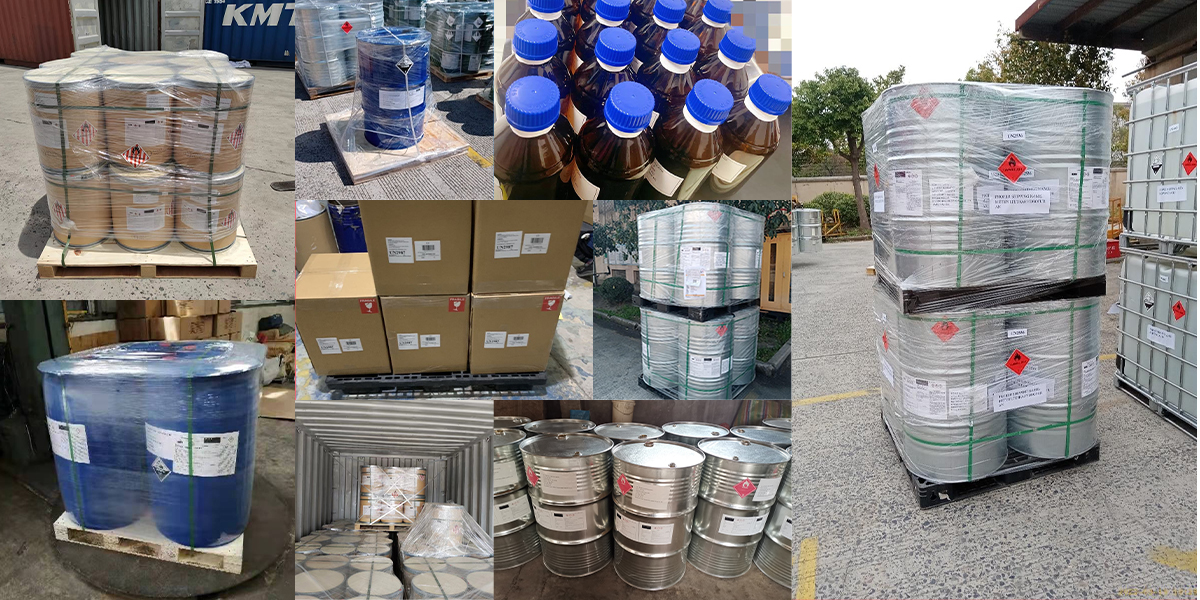
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.