Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
High-temperature reactors are the backbone of many industrial chemical processes, from ammonia synthesis to petrochemical cracking. The materials used within these reactors must withstand extreme thermal stress and often corrosive chemical environments. In this demanding landscape, 99% inert alumina balls have emerged as a vital component, offering unparalleled performance as catalyst support and bed media. As a seasoned manufacturer and supplier, we highlight the indispensable role of these advanced ceramic materials.
Reactors operating at elevated temperatures (often exceeding 1000°C) require materials that maintain their structural integrity and chemical inertness. Catalysts used in these processes are frequently sensitive to impurities and thermal degradation. Therefore, the supporting media must be robust enough to provide physical support without reacting with the process stream or the catalyst itself. Lower-grade materials can leach silica or other contaminants, leading to catalyst poisoning, reduced efficiency, and potential damage to downstream equipment. This is where the high-purity nature of our 99% alumina balls truly shines.
The 99% alumina content ensures that these ceramic balls are exceptionally inert. This means they possess very low reactivity with a wide range of chemicals, including acids, alkalis, and steam, even at high temperatures. This chemical stability prevents the leaching of impurities that could compromise the catalyst's activity or the purity of the final product. For industries like ammonia production, where steam reforming is a critical step, the low silica content of high-purity alumina is essential to prevent silica deposition downstream. Purchasing these balls means investing in process purity and reliability.
Beyond chemical inertness, 99% inert alumina balls offer remarkable thermal stability. They can endure prolonged exposure to high temperatures without significant degradation or loss of mechanical properties. Coupled with their high crush strength, this makes them ideal for supporting heavy catalyst beds and withstanding the thermal cycling common in reactor operations. Their ability to resist thermal shock further enhances their suitability for these demanding applications. As a trusted supplier, we ensure our products meet these critical performance criteria, providing you with materials you can depend on.
These inert alumina balls are widely deployed in applications such as secondary reformers, high-temperature shift reactors, and various petrochemical processes including ethylene cracking and drying. Their consistent performance and durability make them a preferred choice for engineers aiming to optimize reactor uptime and catalyst efficiency. We encourage you to buy these essential components from a manufacturer committed to quality and performance. Contact us for a quote and discover how our 99% inert alumina balls can elevate the performance of your high-temperature reactor systems.
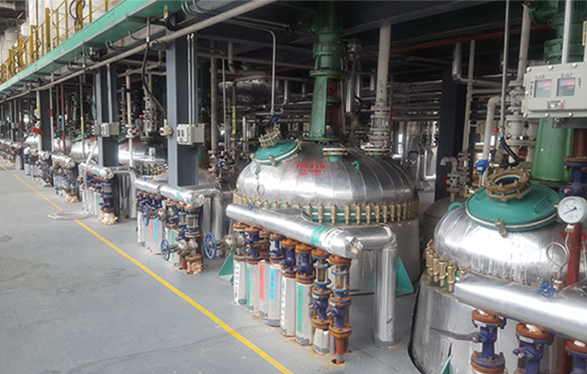
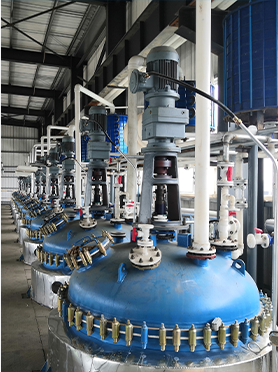
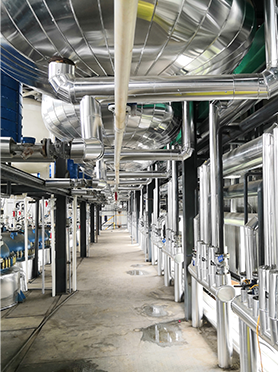
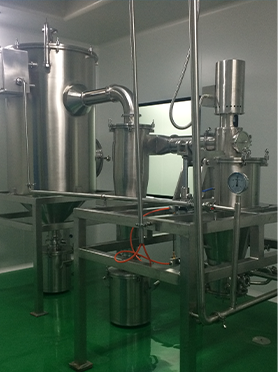
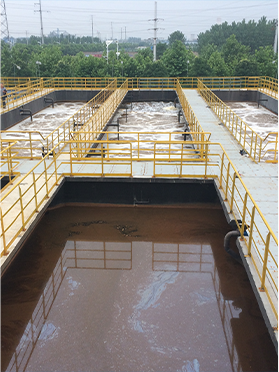
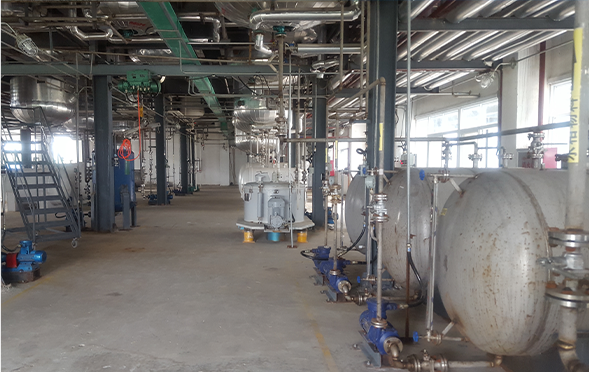
Manufacturing Facilities
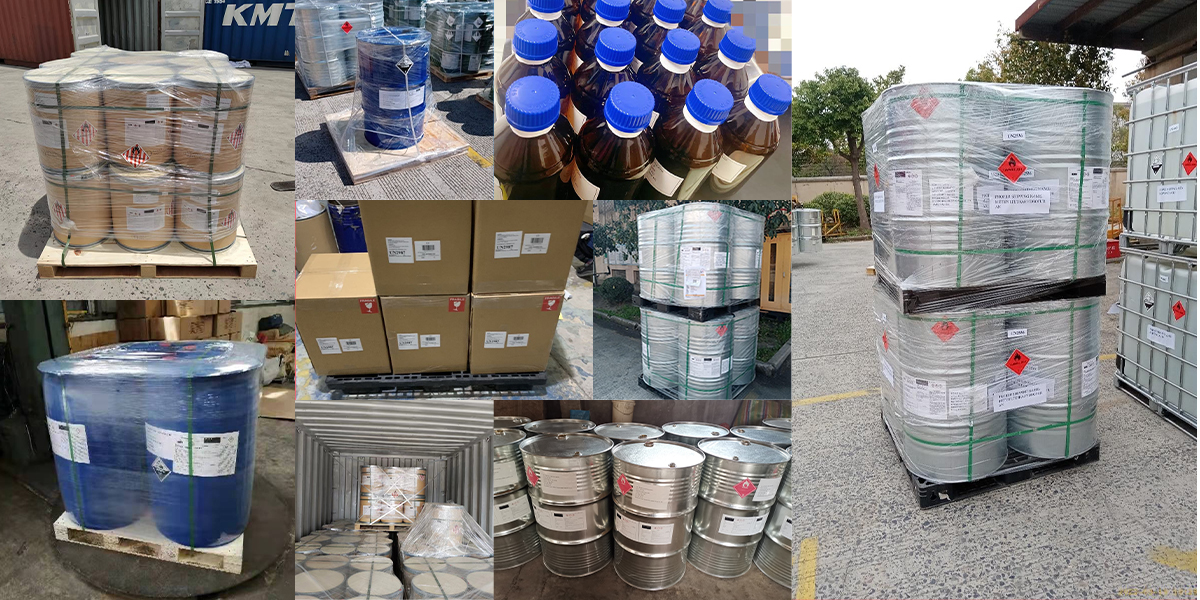
Professional Export Experience
to Global Customers
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.