Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
Industrial water systems, particularly those involving cooling or heating processes, often operate at elevated temperatures. The ability of chemical treatment agents to maintain their efficacy under these thermal stresses is critical for preventing scale, corrosion, and other performance-degrading issues. Organophosphonate copolymer systems are renowned for their exceptional thermal stability, making them a preferred choice for demanding applications. NINGBO INNO PHARMCHEM, a leading manufacturer and supplier, explains why these advanced chemicals are superior.
The Impact of Temperature on Water Treatment Chemicals
Many conventional water treatment chemicals can degrade or lose their effectiveness when exposed to high temperatures. This degradation can lead to:
For industrial facilities that cannot operate at lower temperatures, selecting chemicals with inherent thermal stability is paramount. This is where organophosphonate copolymer systems truly shine.
The Advantage of Organophosphonate Copolymer Systems' Thermal Stability
Organophosphonate copolymer systems are engineered to withstand higher temperatures, allowing them to perform reliably in challenging thermal environments. Their high thermal stability is attributed to the robust molecular structure of both the phosphonate and copolymer components:
When you buy organophosphonate copolymer systems from NINGBO INNO PHARMCHEM, you are procuring a chemical solution built for demanding industrial conditions. Our expertise as a manufacturer and supplier ensures you receive products that deliver consistent performance.
Why Choose NINGBO INNO PHARMCHEM?
As a dedicated provider of advanced water treatment solutions, NINGBO INNO PHARMCHEM offers:
For industries where temperature is a critical factor, the high thermal stability of organophosphonate copolymer systems is a significant advantage. If you are looking to buy effective and reliable water treatment chemicals, contact NINGBO INNO PHARMCHEM today and discover how our products can safeguard your systems even under the most demanding thermal conditions.
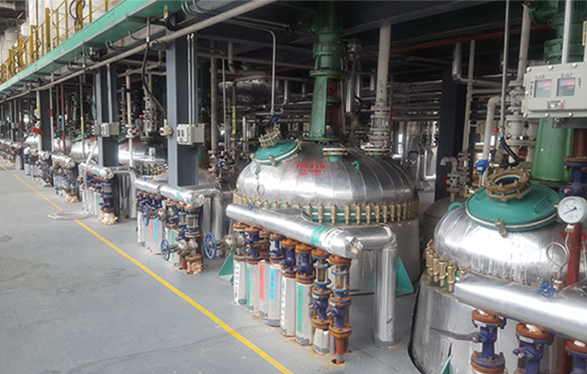
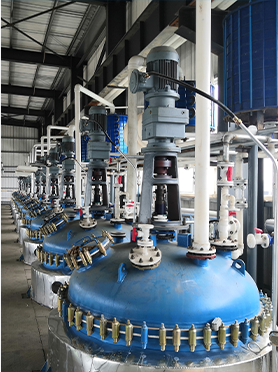
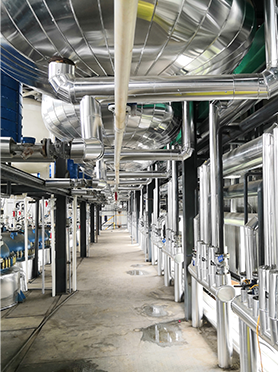
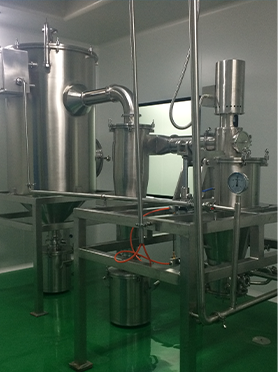
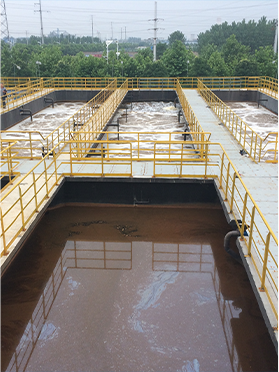
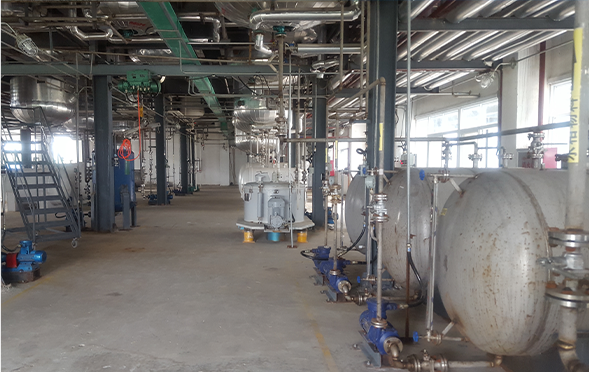
Manufacturing Facilities
Professional Export Experience
to Global Customers
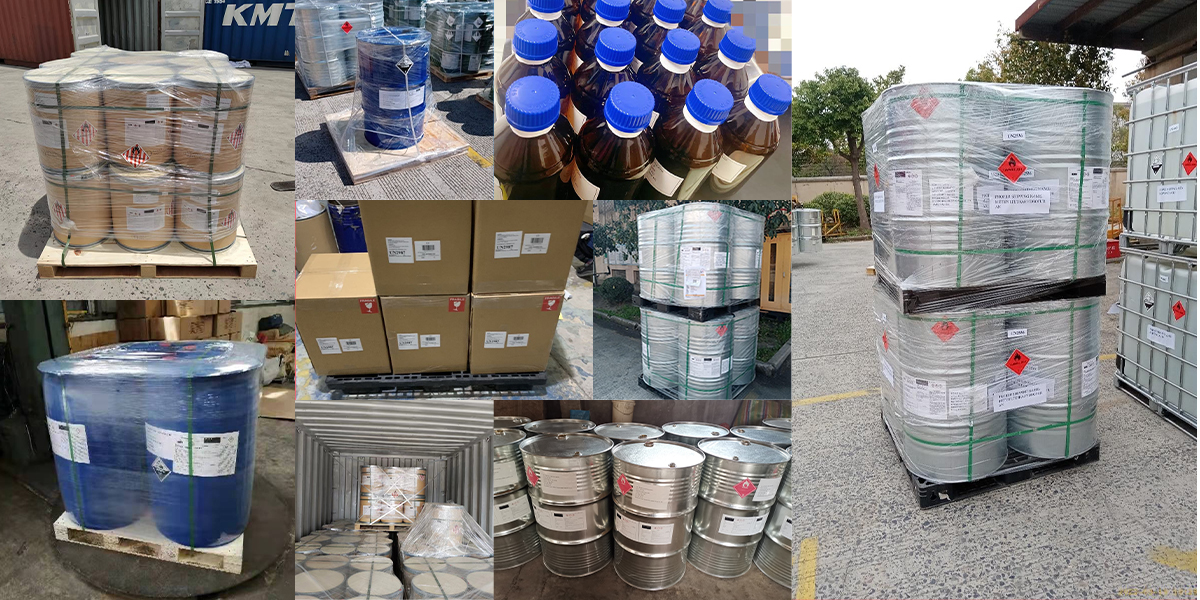
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.