Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
The pharmaceutical industry operates under the strictest quality and purity standards, where even the slightest impurity can have significant consequences. In this highly regulated environment, the choice of solvents and cleaning agents is paramount. 99.9% Isopropyl Alcohol (IPA) emerges as a critical chemical, prized for its potent disinfectant properties, excellent solvency, and rapid evaporation, making it an indispensable component in pharmaceutical manufacturing. NINGBO INNO PHARMCHEM CO.,LTD. is a leading manufacturer and supplier of high-purity Isopropyl Alcohol, ensuring that pharmaceutical companies have access to a reliable and quality-assured product.
Why is High-Purity IPA Essential in Pharmaceuticals?
Pharmaceutical production demands an environment that is free from contaminants, ensuring the safety and efficacy of medications. 99.9% Isopropyl Alcohol plays a multi-faceted role in achieving and maintaining this crucial purity:
The 99.9% purity is crucial because it minimizes the introduction of unwanted substances, such as water or other impurities, which could compromise the integrity of pharmaceutical products or interfere with sensitive manufacturing processes. Sourcing IPA from a reputable supplier in China like NINGBO INNO PHARMCHEM CO.,LTD. guarantees that the product meets the stringent requirements of the pharmaceutical sector.
Key Pharmaceutical Applications:
For pharmaceutical companies, securing a consistent and high-quality supply of 99.9% Isopropyl Alcohol is a matter of regulatory compliance and product safety. NINGBO INNO PHARMCHEM CO.,LTD. understands these demands and offers reliable sourcing, competitive pricing, and expert support to meet your procurement needs. Whether you need to buy IPA in bulk or require tailored solutions, we are your dedicated IPA producer.
In essence, 99.9% Isopropyl Alcohol is a cornerstone chemical in the pharmaceutical industry, contributing significantly to the production of safe, effective, and high-quality medicines. Its versatility and purity make it an indispensable tool for maintaining the rigorous standards of pharmaceutical manufacturing.
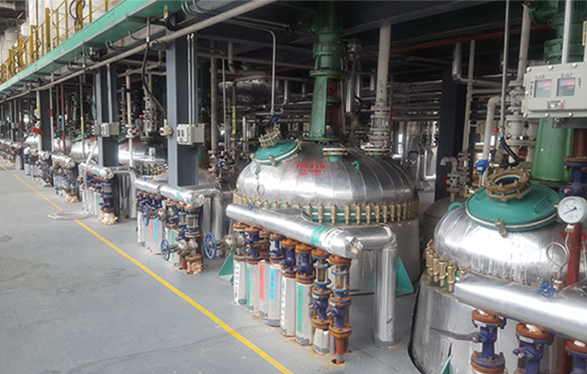
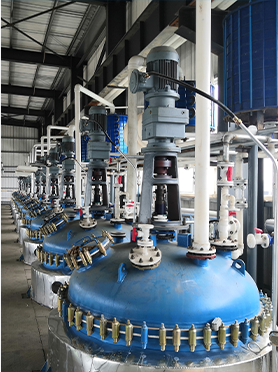
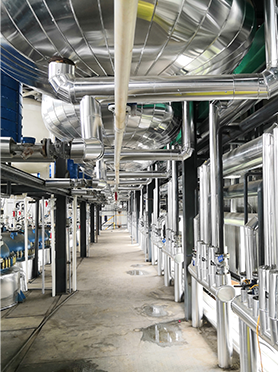
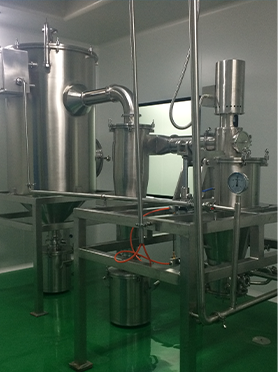
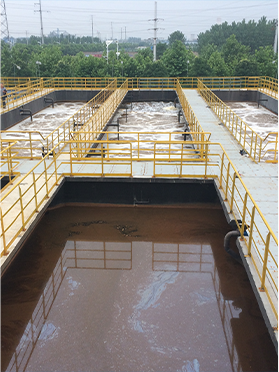
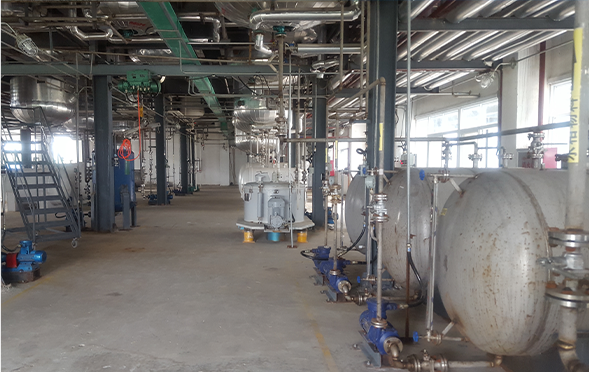
Manufacturing Facilities
Professional Export Experience
to Global Customers
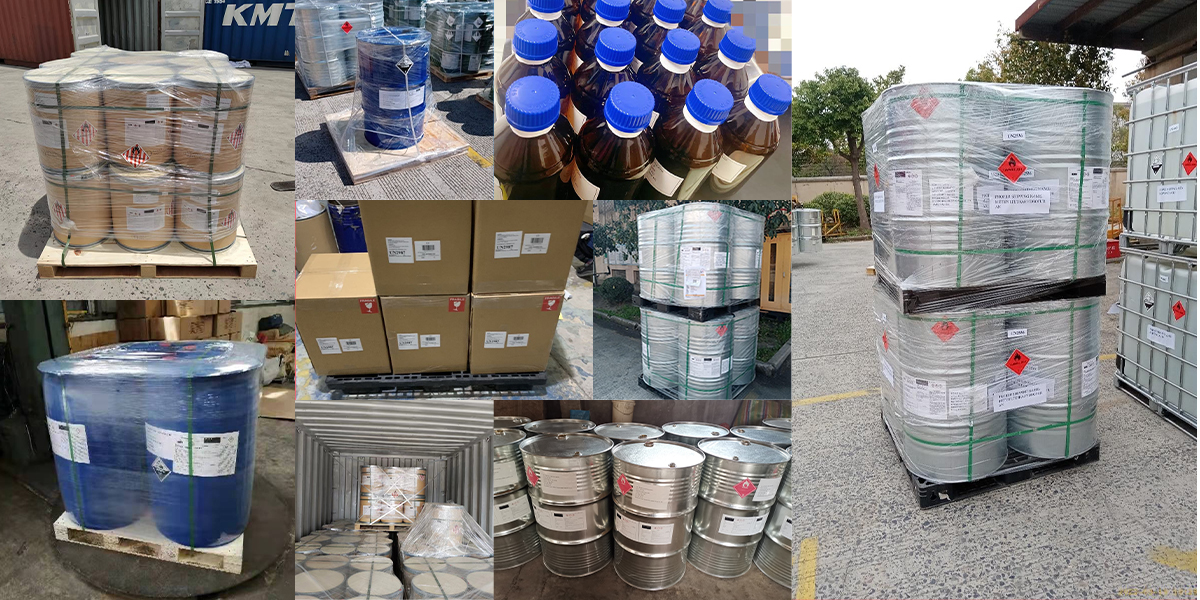
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.