Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
In today's increasingly safety-conscious world, the demand for effective flame retardant materials is on the rise across numerous industries. Melamine, a versatile organic compound (CAS 108-78-1), has emerged as a critical component in the development of advanced, non-halogenated flame retardant systems. As a leading chemical manufacturer, we understand the significance of Melamine's unique properties in enhancing fire safety and performance in a wide range of applications.
Melamine's effectiveness as a flame retardant stems primarily from its high nitrogen content, which constitutes approximately 66% of its molecular mass. When exposed to heat, Melamine undergoes sublimation or decomposition, a process that absorbs significant thermal energy. This endothermic reaction acts as a heat sink, cooling the material and slowing down the combustion process. Furthermore, the decomposition releases nitrogen gas, which dilutes flammable gases and reduces the concentration of oxygen available to the fire, thereby inhibiting flame propagation.
Unlike traditional halogenated flame retardants, Melamine-based systems offer an environmentally friendlier alternative. They do not produce toxic or corrosive by-products when burned, which is a growing concern in regulatory and consumer circles. This makes Melamine an attractive choice for manufacturers seeking to comply with stricter environmental regulations and meet market demands for safer products.
Melamine is extensively used in conjunction with other synergistic compounds, such as ammonium polyphosphate (APP) and pentaerythritol, to create highly effective intumescent flame retardant systems. These systems work by forming a protective char layer on the surface of the material when exposed to fire. This char acts as a barrier, insulating the underlying material from heat and oxygen, and preventing the release of flammable volatiles. You can buy Melamine powder from us to formulate these advanced intumescent coatings, plastics, and textiles.
Industries that benefit from Melamine's flame retardant properties include automotive, construction, electronics, and textiles. Its incorporation into polymers, paints, and fabric treatments significantly improves their fire safety characteristics. As a reliable Melamine supplier, we provide the high-purity industrial grade Melamine necessary for achieving optimal flame retardant performance in your specific applications. Partner with us to enhance the safety and marketability of your products.
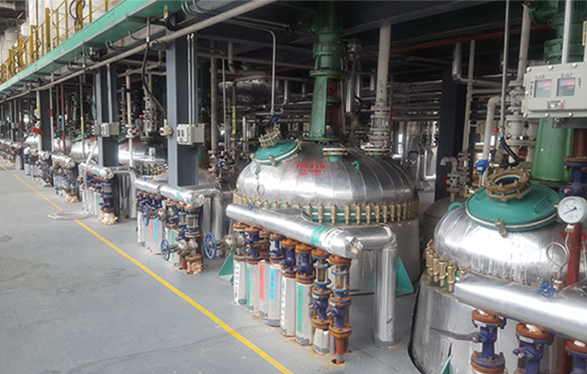
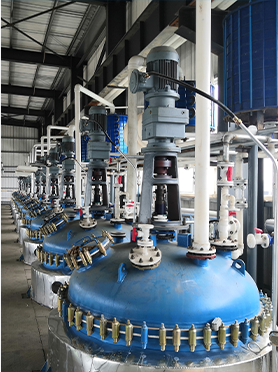
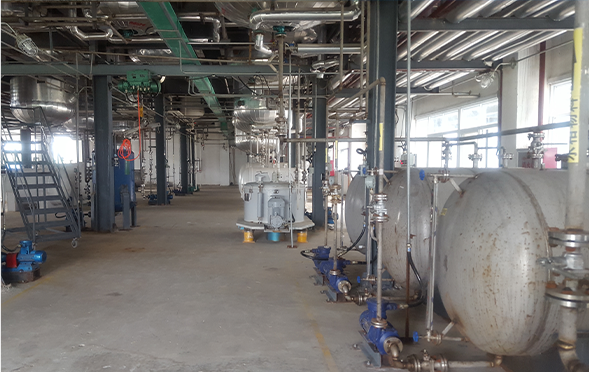
Manufacturing Facilities
Professional Export Experience
to Global Customers
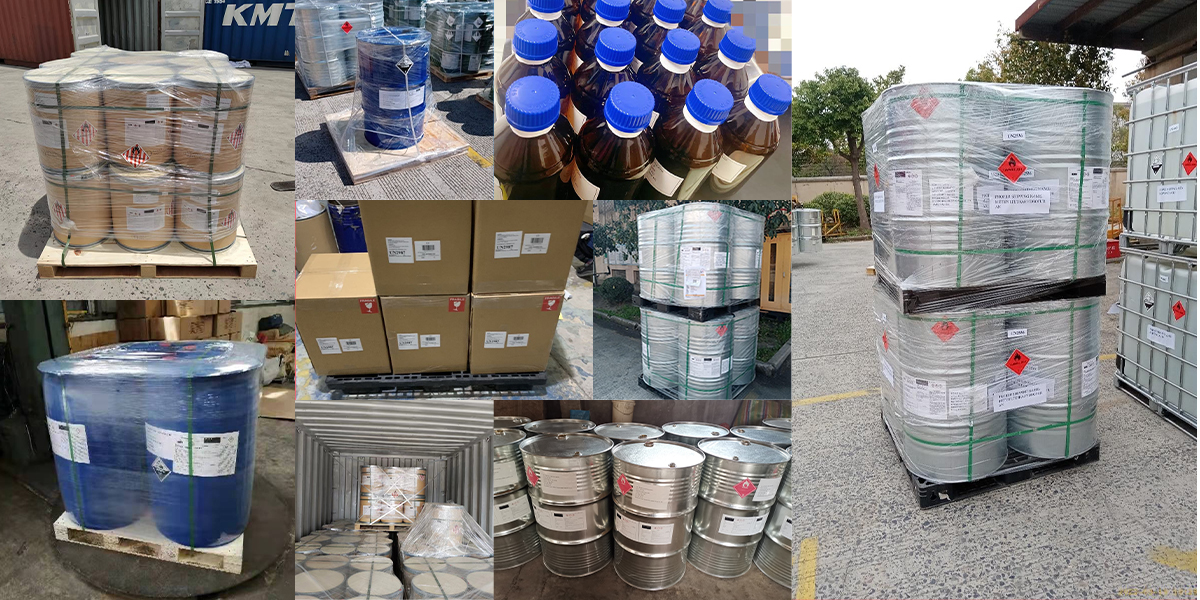
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.