Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
For R&D scientists in the polymer and materials science fields, understanding the intricate properties and mechanisms of chemical additives is fundamental to innovation. Methyl Octabromoether (CAS 97416-84-7) is a sophisticated brominated flame retardant that warrants a closer technical examination. This deep dive aims to provide researchers and formulators with critical insights into its chemical characteristics and performance attributes.
Chemical Structure and Properties
Methyl Octabromoether, chemically identified as Tetrabromobisphenol A bis(2,3-dibromo-2-methylpropyl) ether, boasts a complex molecular structure C23H24Br8O2. Its most significant feature is the presence of eight bromine atoms within the molecule, contributing to its high molecular weight (approximately 971.67 g/mol) and its potent flame retardant capabilities. The compound typically presents as a white powder or granules, with a melting point generally ranging from 90-125°C. Its solubility in common organic solvents like acetone and esters facilitates its incorporation into various polymer systems.
Mechanism of Flame Retardancy
As a brominated flame retardant, Methyl Octabromoether primarily operates in the gas phase during combustion. When a material containing this additive is exposed to heat, the C-Br bonds break, releasing bromine radicals. These highly reactive bromine radicals then scavenge the high-energy hydrogen and hydroxyl radicals (H• and OH•) that are crucial for sustaining the flame propagation cycle. This process effectively interrupts the exothermic chain reactions of combustion, leading to flame inhibition. The high bromine content ensures a sufficient concentration of these radicals is available to quench the flame efficiently.
Key Performance Indicators for R&D Evaluation
When evaluating Methyl Octabromoether for new product development, R&D scientists typically focus on:
Applications and Future Trends
Methyl Octabromoether's effectiveness as an HBCD replacement has made it a cornerstone in the development of safer fire-resistant materials, particularly for insulation foams used in buildings. Its application extends to improving the fire safety of polypropylene, polyethylene, and other engineering plastics, as well as in textile treatments. As regulations evolve and the demand for high-performance, environmentally conscious flame retardants grows, Methyl Octabromoether is well-positioned to remain a key component in the materials science toolkit. Researchers exploring novel polymer composites or seeking to meet stringent new fire safety standards should consider its technical merits. Sourcing from reliable chemical manufacturers ensures access to material meeting these exacting technical requirements.
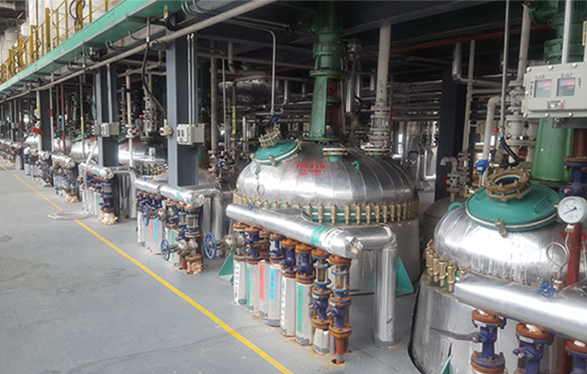
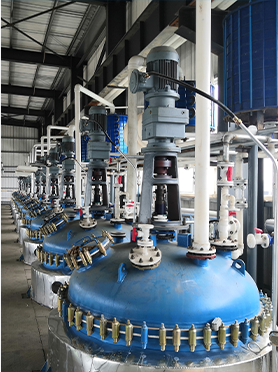
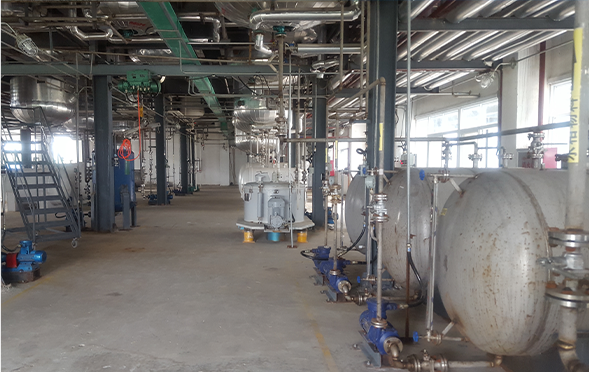
Manufacturing Facilities
Professional Export Experience
to Global Customers
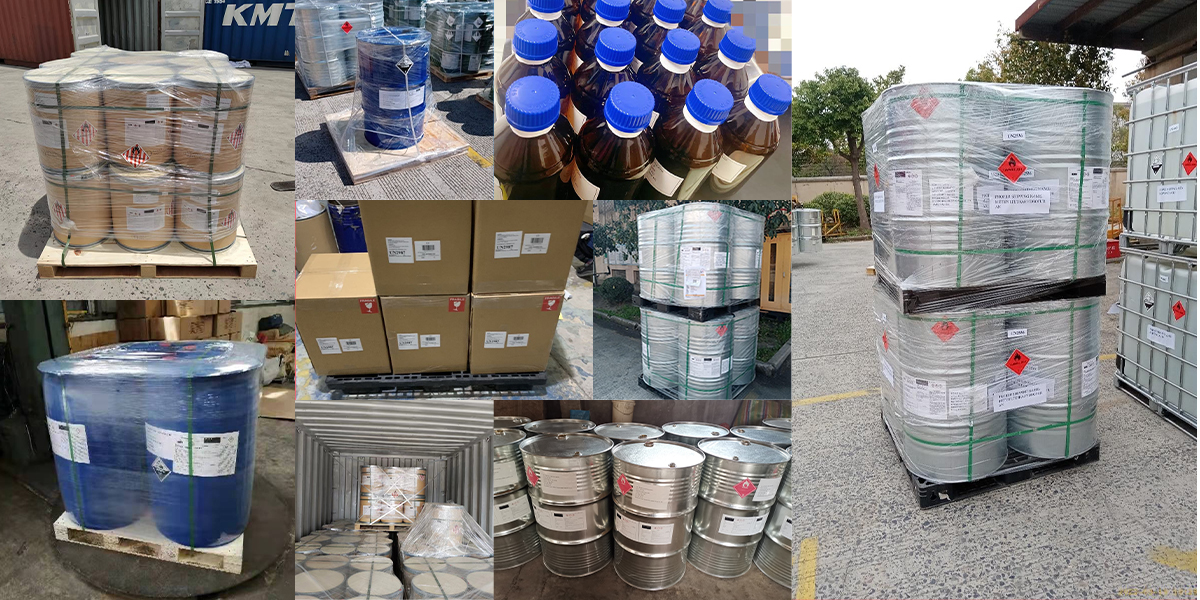
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.