Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
Methyl Octanoate (CAS 111-11-5), a versatile fatty acid methyl ester, is far more than just a pleasant aroma compound. Its chemical structure and reactivity make it an indispensable intermediate in a wide array of organic synthesis applications. For research scientists and product formulators, understanding its utility can unlock new product development avenues. This article delves into the significant role Methyl Octanoate plays in modern chemical manufacturing and highlights how to procure it effectively from trusted suppliers.
Methyl Octanoate as a Synthetic Building Block
At its core, Methyl Octanoate is a source of the octanoyl group, a C8 fatty acid derivative. This makes it an excellent starting material for synthesizing various compounds. One of its primary uses is in the production of detergents and emulsifiers, where its amphiphilic nature is leveraged. The ester linkage can be readily manipulated through reactions like transesterification or hydrolysis to introduce new functional groups or modify existing molecules.
Furthermore, Methyl Octanoate serves as a precursor for other chemicals used in lubricants, plasticizers, and resins. Its role extends to laboratory research, where it participates in complex multi-step syntheses, contributing its ester functionality or alkyl chain. The ability to buy Methyl Octanoate in high purity, as offered by specialized manufacturers, is crucial for achieving high yields and avoiding unwanted side reactions in these sensitive synthetic pathways.
Advantages of Sourcing from a Dedicated Manufacturer
When undertaking organic synthesis, the quality of starting materials directly impacts the success of the reaction. Sourcing Methyl Octanoate from a dedicated chemical manufacturer in China, such as NINGBO INNO PHARMCHEM CO.,LTD., offers several advantages. These include guaranteed purity levels (≥99%), consistent quality lot-to-lot, and a stable supply chain. For those looking to buy this intermediate, understanding its specifications – such as its boiling point of 194-195°C and its insolubility in water – helps in designing appropriate reaction and work-up procedures. By partnering with a reliable supplier, chemists can focus on innovation rather than worrying about the quality of their raw materials.
Driving Innovation with Methyl Octanoate
The continued demand for novel materials and functional chemicals ensures that intermediates like Methyl Octanoate remain vital. Its application in creating custom esters or as a fragment in more complex molecular architectures underscores its importance. For researchers and industrial chemists alike, access to a dependable source of high-quality Methyl Octanoate is key to driving innovation in fields ranging from materials science to pharmaceuticals. If your synthesis projects require this crucial component, consider purchasing directly from experienced manufacturers to ensure your research and production efforts are built on a foundation of quality and reliability.
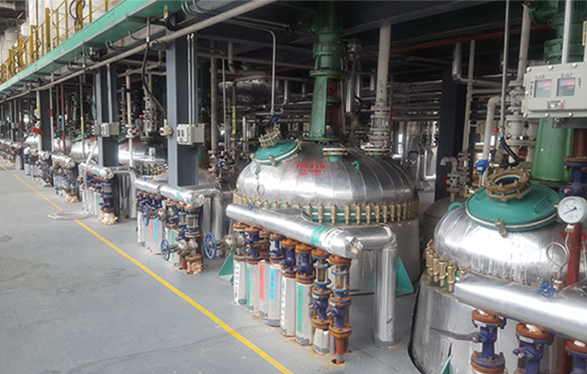
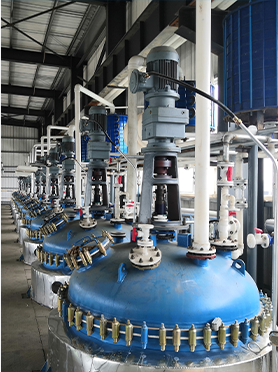
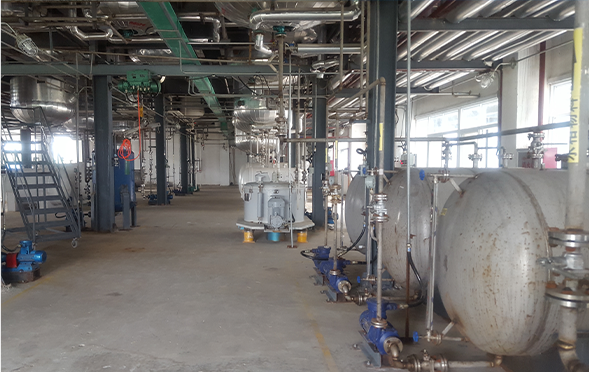
Manufacturing Facilities
Professional Export Experience
to Global Customers
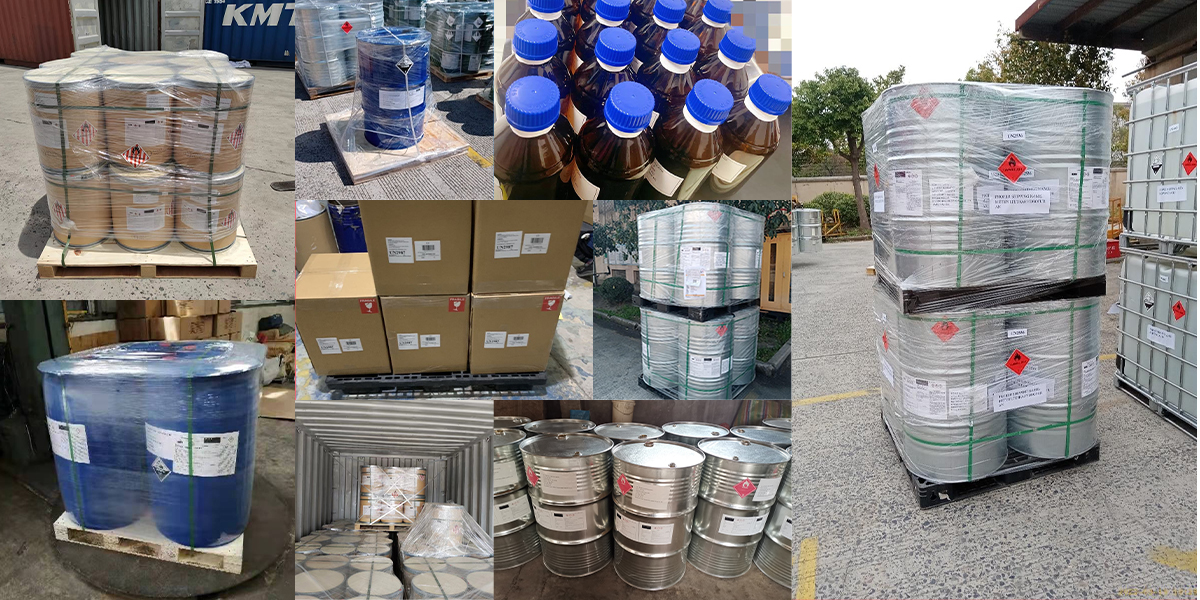
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.