Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
The pharmaceutical industry demands the highest standards of purity, consistency, and reliability for its raw materials. Monoethanolamine (MEA), a foundational chemical with diverse industrial applications, also plays a crucial role in various pharmaceutical processes. From acting as a pH buffer in formulations to serving as an intermediate in the synthesis of active pharmaceutical ingredients (APIs), MEA’s utility is significant. For pharmaceutical manufacturers and procurement specialists, understanding MEA’s role and sourcing it from a dependable supplier is paramount.
MEA's Critical Functions in Pharmaceutical Applications
Monoethanolamine (CAS 141-43-5) is valued in pharmaceutical manufacturing for its chemical properties, particularly its alkalinity and reactivity. Its primary functions include:
The stringent requirements of the pharmaceutical sector mean that the purity and quality of MEA used are of utmost importance. Trace impurities can have significant downstream effects on drug product safety and efficacy. Therefore, sourcing MEA from a manufacturer that adheres to pharmaceutical-grade standards or offers high-purity industrial grades (like our 99.5% MEA) is a crucial consideration.
Sourcing High-Purity MEA: The Advantage of a Global Manufacturer
For pharmaceutical companies needing to buy MEA, partnering with a reputable global manufacturer offers significant advantages:
When sourcing critical raw materials like Monoethanolamine for pharmaceutical use, reliability and quality are non-negotiable. We are committed to being a trusted supplier for the pharmaceutical industry, providing the high-purity MEA necessary to develop safe and effective medications. We invite you to contact us to discuss your specific requirements for MEA 99.5% and discover how our commitment to quality and service can benefit your manufacturing processes.
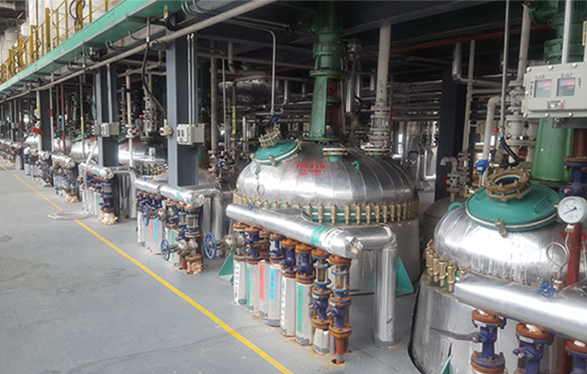
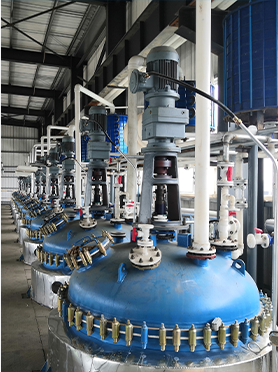
Manufacturing Facilities
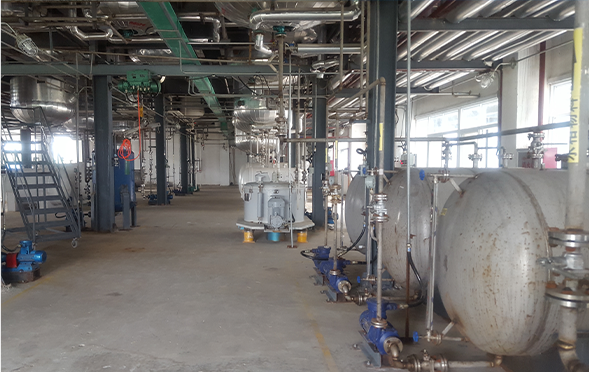
Professional Export Experience
to Global Customers
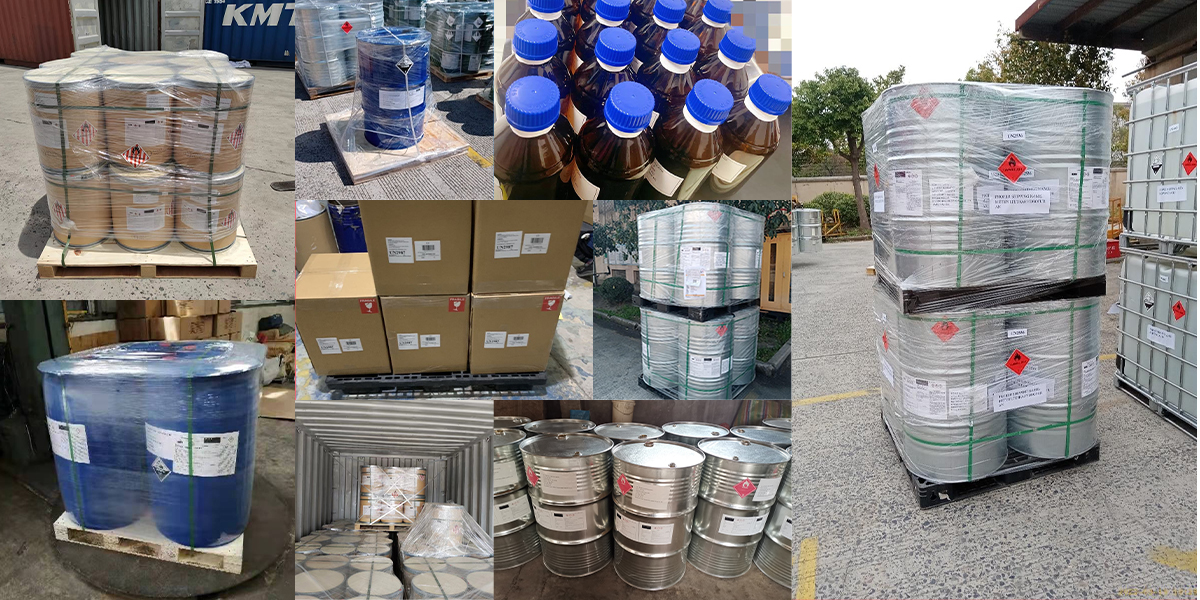
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.