Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
In the constant effort to mitigate environmental impact, industries are continuously seeking more efficient methods for removing Volatile Organic Compounds (VOCs) from their emissions. NINGBO INNO PHARMCHEM CO.,LTD. highlights the significant role of honeycomb zeolite technology as a superior solution for industrial VOC removal. This advanced material combines the exceptional adsorption properties of zeolites with a structured honeycomb matrix to deliver unparalleled performance.
The Synergy of Zeolite and Honeycomb Structure
Zeolites, often referred to as molecular sieves, are renowned for their precisely engineered porous structures that allow for selective adsorption of molecules. When formed into a honeycomb matrix, these materials offer several key advantages for VOC abatement:
1. Enhanced Surface Area: The honeycomb structure dramatically increases the surface area accessible to VOCs. This geometric design maximizes the contact between the pollutant molecules and the zeolite adsorbent, leading to more efficient capture.
2. Low Pressure Drop: The open channels of the honeycomb matrix facilitate excellent gas flow dynamics, resulting in a low pressure drop. This is crucial for energy efficiency in large-scale industrial systems, as it requires less energy to move air through the adsorbent bed.
3. Improved Adsorption Efficiency: The combination of zeolite's selective adsorption capabilities and the honeycomb structure's large surface area leads to higher overall VOC removal efficiency. This is a critical aspect of industrial VOC abatement solutions.
Why Choose Honeycomb Zeolite? Advantages for Industry
NINGBO INNO PHARMCHEM CO.,LTD. advocates for honeycomb zeolite technology due to its distinct benefits:
1. Superior Adsorption Capacity for VOCs: Zeolites are highly effective at adsorbing a wide range of VOCs, including those that are challenging for other adsorbents. Their strong affinity for organic molecules ensures high capture rates, crucial for meeting emission standards.
2. High-Temperature Regeneration Capability: Unlike many conventional adsorbents, zeolites can be regenerated at elevated temperatures. This allows for the effective release of adsorbed VOCs and reuse of the adsorbent material, making it a sustainable and cost-effective option for long-term operation.
3. Robust Thermal and Chemical Stability: Honeycomb zeolites are engineered to withstand demanding industrial conditions, including high temperatures and the presence of various chemicals. This durability ensures consistent performance over extended periods, a key factor in honeycomb ceramic applications in emissions control.
4. Customization for Specific Applications: NINGBO INNO PHARMCHEM CO.,LTD. can offer customized honeycomb zeolite solutions tailored to specific industrial needs, considering the types of VOCs, flow rates, and operating conditions. This flexibility ensures optimal performance for each unique application.
Applications and Environmental Impact
Honeycomb zeolite technology is widely implemented in industries such as automotive manufacturing, printing, chemical processing, and pharmaceutical production. It is used in regenerative thermal oxidizers (RTOs) and catalytic oxidizers to concentrate VOCs before destruction, or as a direct adsorption medium. The ability to efficiently remove VOCs contributes significantly to improving air quality and ensuring regulatory compliance. This aligns perfectly with the goals of sustainable waste gas treatment.
At NINGBO INNO PHARMCHEM CO.,LTD., we are committed to providing innovative and effective solutions for environmental challenges. Our honeycomb zeolite products represent a leap forward in VOC removal technology, offering industries a powerful tool to achieve cleaner emissions and a healthier planet.
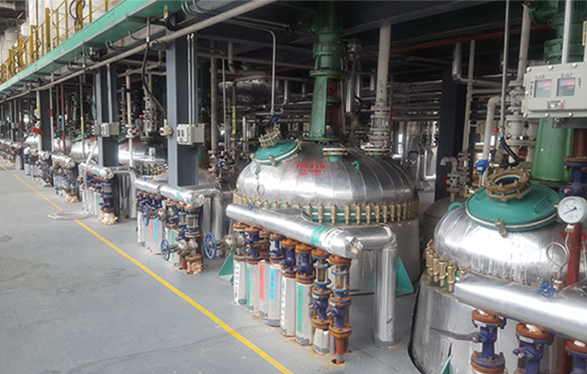
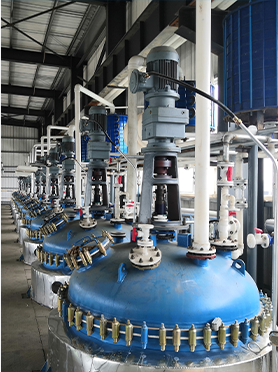
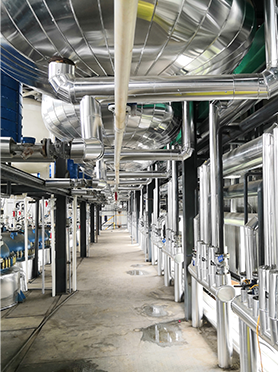
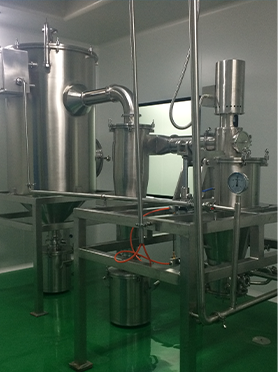
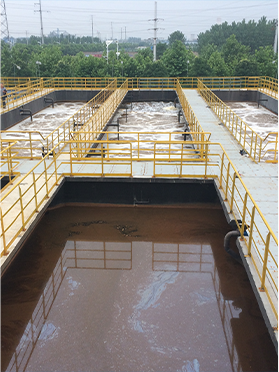
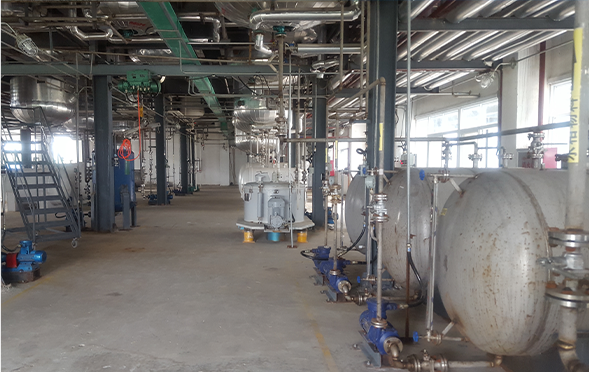
Manufacturing Facilities
Professional Export Experience
to Global Customers
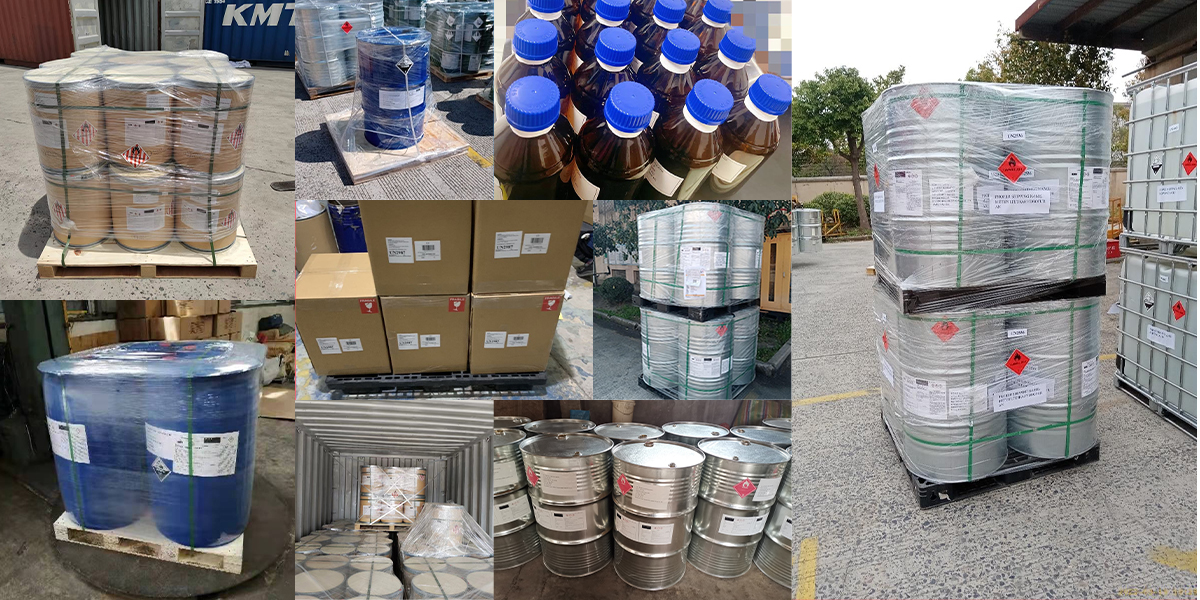
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.