Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
The medical device industry operates under stringent requirements for material safety, performance, and reliability. Among the advanced materials that meet these demanding criteria, silicone copolymers, specifically Vinylmethylsiloxane-Dimethylsiloxane Copolymers, play a pivotal role. These sophisticated polymers are integral to the design and functionality of a vast range of medical products, from simple tubing to complex implantable devices.
The Biocompatibility and Performance of Silicone Copolymers
Vinylmethylsiloxane-Dimethylsiloxane Copolymers, trimethylsiloxy terminated (CAS 67762-94-1), are highly valued in the medical field due to their exceptional biocompatibility. They exhibit low toxicity, minimal reactivity with biological tissues, and resistance to degradation in physiological environments. This makes them an ideal choice for applications that involve direct or indirect contact with the human body. Beyond biocompatibility, these copolymers offer excellent flexibility, which is crucial for devices like catheters and medical tubing, allowing for ease of insertion and patient comfort.
Furthermore, their chemical structure provides inherent resistance to a variety of sterilization methods, including autoclaving and gamma irradiation, which is essential for ensuring the sterility of medical equipment. The ability to form durable, yet flexible, elastomers through their vinyl functionality means that medical device manufacturers can produce components that withstand repeated use and sterilization cycles without compromising performance.
Key Applications in the Medical Field
The versatility of these silicone copolymers translates into numerous critical applications:
Research scientists and product development teams constantly explore new ways to leverage the unique properties of these copolymers to create more effective and patient-friendly medical solutions.
Reliable Sourcing from Expert Manufacturers
For medical device manufacturers, securing a consistent and high-quality supply of critical raw materials like these silicone copolymers is non-negotiable. When seeking a manufacturer or supplier, it is imperative to partner with organizations that understand and adhere to the rigorous quality standards of the medical industry. Sourcing from experienced companies, particularly those with a strong presence in specialty chemical markets such as China, can provide access to competitively priced, high-purity materials. Ensuring that your supplier can provide comprehensive documentation, including certificates of analysis and regulatory compliance information, is vital.
The ability to buy these materials with confidence from a reputable source ensures that your medical devices meet all necessary safety and performance benchmarks. A close working relationship with your chemical supplier can also facilitate the sourcing of specific grades tailored to your unique manufacturing processes and product requirements.
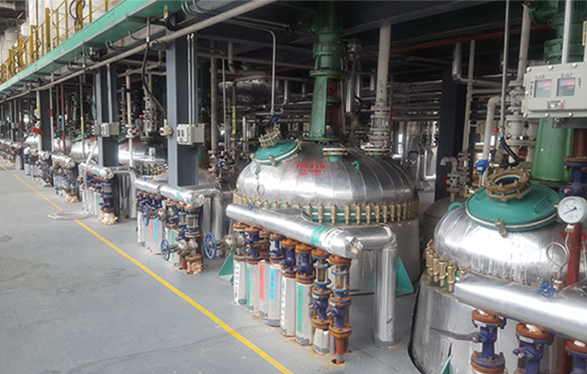
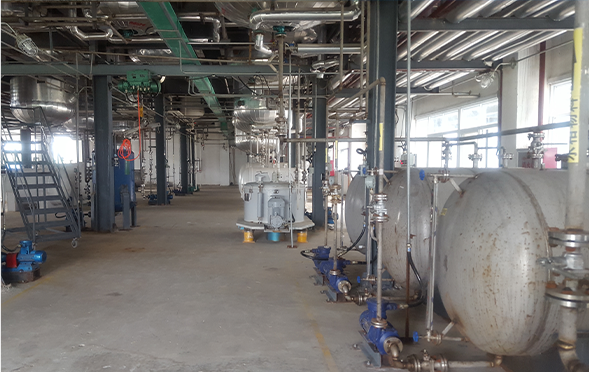
Manufacturing Facilities
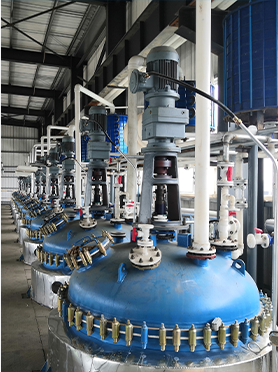
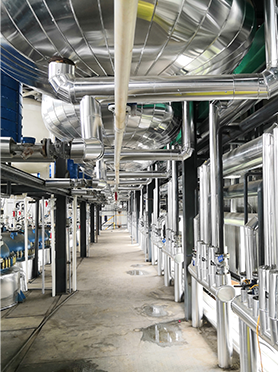
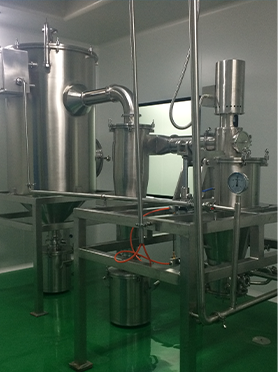
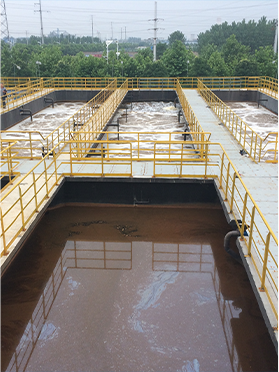
Professional Export Experience
to Global Customers
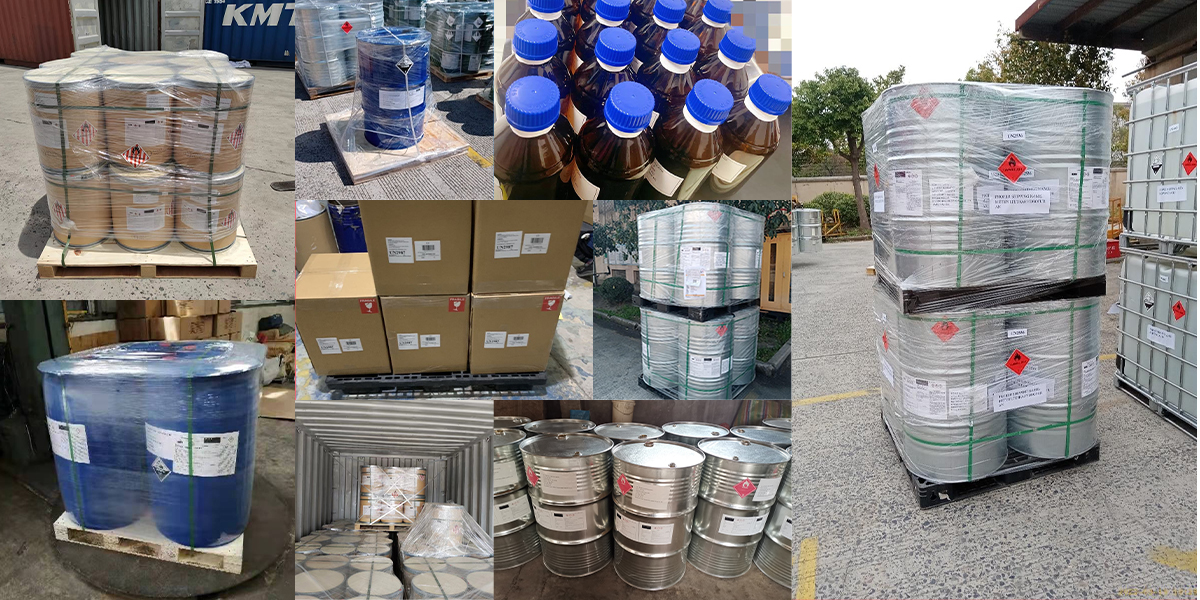
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.