Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
In the complex world of mineral processing, optimizing recovery rates and ensuring concentrate quality are paramount. For professionals in the mining industry, understanding the specific roles of key chemical reagents can lead to significant improvements in efficiency and cost-effectiveness. Among these essential chemicals is Sodium Metabisulfite, commonly abbreviated as SMBS.
Sodium Metabisulfite is primarily recognized for its function as a beneficiation agent and inhibitor in various mining operations. Its effectiveness stems from its strong reducing properties, which allow it to interact with mineral surfaces in specific ways to enhance the separation of valuable ores from gangue.
The primary application of SMBS in mining revolves around its ability to influence the flotation process. It acts as a selective depressant for certain sulfide minerals, most notably pyrite and sphalerite. This is achieved through several mechanisms:
The effective use of Sodium Metabisulfite requires careful consideration of its application method and dosage. As a chemical that can be easily oxidized, SMBS solutions are typically prepared on the day of use to ensure maximum efficacy.
Preparation of Solution: SMBS is dissolved in water to create a solution of a specified concentration. This solution is then added to the ore pulp.
Segmented Addition: To maintain a stable inhibitory effect throughout the flotation process, a segmented addition strategy is often employed. This involves adding the SMBS solution in multiple stages rather than all at once.
Dosage: The exact dosage of Sodium Metabisulfite is not fixed and depends heavily on several factors, including the specific ore characteristics, the processing technology employed, pulp concentration, and pH levels. Practical experience and laboratory tests are crucial for determining the optimal dosage for a given operation. Typical dosages can range from a few grams to tens of grams per ton of ore. For instance, in detoxification tests for cyanide leaching tailings, dosages around 4.0g/L have been used, while in processes to improve leaching rates of refractory gold ores, dosages might be around 3kg/t. It is essential for mining professionals to consult with expert suppliers or conduct pilot tests to find the precise SMBS dosage that maximizes their beneficiation results.
For any mining operation looking to procure Sodium Metabisulfite, partnering with a reputable manufacturer or supplier is key. When you choose to buy SMBS, consider factors such as product purity, consistency, packaging, and the availability of technical support. As a leading provider from China, we are committed to delivering high-quality Sodium Metabisulfite that meets stringent industrial standards. We invite you to request a quote to explore how our SMBS can optimize your mineral processing operations.
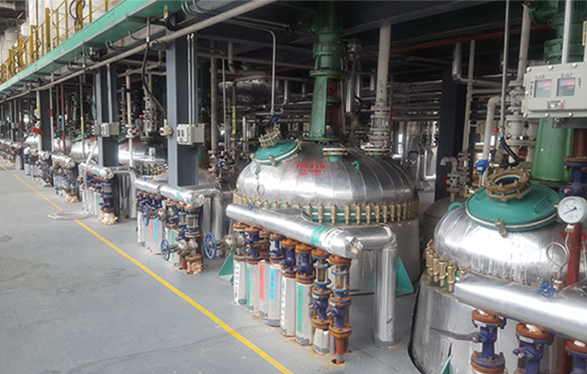
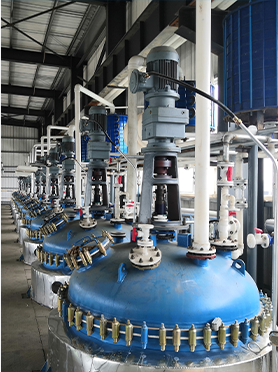
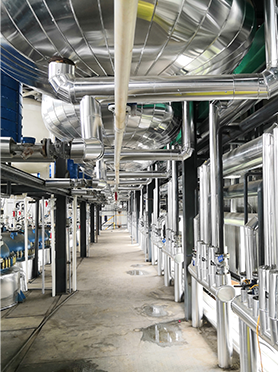
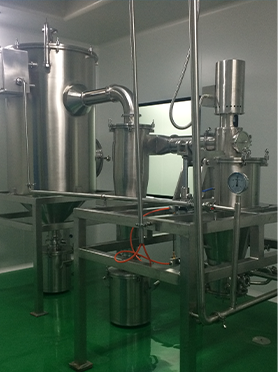
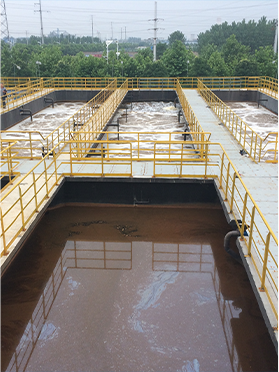
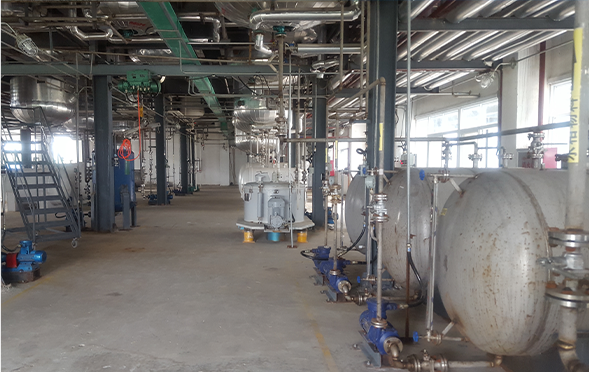
Manufacturing Facilities
Professional Export Experience
to Global Customers
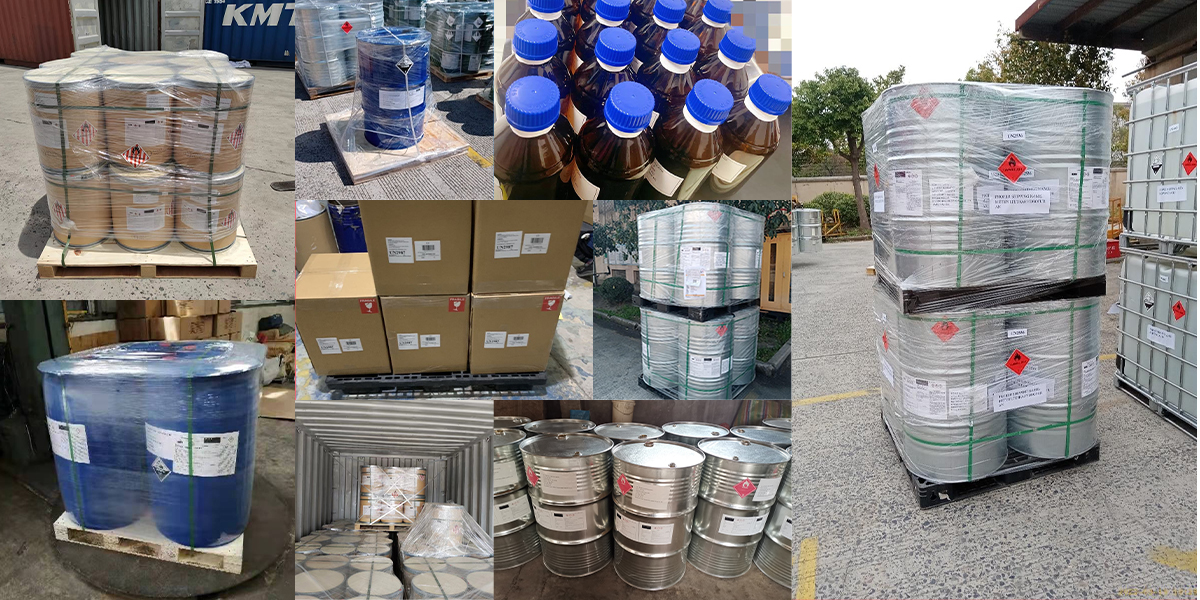
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.