Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
Protecting industrial piping systems from the ravages of scale and corrosion is fundamental to operational integrity and cost management. Many industries rely on chemical treatments to maintain the health of their fluid transport networks. For businesses seeking to purchase top-tier chemical auxiliaries, understanding the advantages of advanced formulations like organophosphonate copolymer systems is key. NINGBO INNO PHARMCHEM, as a leading manufacturer and supplier, details why these chemicals are essential for optimal piping protection.
The Silent Threat: Scale and Corrosion in Pipelines
Pipelines in industrial settings, whether for cooling water, process fluids, or raw materials, are constantly exposed to conditions that promote scale formation and corrosion. Calcium-based scales, mineral deposits, and aggressive chemical environments can all compromise the integrity of pipes. This leads to:
To combat these issues effectively, companies need to buy specialized water treatment chemicals that offer comprehensive protection.
Organophosphonate Copolymer Systems: A Superior Choice for Piping Protection
Organophosphonate copolymer systems offer a multi-faceted approach to safeguarding industrial piping. Their unique chemical structure allows them to perform multiple functions simultaneously:
As a reliable manufacturer and supplier from China, NINGBO INNO PHARMCHEM provides these advanced solutions to industries worldwide. Our commitment is to deliver products that not only protect but also enhance the operational efficiency of your piping systems.
Procuring Quality Water Treatment Chemicals from NINGBO INNO PHARMCHEM
When you choose NINGBO INNO PHARMCHEM, you are partnering with a company dedicated to excellence in chemical manufacturing. We offer organophosphonate copolymer systems that are rigorously tested to ensure they meet the highest performance standards. By opting to buy from us, you gain:
Invest in the long-term health of your industrial infrastructure. If you are looking to buy effective piping protection solutions, contact NINGBO INNO PHARMCHEM. Discover how our organophosphonate copolymer systems can provide the comprehensive protection your systems require.
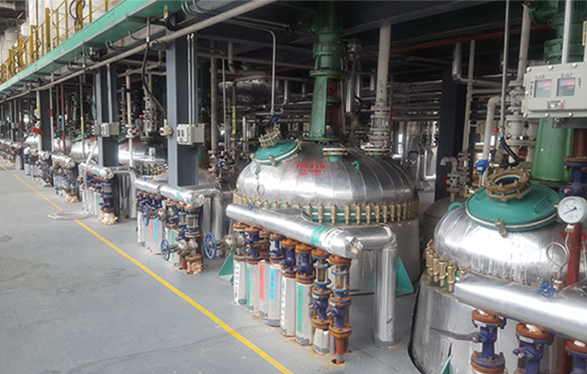
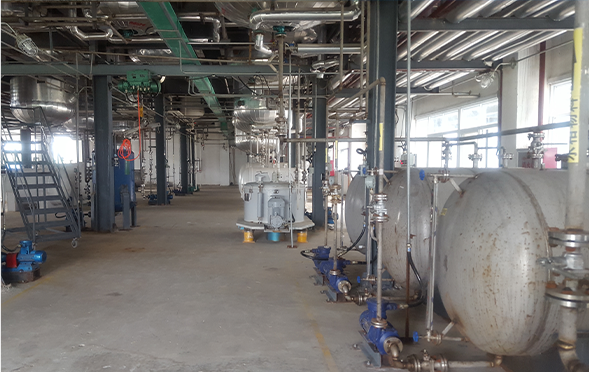
Manufacturing Facilities
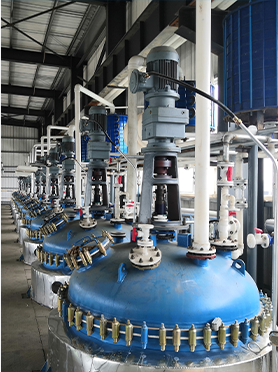
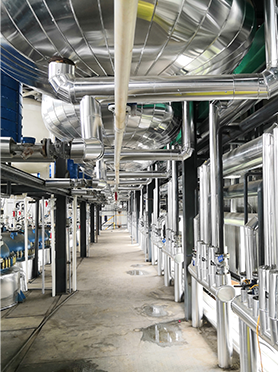
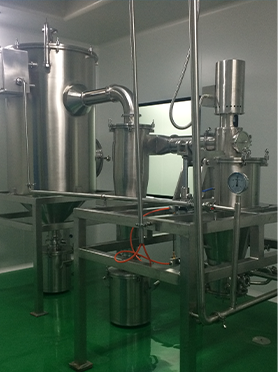
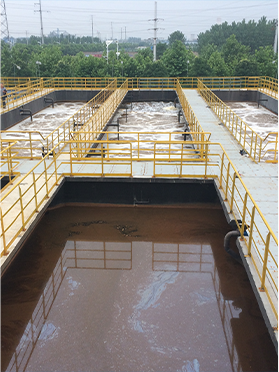
Professional Export Experience
to Global Customers
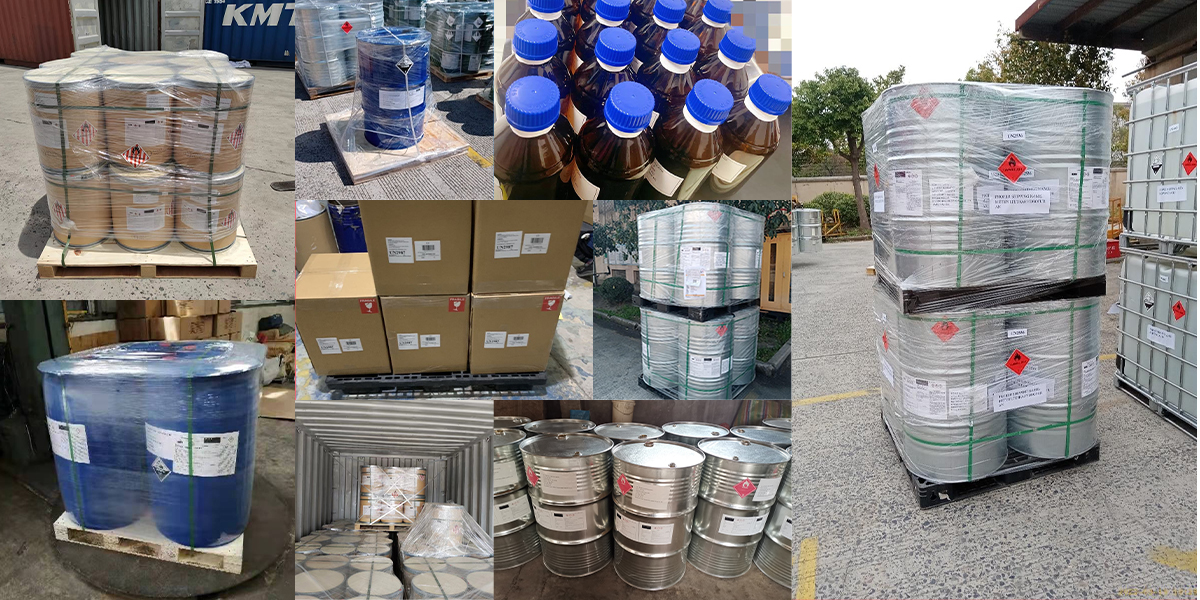
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.