20 YEARS OF PROFESSIONAL & DEDICATED SERVICE TO GLOBAL CUSTOMERS

Custom Manufacturing, Project Outsourcing, your Trusted Partner from China

Procurement Guide: Sourcing High-Quality Boiler Water Treatment Chemicals

The efficient and safe operation of industrial boilers is heavily reliant on effective water treatment programs. Procurement managers and technical leads are constantly seeking high-quality chemicals that can prevent scale, control corrosion, and ensure optimal performance throughout the boiler's lifecycle. From daily operational treatments to critical shutdown protection, the right chemical solutions are indispensable. As a leading manufacturer and supplier in China, we aim to provide clarity on sourcing these vital industrial chemicals.

Understanding Key Boiler Water Treatment Chemicals
Effective boiler water treatment typically involves a combination of chemicals designed to address specific issues. Among the most crucial categories are:

  • Corrosion Inhibitors: These chemicals are designed to protect metal surfaces from corrosion, which can be exacerbated by dissolved oxygen, high temperatures, and aggressive ions. Octadecylamine, a long-chain fatty amine, is a prime example, forming a protective film on metal surfaces. Its efficacy in boiler systems and during shutdown periods makes it a popular choice. If you are looking to buy corrosion inhibitors, understanding their application and sourcing them from a reputable manufacturer is key.
  • Scale Inhibitors: Scale, such as calcium carbonate or magnesium silicate, can form on boiler surfaces, reducing heat transfer efficiency and potentially causing overheating. Scale inhibitors prevent the formation and adherence of these deposits.
  • Oxygen Scavengers: While proper deaeration is crucial, oxygen scavengers are often used as a secondary measure to remove any residual dissolved oxygen that could otherwise contribute to corrosion.
  • Shutdown Protection Agents: Specifically formulated for periods when boilers are inactive, these agents provide long-term anti-rust protection, reduce scaling, and can even clean components like turbine blades. Their ability to protect equipment for over two years makes them a strategic purchase for extending asset life.

The Importance of Sourcing from a Reliable Manufacturer
When procuring industrial chemicals, the quality and consistency of the product are paramount. As a manufacturer based in China, we understand the importance of:

  • Purity and Formulation: The efficacy of a chemical depends heavily on its purity and precise formulation. Our advanced manufacturing processes ensure that our products, including Octadecylamine and specialized protection agents, meet high standards.
  • Technical Support: A good supplier not only provides chemicals but also offers technical expertise to help clients select the right products and apply them correctly for maximum benefit.
  • Competitive Pricing: By sourcing directly from a manufacturer, you can often achieve more competitive pricing, especially for bulk orders, making essential treatments more economically viable.
  • Supply Chain Reliability: A stable supply chain is critical for industrial operations. We ensure consistent availability and timely delivery of our products.

Making the Right Procurement Decisions
For procurement managers and chemists, selecting the right boiler water treatment chemicals involves balancing effectiveness, cost, and ease of application. Whether you need Octadecylamine for ongoing corrosion control or a specialized shutdown protection agent for planned maintenance, understanding the product's function and benefits is essential. We encourage you to consider our range of high-quality industrial chemicals. If you are looking to buy these vital products or require a quote for your facility, please contact our sales team. Partnering with a trustworthy manufacturer ensures you are investing in the long-term health and efficiency of your boiler systems.

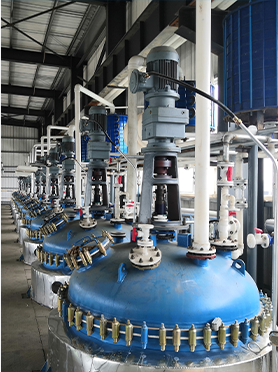
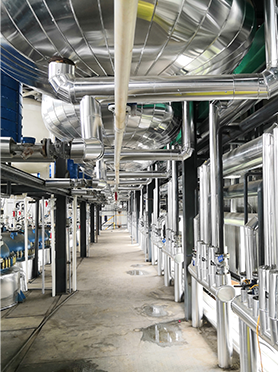
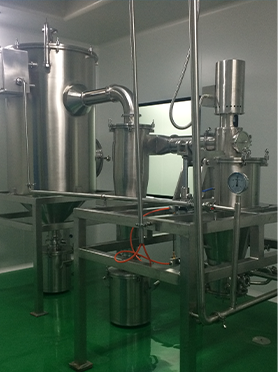
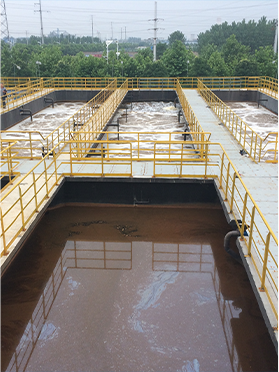
Manufacturing Facilities
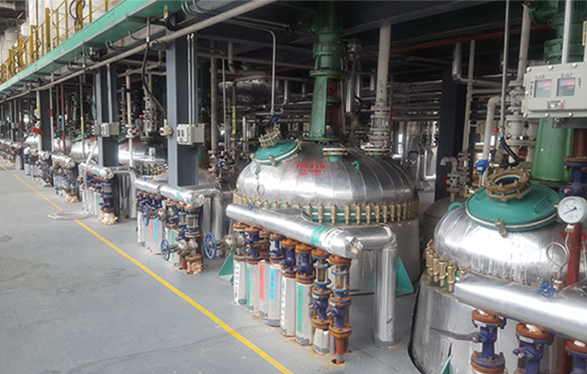
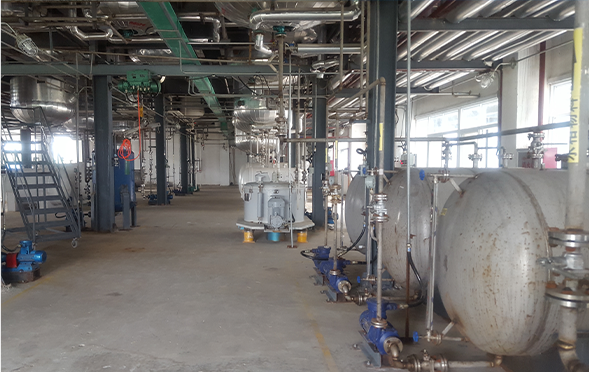
NINGBO INNO PHARMCHEM CO.,LTD. was established in 2007. It is committed to the R&D, production and sales of raw materials, pharmaceutical intermediates and fine chemicals. We striving to create a high-efficiency and high-quality integrated chemical service platform to better serve domestic and foreign customers.

Professional Export Experience

to Global Customers
WHY CHOSE US?

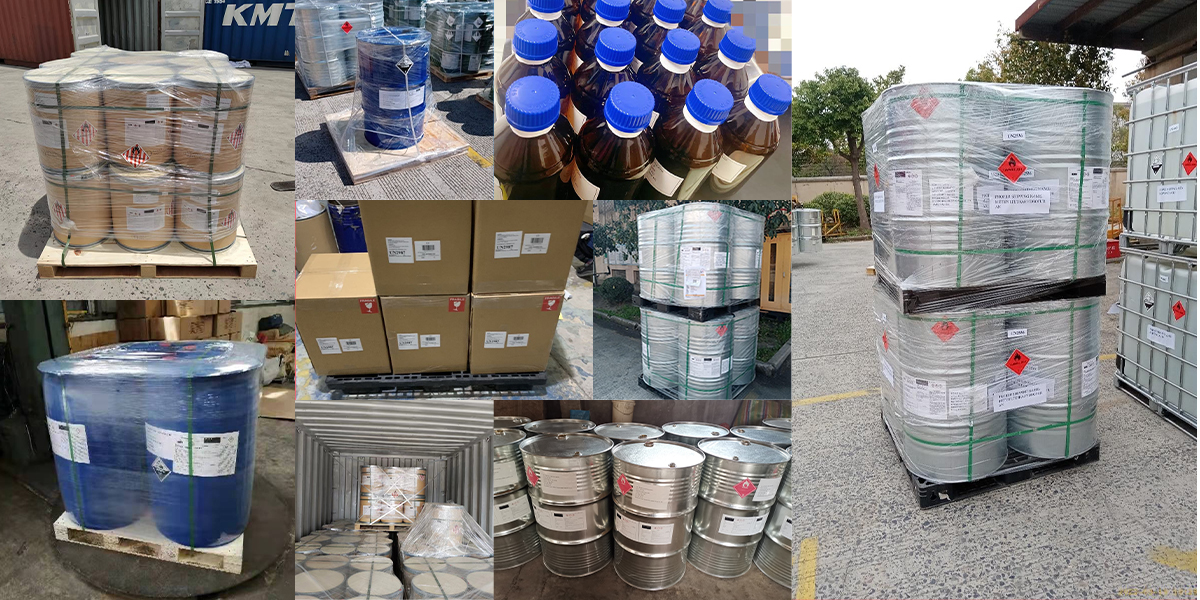
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;

2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;

3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).

FAQ

  • A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.

  • A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.

  • A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.
CONTACT US
Should you need to contact us; you may call during regular business hours, Monday through Friday, 8am – 6 pm.
NINGBO INNO PHARMCHEM CO.,LTD.
Address: No.163 Ruiqing Rd.,Ningbo 315000 China
Phone: 86-574-87319282
Fax: 86-574-27912196
SEND US AN EMAIL

NAME*

EMAIL*

COMPANY

COUNTRY*

MESSAGE*

Previous: Extending Boiler Life: The Power of Shutdown Protection Agents

Next: Protecting Industrial Assets: The Role of Film-Forming Amines

All Rights Reserved