Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
Activated alumina plays a crucial role in modern industry, serving as a highly effective desiccant for industrial drying and a key agent in water purification processes. NINGBO INNO PHARMCHEM CO.,LTD. specializes in providing a premium quality activated alumina adsorbent that meets stringent industry demands. Understanding the activated alumina desiccant properties is fundamental to appreciating its broad applicability.
In the field of industrial drying, activated alumina is unparalleled. Its high moisture absorption capacity and ability to be regenerated make it a sustainable and efficient choice for drying compressed air, natural gas, and various industrial feedstocks. The consistent performance and reliability of a high quality activated alumina adsorbent ensure that processes operate smoothly and efficiently, preventing moisture-related issues that can lead to equipment damage or product spoilage.
The application of activated alumina for water purification is equally significant, particularly in the removal of fluoride. Fluoride, while beneficial in small amounts, can be detrimental to health when present in excess. Activated alumina demonstrates a remarkable high defluorination volume, effectively binding and removing fluoride ions from drinking water sources. This makes it an indispensable component in municipal water treatment plants and household water purification systems. The efficacy of activated alumina in this context is a testament to its specific surface area and pore structure.
When businesses consider where to buy activated alumina, they look for consistent quality and reliable supply. NINGBO INNO PHARMCHEM CO.,LTD. ensures that their activated alumina desiccant meets rigorous standards, offering various particle sizes to suit different application requirements. The price of activated alumina is often considered in relation to its performance and lifespan, and its regenerative capabilities contribute to its cost-effectiveness over time.
Beyond drying and defluorination, activated alumina also serves as a catalyst support in various chemical reactions, further highlighting its versatility. Its stable structure and inert nature make it an ideal matrix for active catalytic components. This broad range of applications underscores the importance of this material in multiple industrial sectors.
In conclusion, activated alumina is a cornerstone material for both industrial drying and ensuring safe drinking water through effective purification. NINGBO INNO PHARMCHEM CO.,LTD. is proud to offer a superior grade of activated alumina that delivers exceptional performance. We encourage industries to explore the benefits of this versatile adsorbent for their critical processes.
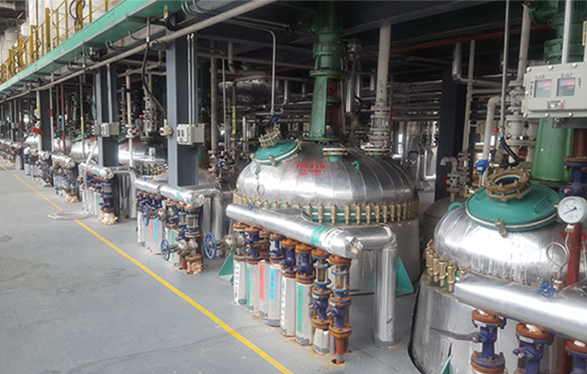
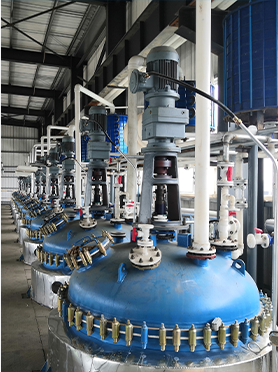
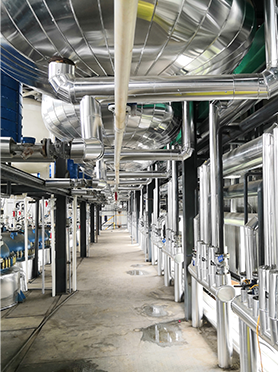
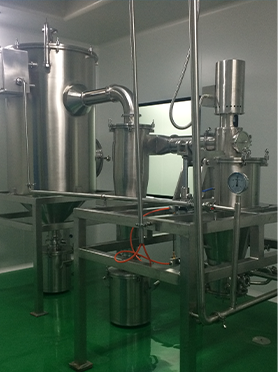
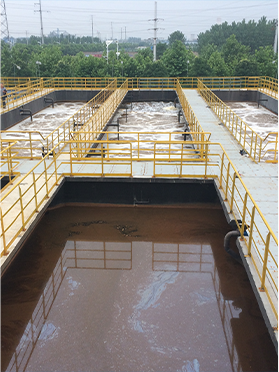
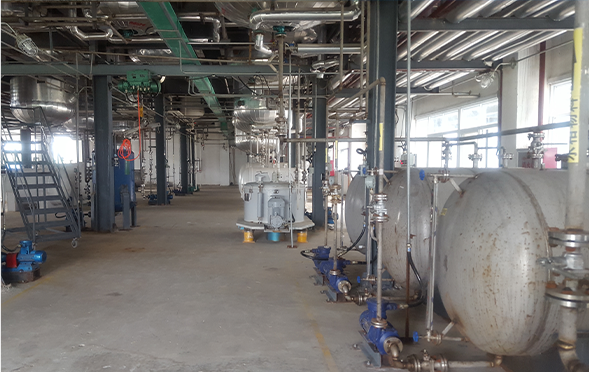
Manufacturing Facilities
Professional Export Experience
to Global Customers
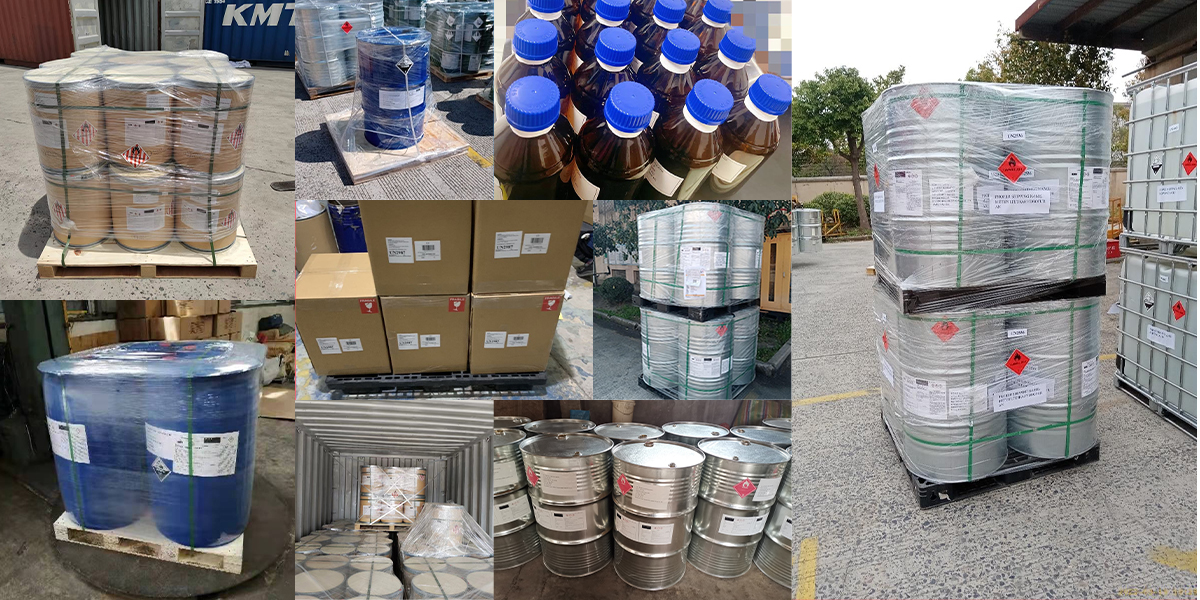
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.