Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
In the competitive landscape of pharmaceutical manufacturing, the quality and reliability of intermediates are paramount. For companies involved in the production of advanced therapies like Olaparib, securing a consistent supply of high-purity intermediates is not just a logistical necessity but a critical factor in ensuring drug efficacy and patient safety. This article explores the significance of sourcing key pharmaceutical intermediates, focusing on 4-[4-Fluoro-3-(piperazine-1-carbonyl)benzyl]phthalazin-1(2H)-one (CAS: 763111-47-3), a crucial building block in Olaparib synthesis.
Olaparib, a groundbreaking PARP inhibitor, has revolutionized cancer treatment, particularly for ovarian, breast, and prostate cancers linked to BRCA mutations. The synthesis of such a complex molecule relies heavily on the precise quality of its constituent intermediates. 4-[4-Fluoro-3-(piperazine-1-carbonyl)benzyl]phthalazin-1(2H)-one, often supplied as a yellow to white solid with a purity of ≥98%, serves as an indispensable component in its production pathway. Manufacturers worldwide seek dependable suppliers who can guarantee both the quality and the scale required for commercial production.
When looking to buy this essential pharmaceutical intermediate, understanding the specifications is key. Purity levels, consistent physical properties, and adherence to stringent manufacturing standards are non-negotiable. As a leading manufacturer and supplier of pharmaceutical intermediates in China, we specialize in delivering compounds that meet these exacting requirements. Our robust production processes ensure that every batch of 4-[4-Fluoro-3-(piperazine-1-carbonyl)benzyl]phthalazin-1(2H)-one adheres to the highest industry benchmarks.
For R&D scientists and procurement managers, identifying a trustworthy Olaparib intermediate manufacturer is crucial. Factors such as production capacity, quality control measures, and competitive price points are vital considerations. We invite you to explore our offerings and discover why partnering with us provides a distinct advantage. Our commitment to excellence ensures that your supply chain remains robust, allowing you to focus on developing and delivering life-saving medications. Whether you are planning large-scale production or require materials for early-stage research, we are equipped to meet your needs. Consider us your strategic partner for all your pharmaceutical intermediate sourcing requirements.
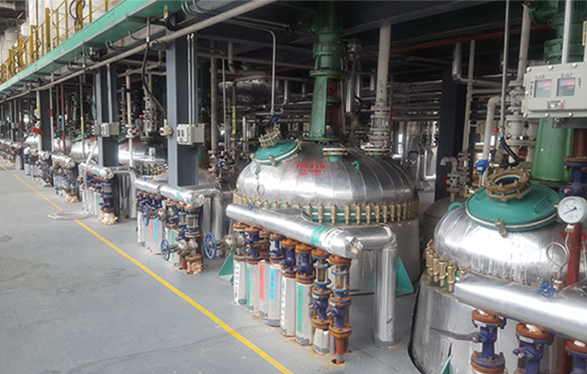
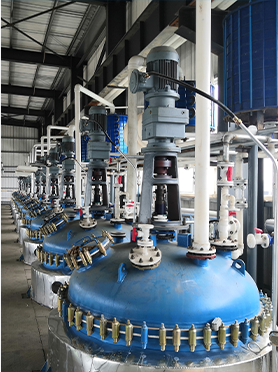
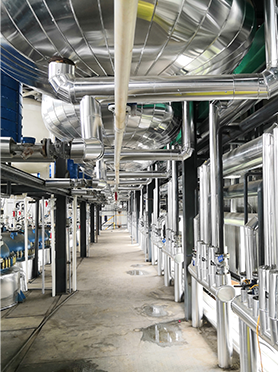
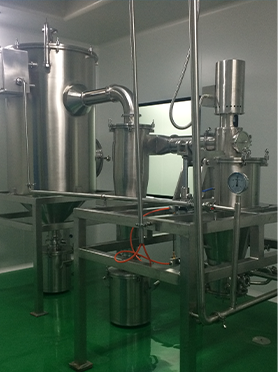
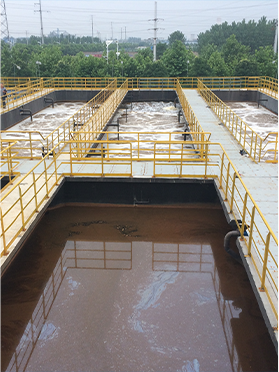
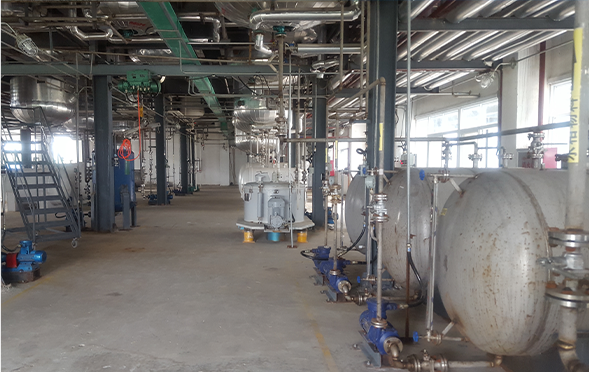
Manufacturing Facilities
Professional Export Experience
to Global Customers
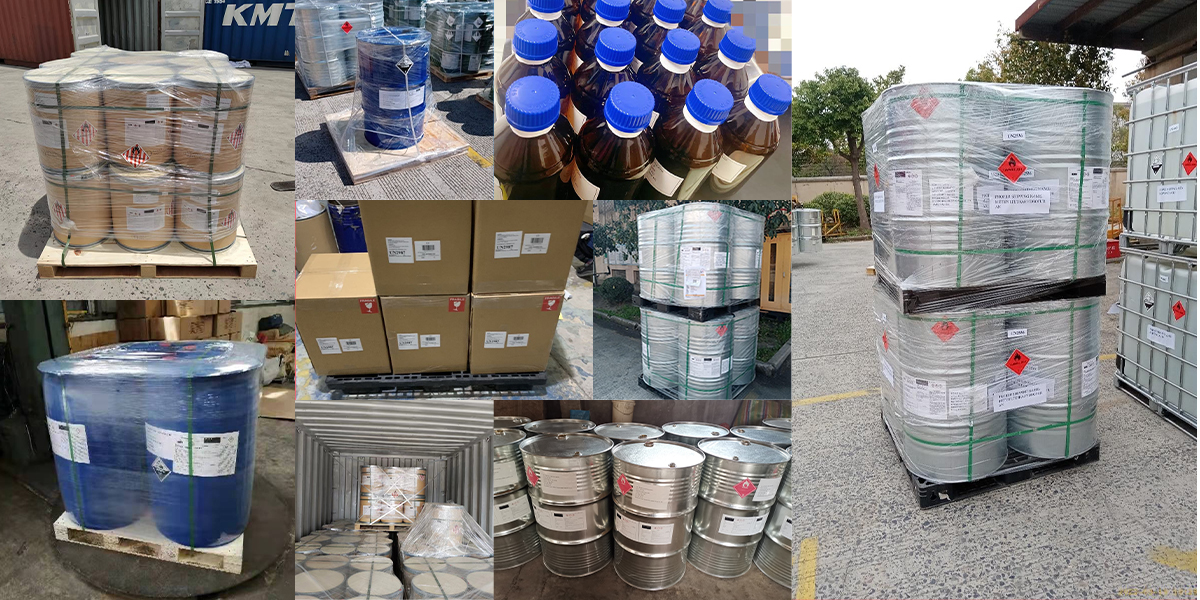
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.