Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
In the fast-paced world of pharmaceutical research and development, the reliability of the supply chain for critical raw materials and intermediates is non-negotiable. For compounds like (R)-3-Amino-3-(4-cyanophenyl)propionic acid, which serve as essential building blocks for novel therapeutics, disruptions in supply can have cascading negative effects on project timelines and budgetary goals.
As a manufacturer and supplier of advanced chemical intermediates, we understand the imperative of maintaining a consistent and dependable supply. Our operations are geared towards ensuring that when our clients need to buy (R)-3-Amino-3-(4-cyanophenyl)propionic acid, it is readily available in the required quantities and purity levels. This involves meticulous inventory management, efficient production planning, and robust logistics.
The pharmaceutical industry operates under strict regulatory and quality control standards. Therefore, the intermediates used must not only be available but also meet exacting specifications. For (R)-3-Amino-3-(4-cyanophenyl)propionic acid, this means a guaranteed high purity (e.g., 97%) and precise stereochemical integrity. Partnering with a supplier that prioritizes these aspects from manufacturing through to delivery is paramount. A trustworthy supplier acts as an extension of your R&D team, ensuring that your foundational materials are always up to standard.
When evaluating potential suppliers, consider their track record for on-time delivery, their quality control processes, and their capacity to scale production if your project progresses to larger quantities. Factors like competitive pricing are important, but they should never overshadow the critical need for supply chain stability and product consistency. Investing in a strong relationship with a reliable manufacturer can mitigate risks associated with unexpected shortages or quality deviations.
Ultimately, the success of developing new pharmaceuticals hinges on the seamless integration of various components, starting with the highest quality intermediates. By focusing on reliable supply chains and partnering with experienced manufacturers, research institutions and pharmaceutical companies can accelerate their innovation cycles and bring life-changing treatments to market more effectively.
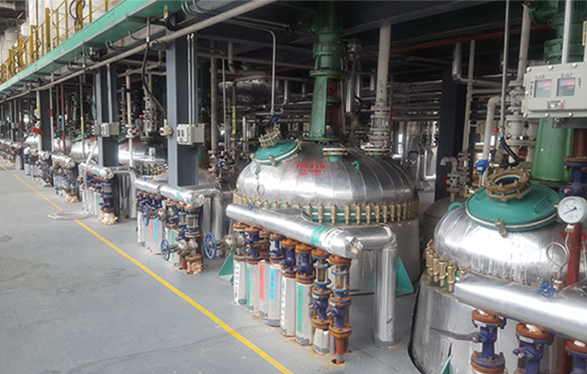
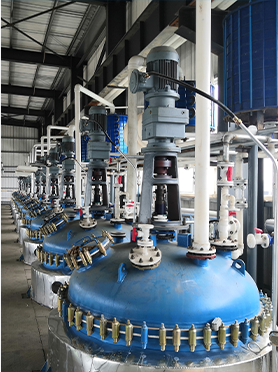
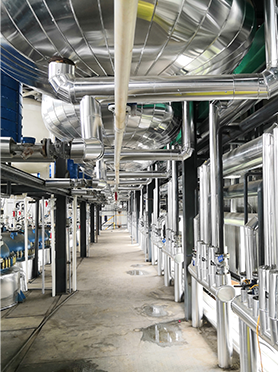
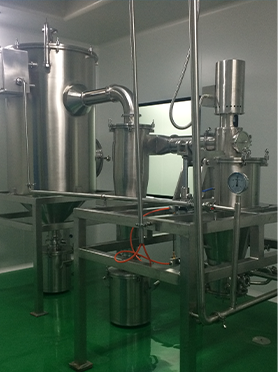
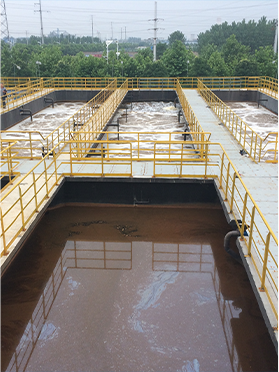
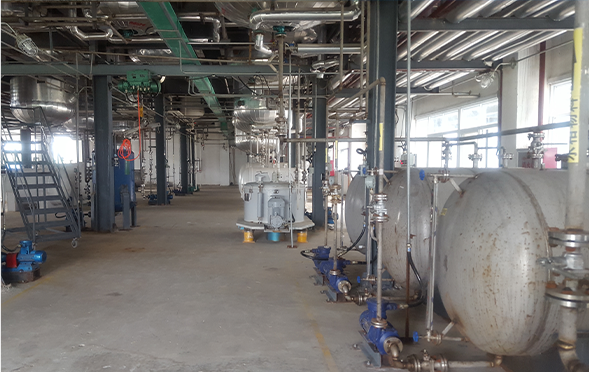
Manufacturing Facilities
Professional Export Experience
to Global Customers
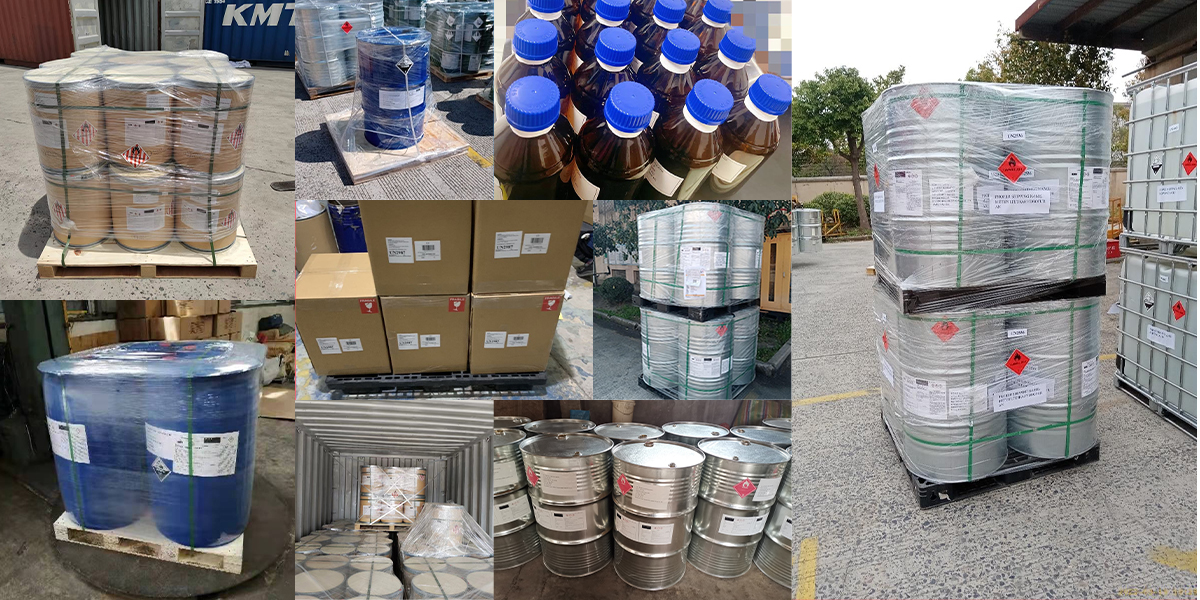
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.