Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
In the realm of industrial water treatment, maintaining the optimal performance and longevity of Reverse Osmosis (RO) membranes is paramount. The accumulation of scale and foulants on membrane surfaces can significantly diminish efficiency, increase operating costs, and ultimately lead to premature membrane failure. This is where high-quality RO membrane scale inhibitors and dispersants play a critical role. NINGBO INNO PHARMCHEM CO.,LTD. is at the forefront of providing advanced chemical solutions designed to combat these challenges effectively.
Scale formation is a common issue, often caused by dissolved mineral salts such as calcium carbonate, calcium sulfate, and barium sulfate, which precipitate onto membrane surfaces. Additionally, metal oxides, silicon compounds, and organic pollutants can contribute to fouling. The consequences are manifold: reduced permeate flux, increased transmembrane pressure, higher energy consumption, and ultimately, a need for more frequent cleaning or replacement of the RO membranes. Understanding how to prevent membrane scaling with reliable water treatment scale inhibitor products is key for any industrial operation relying on RO technology.
NINGBO INNO PHARMCHEM CO.,LTD.'s advanced dispersant for RO systems is formulated to address these issues head-on. It works by preventing the nucleation and growth of scale crystals, keeping them dispersed in the water and preventing them from adhering to the membrane. This active intervention ensures that the membranes remain clean and porous, facilitating efficient water flow and separation. For instance, their product excels at controlling inorganic scaling across a wide concentration range, allowing for higher LSI values without the need for acid addition. This makes the reverse osmosis antiscalant a safer and more effective solution.
Furthermore, the effectiveness of a good RO membrane scale inhibitor extends to its interaction with other contaminants. The products offered by NINGBO INNO PHARMCHEM CO.,LTD. are designed not to react with common foulants like iron, aluminum oxides, and silicon compounds, thus preventing the formation of insoluble substances that can further clog the membranes. This characteristic is vital for systems that handle water with high metal oxide content. The ability to manage iron, aluminum, and heavy metal pollutants, even at permissible iron concentrations up to 8.0ppm, highlights the robustness of these solutions.
The benefits of using a high-quality RO membrane scale inhibitor are directly translatable into tangible operational improvements. By using effective dispersant for RO systems, industries can achieve increased water production, improved water quality, and a significant reduction in operating costs. The enhanced performance means less downtime for cleaning and maintenance, and a longer service life for the RO membranes themselves. Companies looking to buy these essential chemicals can rely on the expertise and quality offered by NINGBO INNO PHARMCHEM CO.,LTD. for their water treatment scale inhibitor needs.
In conclusion, the selection of an appropriate RO membrane scale inhibitor is a strategic decision that impacts the economic and operational viability of industrial water treatment processes. NINGBO INNO PHARMCHEM CO.,LTD. provides advanced chemical solutions that are essential for maintaining the efficiency and extending the lifespan of RO membranes, ensuring a consistent supply of purified water. Their commitment to innovation and quality makes them a trusted partner for industries seeking effective water treatment solutions.
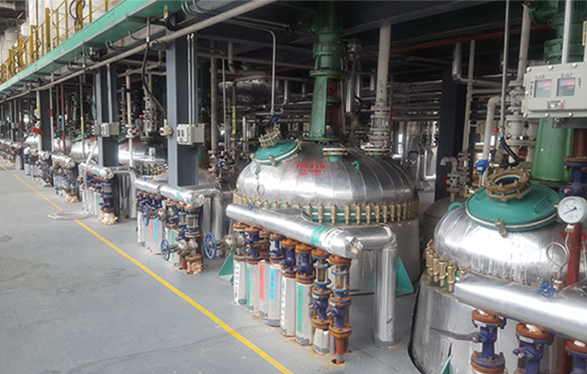
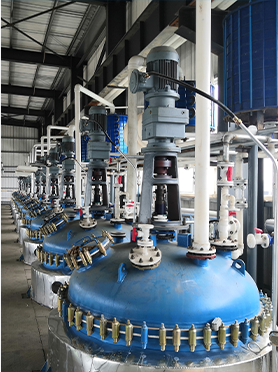
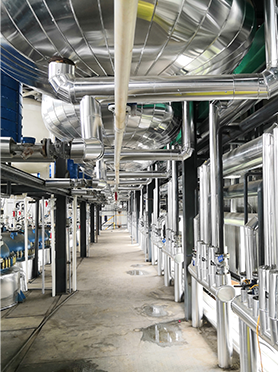
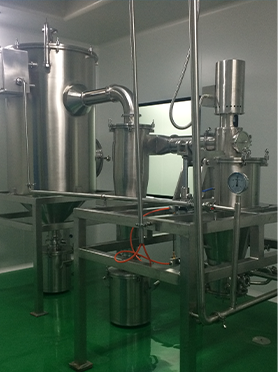
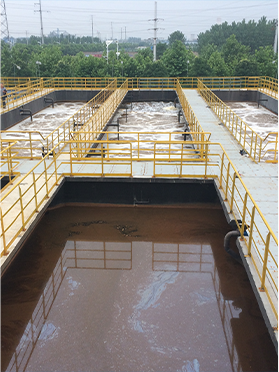
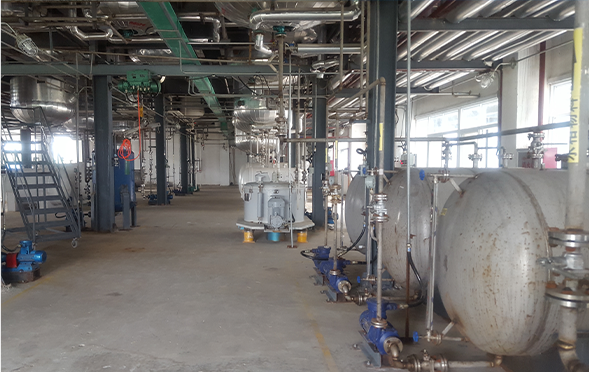
Manufacturing Facilities
Professional Export Experience
to Global Customers
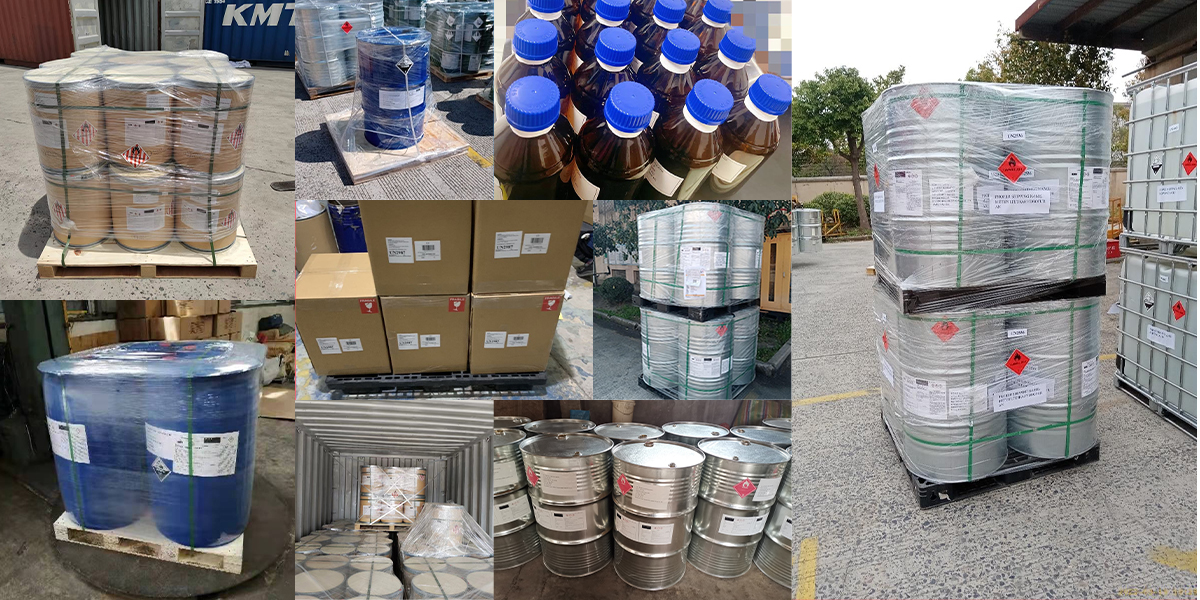
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.