Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
At NINGBO INNO PHARMCHEM CO.,LTD., we understand the critical importance of high-purity chemicals in advanced industrial processes. One such essential chemical is hydrogen peroxide (H2O2), widely used across various sectors from healthcare to electronics. The efficient and stable production of H2O2 relies heavily on specialized materials, and activated alumina plays a pivotal role in this intricate manufacturing process. Specifically, activated alumina serves as a key component in the anthraquinone method, the dominant industrial route for H2O2 synthesis.
The anthraquinone process involves a cyclic system where an anthraquinone derivative is hydrogenated, oxidized, and then extracted. During these stages, degradation products can form, potentially reducing the yield and purity of the H2O2. This is where high-quality activated alumina, such as those we supply, becomes indispensable. Our activated alumina products are engineered with a high specific surface area and a porous structure, making them excellent adsorbents and catalyst carriers. These properties allow them to effectively remove unwanted degradation products and impurities from the working solution.
One of the primary functions of activated alumina in this context is to act as a catalyst carrier, supporting the regeneration of the working solution. It helps in de-hydrogenation and de-epoxidation reactions, thereby maintaining the quality of the anthraquinone derivatives. Furthermore, its strong adsorption capabilities are crucial for removing polar degradation products that can accumulate over time. This continuous purification process ensures the stability of the working solution, leading to a more consistent and efficient H2O2 production. The ability to regenerate and maintain its activity after multiple cycles makes activated alumina a cost-effective solution for manufacturers.
The selection of the right activated alumina is paramount. Key performance indicators we focus on include high crushing strength to withstand process conditions, low sodium oxide content to prevent interference with the H2O2 formation, and a significant water absorption rate to manage moisture. These specifications ensure that our activated alumina not only performs its intended function but also contributes to the overall safety and stability of the H2O2 production plant. By partnering with NINGBO INNO PHARMCHEM CO.,LTD., you gain access to activated alumina that meets stringent industry standards, helping you optimize your H2O2 production and achieve superior product quality.
We are committed to providing solutions that enhance chemical manufacturing processes. Our expertise in sourcing and supplying high-performance chemical auxiliaries allows us to support your operational needs effectively. Whether you are looking to improve process stability, increase H2O2 yield, or reduce operational costs, our range of activated alumina products offers a reliable and efficient solution for your manufacturing challenges.
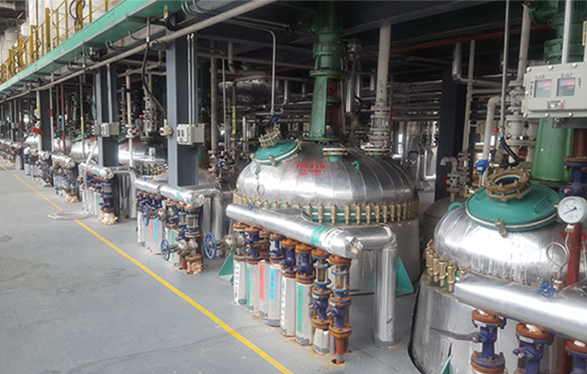
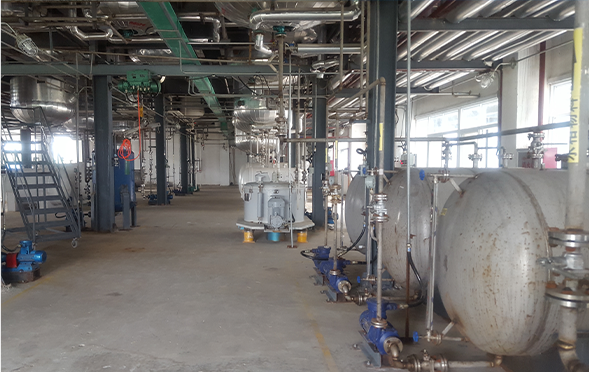
Manufacturing Facilities
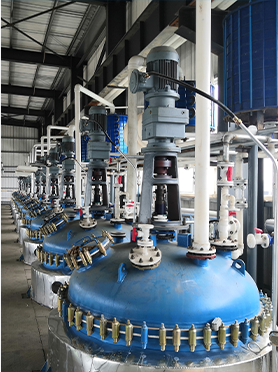
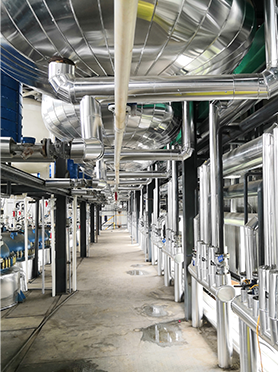
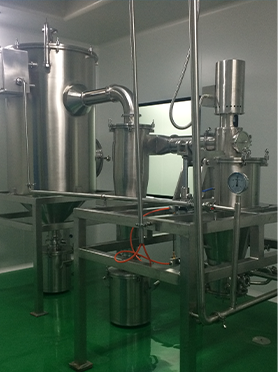
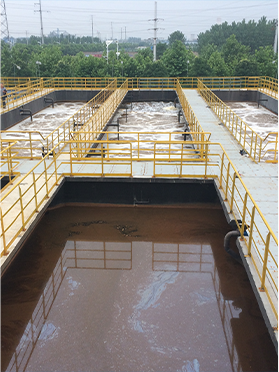
Professional Export Experience
to Global Customers
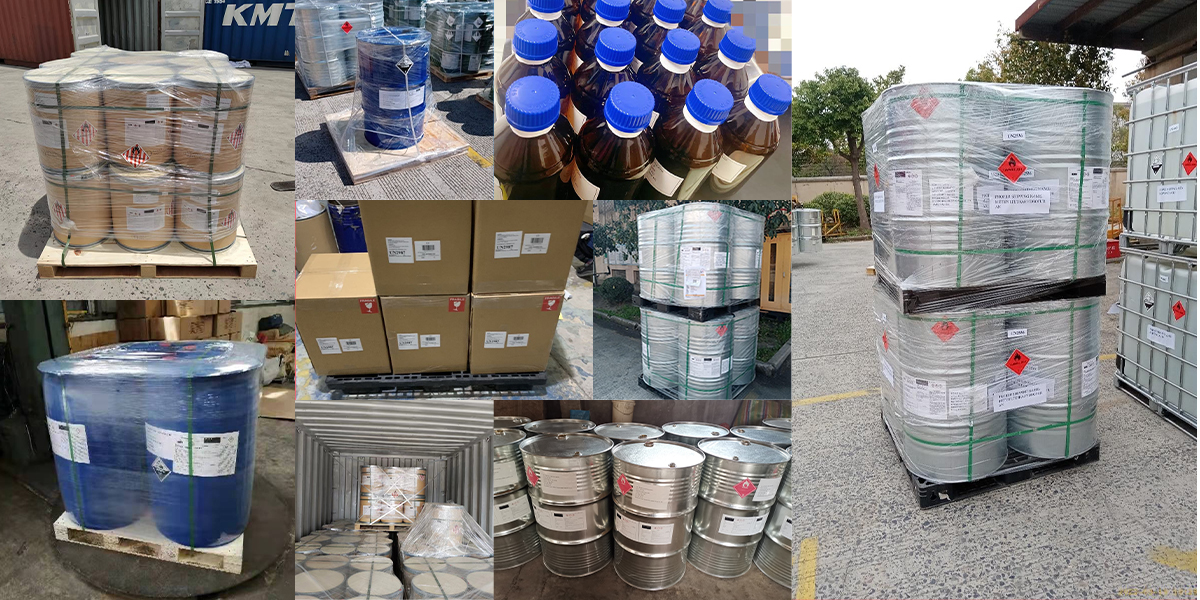
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.