Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
In the intricate world of pharmaceutical manufacturing, the quality and reliability of chemical intermediates are paramount. These compounds serve as the foundational building blocks for active pharmaceutical ingredients (APIs), directly impacting the efficacy, safety, and consistency of the final medicinal products. A prime example of such a critical intermediate is the compound used in the synthesis of Ribavirin, an essential antiviral medication widely recognized for its broad-spectrum activity.
The journey from raw chemicals to a finished drug involves complex multi-step synthesis. For Ribavirin, a key precursor molecule, often referred to by its CAS number 39925-10-5 and chemical name 1-(2,3,5-Tri-O-acetyl-beta-D-ribofuranosyl)-1H-1,2,4-triazole-3-carboxylic acid methyl ester, plays an indispensable role. Its specific molecular structure, featuring a protected ribofuranose moiety attached to a triazole ring with a methyl ester group, is meticulously designed to facilitate subsequent chemical transformations. The acetyl protection groups are crucial for managing reactivity during synthesis, ensuring that reactions proceed with the desired selectivity and yield.
The production of such high-purity intermediates is a testament to advancements in chemical synthesis and stringent quality control measures. Manufacturers, including those specializing in pharmaceutical intermediates, invest heavily in research and development to optimize synthetic routes, improve yields, and eliminate impurities. The demand for these intermediates is intrinsically linked to the global need for effective antiviral treatments. As viral infections continue to pose significant public health challenges, the reliable supply of Ribavirin and, consequently, its key intermediates becomes increasingly vital. Companies that can consistently provide intermediates that meet rigorous specifications are invaluable partners in the pharmaceutical ecosystem.
Beyond its direct application in Ribavirin production, this type of nucleoside analog intermediate also holds promise for broader pharmaceutical research. The unique structural features offer a platform for exploring modifications that could lead to the development of novel antiviral or even anticancer agents. Such research endeavors rely on the availability of well-characterized and high-quality starting materials. The continued innovation in pharmaceutical intermediate manufacturing, driven by a commitment to quality and efficiency, directly supports the advancement of modern medicine and the fight against disease. Exploring Ribavirin intermediate production processes helps illuminate the critical role these compounds play in bringing effective therapies to patients worldwide.
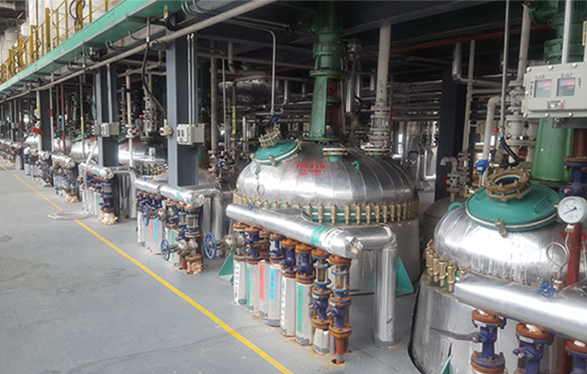
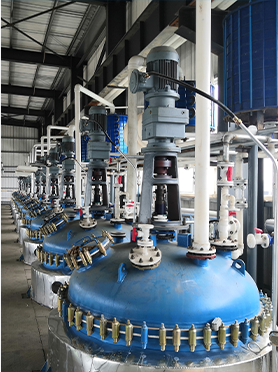
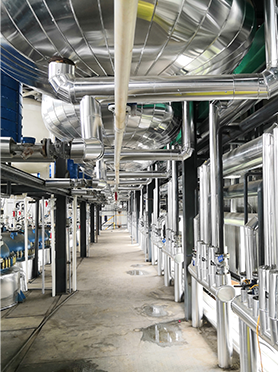
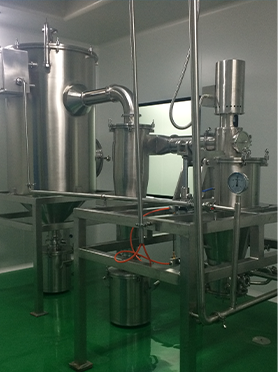
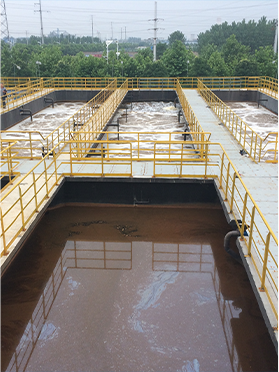
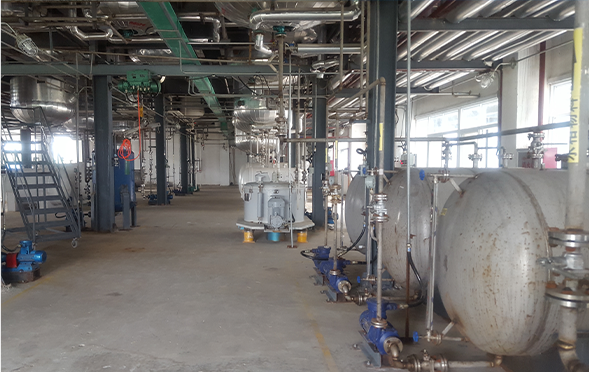
Manufacturing Facilities
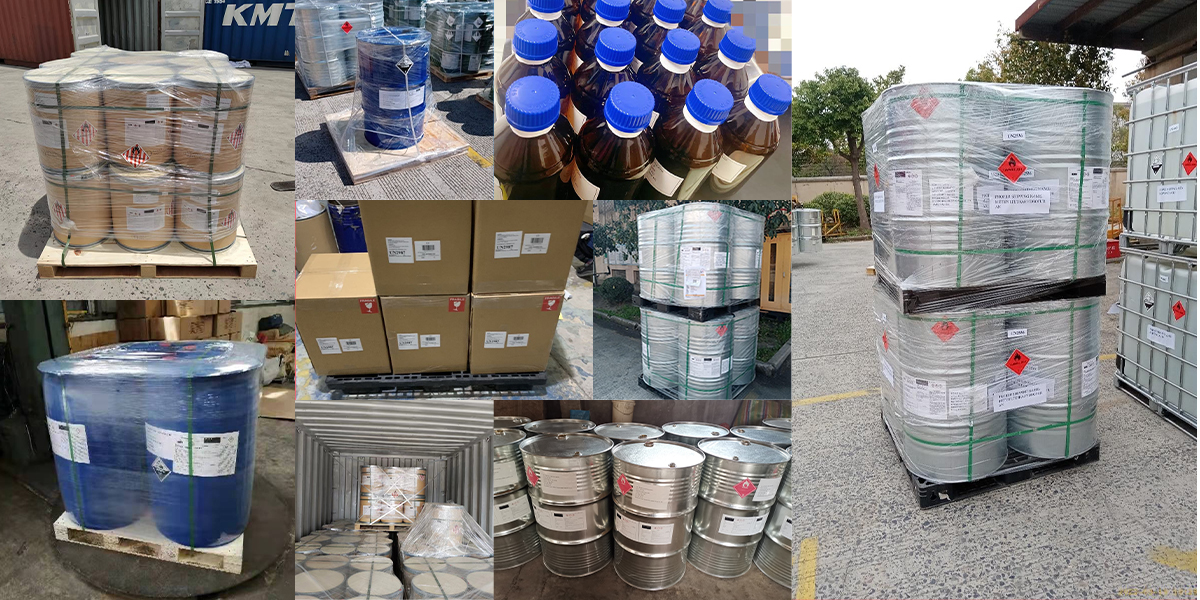
Professional Export Experience
to Global Customers
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.