Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
The efficacy of activated alumina in water treatment, particularly for removing substances like fluoride, is rooted in its unique physical and chemical properties. As a leading supplier of activated alumina, we understand the importance of detailing these mechanisms to our B2B clients, including procurement managers and R&D scientists, who seek to optimize their water purification processes. This article explores the adsorption mechanisms that make activated alumina a premier choice for water treatment applications.
Surface Chemistry and Adsorption Sites
Activated alumina is essentially aluminum oxide (Al2O3) processed to create a highly porous structure with a large surface area. The surface of activated alumina is characterized by hydroxyl groups (-OH), which can exist in various states depending on the pH of the surrounding water. These surface hydroxyl groups are the primary active sites responsible for adsorption. In water treatment, especially for fluoride removal, the surface chemistry plays a critical role. At specific pH levels, the surface can develop a positive charge, creating an electrostatic attraction for negatively charged ions like fluoride (F⁻).
Key Adsorption Mechanisms
Optimizing Adsorption Performance
The effectiveness of activated alumina is significantly influenced by several factors, including pH, initial contaminant concentration, contact time, and adsorbent dosage. Research indicates that optimal fluoride removal often occurs at a slightly acidic pH (around pH 5.5-6.0), where the alumina surface is positively charged and fluoride is present as F⁻ ions. Higher initial fluoride concentrations generally lead to higher adsorption capacities, up to the point where the active sites become saturated. Sufficient contact time is necessary for the adsorption process to reach equilibrium, and increasing the adsorbent dosage provides more active sites, thereby enhancing removal efficiency. As a dedicated supplier, we provide technical data and support to help our clients determine the optimal operating parameters for their specific water treatment challenges.
Why Choose Our Activated Alumina?
As a leading manufacturer and supplier of activated alumina, we ensure our products are engineered for maximum adsorption capacity and regenerability. Our activated alumina balls are produced under strict quality control to guarantee consistent performance for water treatment applications. By purchasing from us, you benefit from a reliable supply chain, competitive pricing, and expert technical support to help you achieve your water quality goals. We are committed to providing solutions that meet the highest industry standards.
For procurement managers and R&D scientists looking to buy activated alumina for water treatment, we offer high-quality products designed for superior performance. Contact us today to discuss your requirements and explore how our activated alumina can enhance your water purification systems.
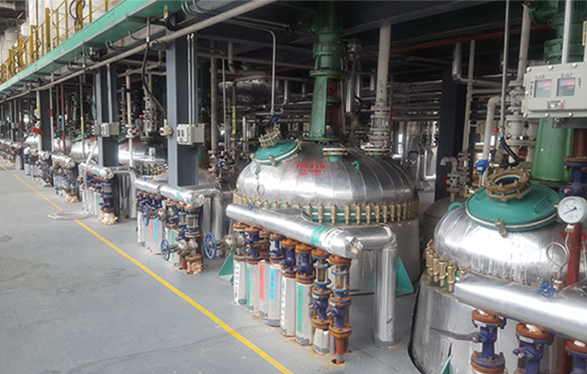
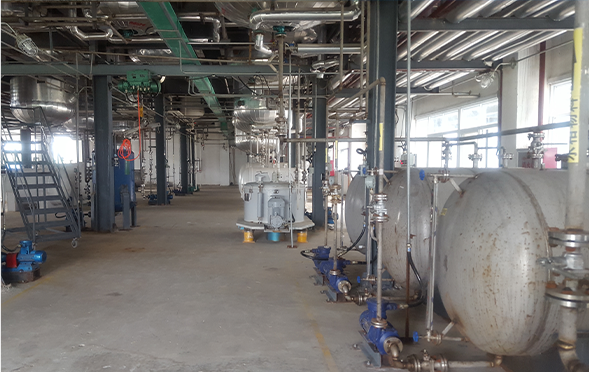
Manufacturing Facilities
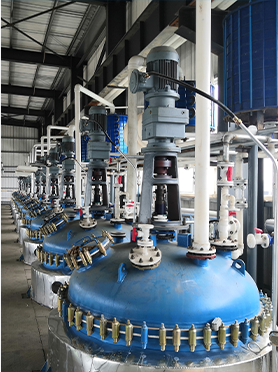
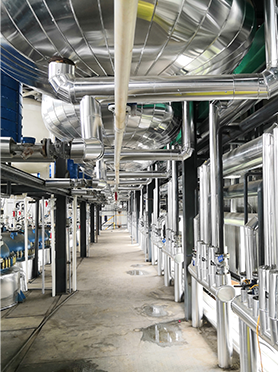
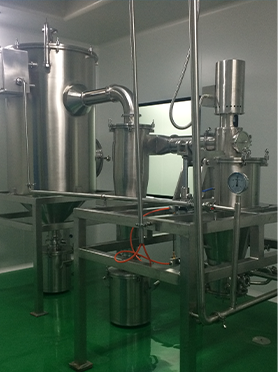
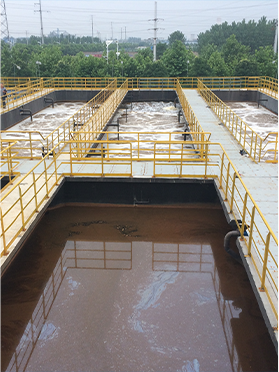
Professional Export Experience
to Global Customers
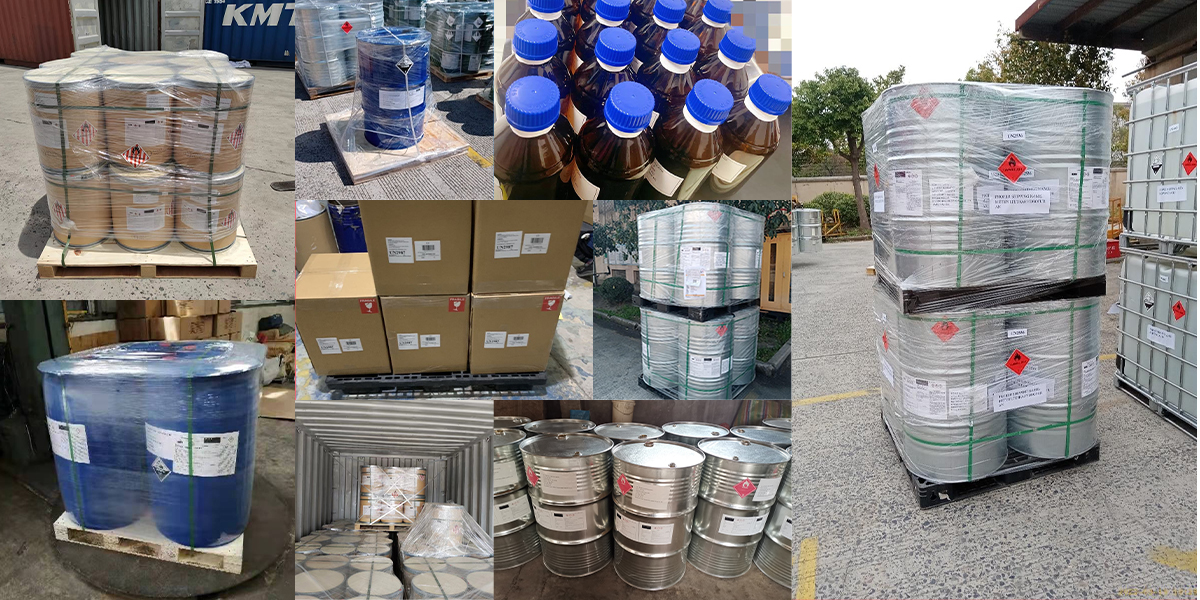
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.