Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
Vitamin E is a collective term for a group of fat-soluble compounds, with alpha-tocopherol being the most biologically active form for humans. As a crucial nutrient, it plays a vital role in protecting cells from oxidative damage, supporting immune function, and maintaining healthy skin and eyes. For businesses in the pharmaceutical, cosmetic, and nutraceutical industries, understanding the nuances of Vitamin E and securing a reliable supply of high-quality product is essential. As a dedicated Vitamin E manufacturer and supplier, we provide clarity on these aspects.
The primary function of Vitamin E is its role as a potent antioxidant. It intercepts free radicals, unstable molecules that can damage cells and contribute to aging and various chronic diseases. This antioxidant capability makes Vitamin E a highly sought-after ingredient for products aimed at health promotion and disease prevention. When you buy Vitamin E from a trusted supplier, you are ensuring that your formulations benefit from this crucial protective function.
Several forms of Vitamin E exist, including tocopherols and tocotrienols, each with varying biological activities. Alpha-tocopherol is the most widely recognized and studied form, and it's often the focus for supplementation and therapeutic applications. For formulators, understanding the specific form and purity required for their application is key. As a Vitamin E supplier, we offer products that meet stringent quality specifications, often identified by CAS numbers like 14638-18-7, which denotes a specific derivative often used in various applications.
The importance of sourcing Vitamin E from a reputable manufacturer cannot be overstated. Quality control, purity, and consistency are critical, especially for pharmaceutical and nutraceutical applications. A reliable supplier ensures that the Vitamin E provided meets all necessary standards, thus safeguarding the integrity of the end product. We pride ourselves on being a manufacturer that prioritizes these aspects, offering competitive pricing and excellent customer support to those looking to purchase Vitamin E.
Whether you are developing advanced skincare products, health supplements, or pharmaceutical formulations, integrating high-quality Vitamin E is a strategic decision. As an experienced Vitamin E supplier and manufacturer in China, we are equipped to meet your diverse needs. We encourage you to reach out to us to learn more about our product offerings and to secure a dependable source for your Vitamin E requirements, ensuring the efficacy and safety of your products.
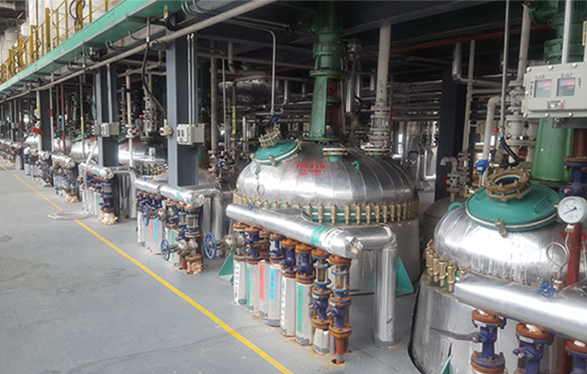
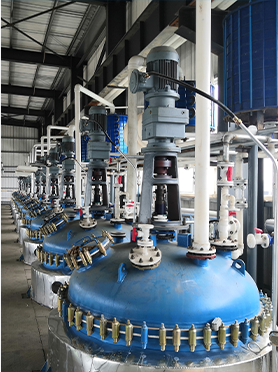
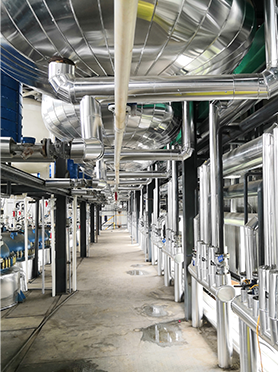
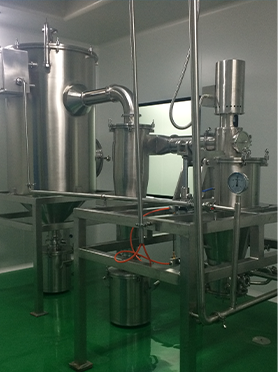
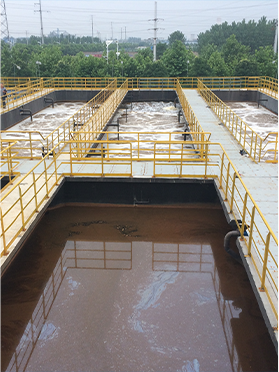
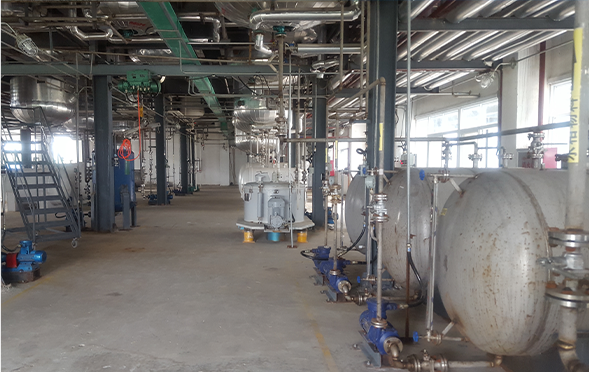
Manufacturing Facilities
Professional Export Experience
to Global Customers
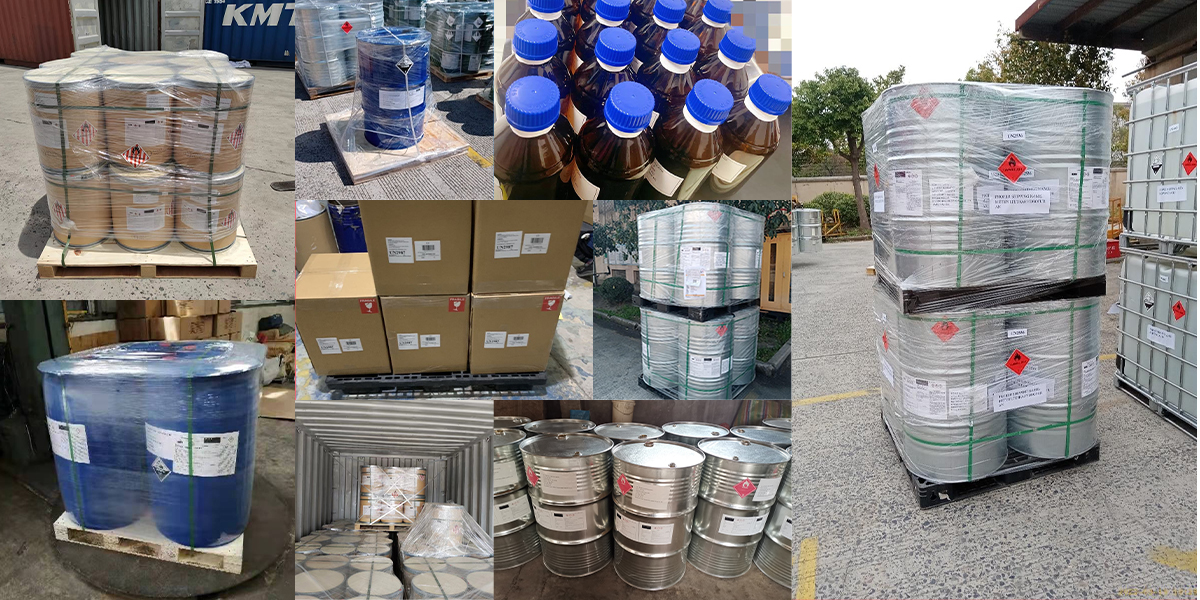
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.