Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
At NINGBO INNO PHARMCHEM CO.,LTD., we recognize the profound impact of Sodium Alginate in the pharmaceutical industry. The medical applications of Sodium Alginate are diverse and scientifically validated, establishing it as a vital excipient in numerous formulations. Understanding its properties is key for developing effective and stable pharmaceutical products.
Sodium Alginate is widely employed as a suspending agent, ensuring that insoluble drug particles remain evenly dispersed in liquid formulations, thereby guaranteeing accurate dosage with each administration. Its excellent viscosity-enhancing properties also contribute to the stability and texture of suspensions and emulsions. When manufacturers buy sodium alginate online from reputable sources like ours, they ensure the consistent performance required for pharmaceutical-grade materials.
Furthermore, Sodium Alginate is utilized as a matrix material for microencapsulation, a crucial technique in controlled drug release. This allows for the protection of active pharmaceutical ingredients and the precise modulation of drug delivery profiles. The ability to tailor these properties makes Sodium Alginate an invaluable component in advanced pharmaceutical formulations. The detailed specifications for sodium alginate CAS 9005-38-3 highlight its suitability for these demanding applications.
Beyond its traditional roles, research is continually exploring new sodium alginate medical applications. Its biocompatibility and biodegradability make it an attractive candidate for novel drug delivery systems, including mucoadhesive formulations and wound dressings. The benefits of Alginic Acid Sodium Salt extend to patient comfort and therapeutic efficacy, making it a compound of significant interest.
For pharmaceutical companies seeking a reliable sodium alginate supplier, NINGBO INNO PHARMCHEM CO.,LTD. offers high-purity Sodium Alginate that meets stringent regulatory requirements. Our commitment to quality ensures that our products contribute to the safety and effectiveness of the medicines you develop. We aim to be your trusted partner in sourcing essential pharmaceutical intermediates and excipients.
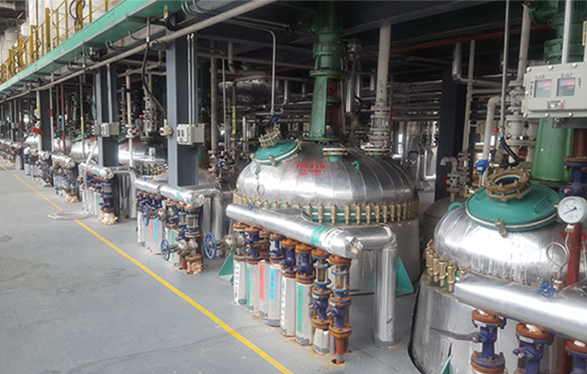
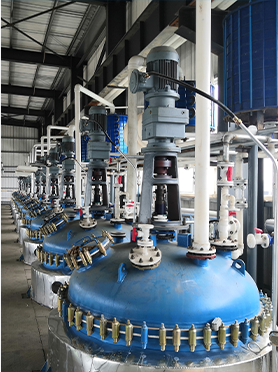
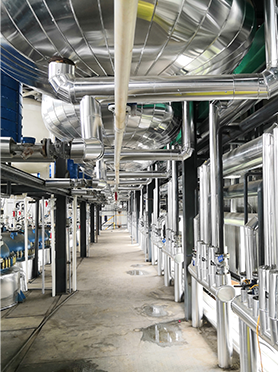
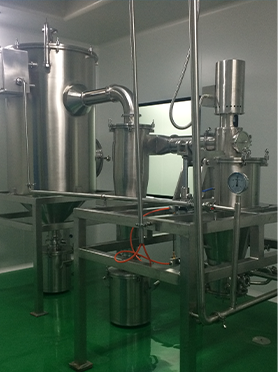
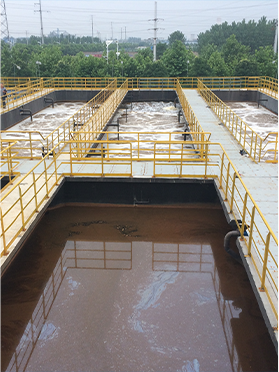
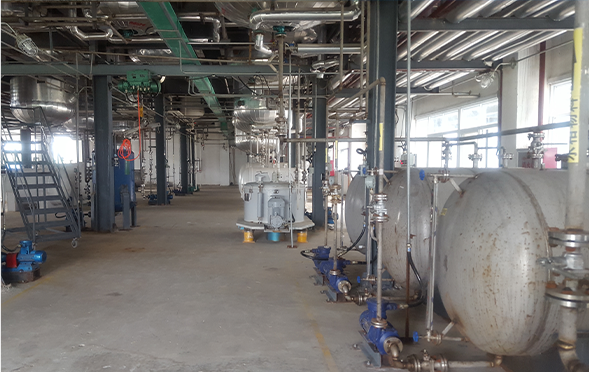
Manufacturing Facilities
Professional Export Experience
to Global Customers
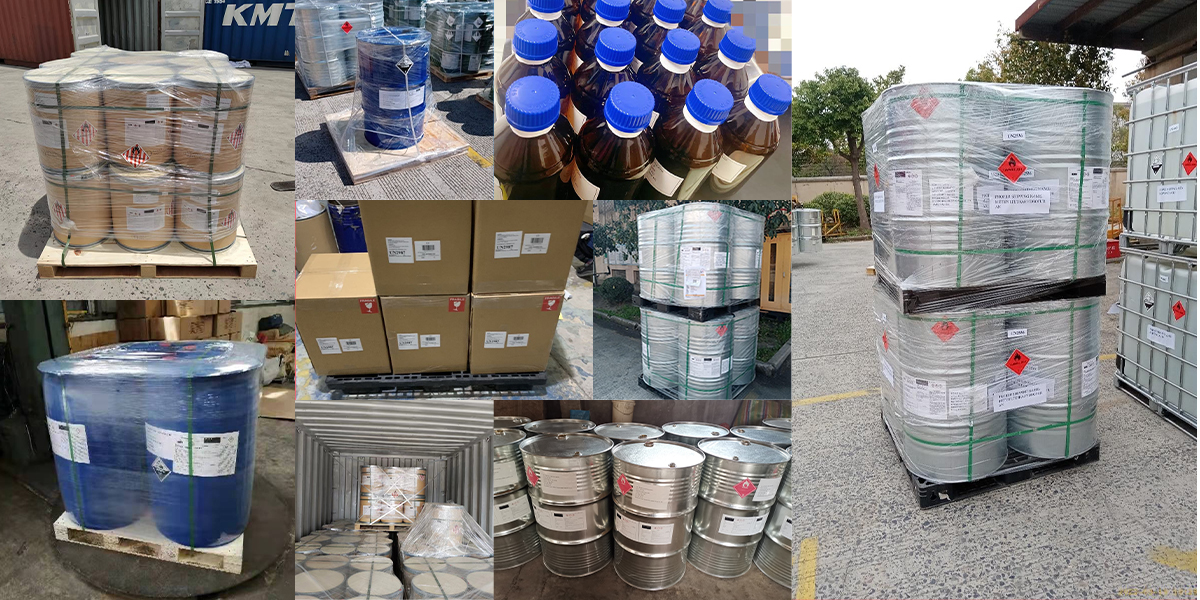
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.