Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
For companies operating in the pharmaceutical sector, the sourcing of raw materials demands the highest standards of purity, consistency, and regulatory compliance. Vitamin A (CAS 11103-57-4), in its pharmaceutical-grade form, is a critical component in various drug formulations, particularly those related to ophthalmology, dermatology, and immune support. Understanding how to procure this vital nutrient from reliable sources, such as leading manufacturers in China, is essential for product development and patient safety.
Pharmaceutical Grade Vitamin A: The Quality Imperative
Pharmaceutical applications require Vitamin A that meets stringent quality specifications. This typically means high purity levels (often 99%), rigorous testing, and compliance with pharmacopoeial standards (e.g., USP, EP, JP). The CAS number 11103-57-4 is a key identifier for specifying this critical raw material. Pharmaceutical manufacturers rely on Vitamin A for its therapeutic properties, including its role in vision, cell differentiation, and immune modulation. Ensuring the integrity of the supply chain from the Vitamin A manufacturer is paramount to maintaining the quality and safety of the final pharmaceutical product.
Sourcing Pharmaceutical Vitamin A from China
China has become a significant global supplier of pharmaceutical raw materials, offering a compelling combination of advanced manufacturing capabilities and competitive pricing. When seeking to buy Vitamin A for pharmaceutical use, consider partnering with Chinese manufacturers who demonstrate:
As a premier Vitamin A manufacturer in China, we are dedicated to meeting the exacting standards of the pharmaceutical industry. Our Vitamin A (CAS 11103-57-4) is produced under strict cGMP conditions, ensuring the high purity and reliability required for pharmaceutical applications. We understand the critical nature of pharmaceutical sourcing and are committed to providing transparent and dependable supply chains. Let us be your trusted Vitamin A supplier for your critical drug development and manufacturing needs.
Procurement Best Practices for Pharmaceutical Vitamin A
To ensure a successful sourcing strategy:
By prioritizing these elements, pharmaceutical companies can secure a reliable and high-quality supply of Vitamin A, critical for developing safe and effective medicines. Partner with us for your pharmaceutical-grade Vitamin A needs, and experience the benefits of working with a leading Chinese manufacturer dedicated to excellence.
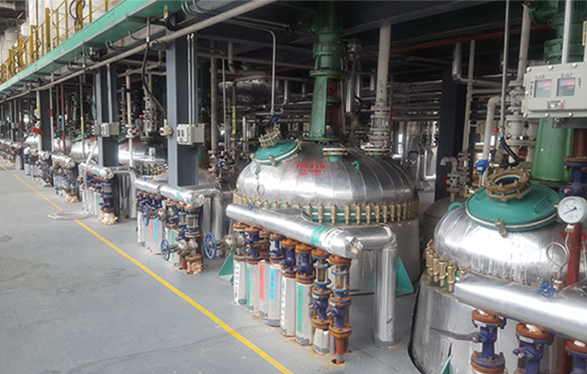
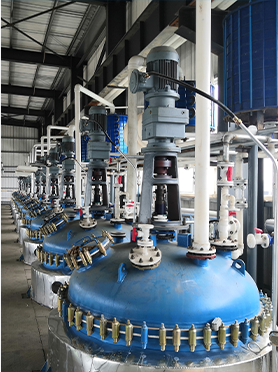
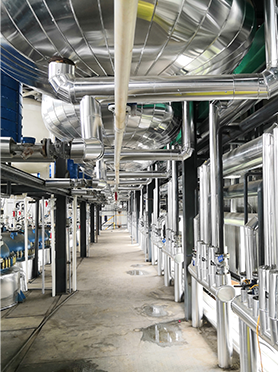
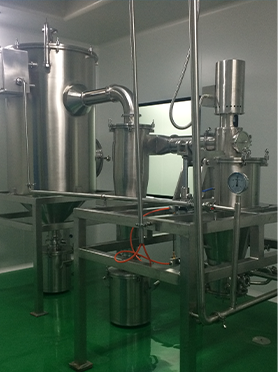
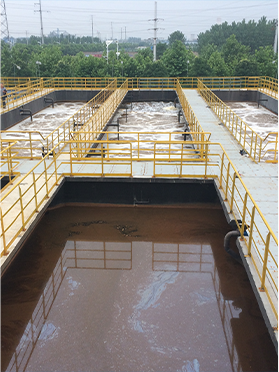
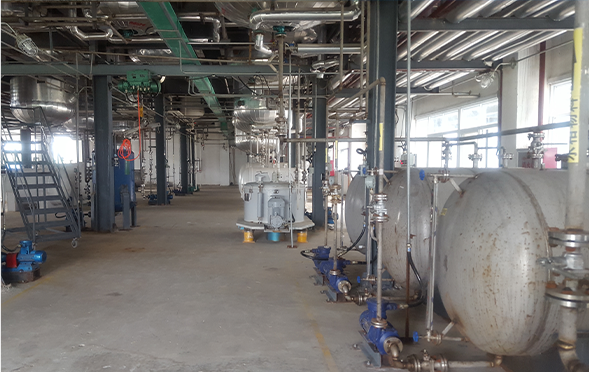
Manufacturing Facilities
Professional Export Experience
to Global Customers
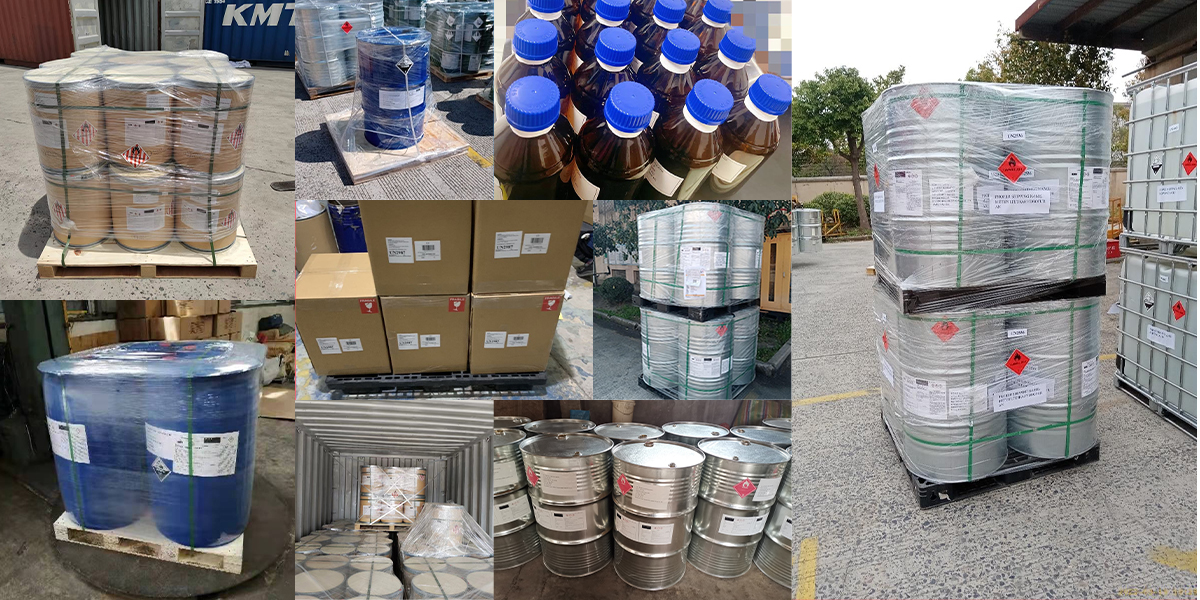
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.