Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
In the competitive food and beverage industry, maintaining product freshness and extending shelf life are critical for success. Natural antioxidants play a vital role in preventing lipid oxidation, a primary cause of spoilage in many food products, particularly those containing fats and oils. Among the most effective and widely recognized natural antioxidants is Vitamin E, specifically alpha-Tocopherol (CAS 59-02-9).
Vitamin E, also known as tocopherol, is a fat-soluble vitamin that acts as a potent antioxidant. It effectively neutralizes free radicals, thereby inhibiting the chain reactions that lead to rancidity and the degradation of flavor, color, and nutritional value in food products. Its efficacy makes it a preferred choice for manufacturers looking to replace synthetic antioxidants with natural alternatives.
Food manufacturers commonly incorporate Vitamin E into a diverse range of products, including vegetable oils, margarines, baked goods, cereals, snacks, and processed meats. By acting as a 'chain-breaking' antioxidant, it protects unsaturated fatty acids from oxidation, ensuring that products remain appealing and safe for consumption over extended periods. This makes it an essential ingredient for maintaining product quality and consumer satisfaction.
When sourcing Vitamin E for food applications, it is crucial to work with a trusted supplier that can provide food-grade material. The CAS number 59-02-9 signifies the alpha-Tocopherol isomer, the most biologically active and commonly used form. A reputable Vitamin E manufacturer will offer products that meet international food safety standards and provide comprehensive documentation, such as ISO certifications and specifications for purity and origin.
Procurement specialists in the food industry often seek competitive pricing and reliable delivery for bulk ingredients. Buying Vitamin E in larger quantities from established suppliers ensures cost-effectiveness and a stable supply chain, which is vital for uninterrupted production. Exploring options from leading Vitamin E manufacturers can lead to significant benefits in terms of quality, price, and technical support.
In essence, Vitamin E is an invaluable natural antioxidant for the food industry. Its ability to prevent oxidation and maintain product quality makes it a key ingredient for a wide range of applications. By choosing to buy Vitamin E from certified suppliers, food manufacturers can enhance their product's stability, appeal, and nutritional value, ultimately contributing to consumer trust and brand reputation. Partnering with a dedicated Vitamin E supplier is a strategic step towards achieving these goals.
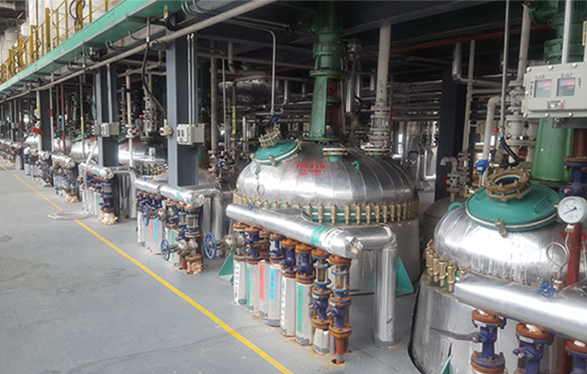
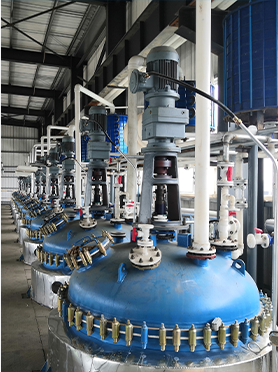
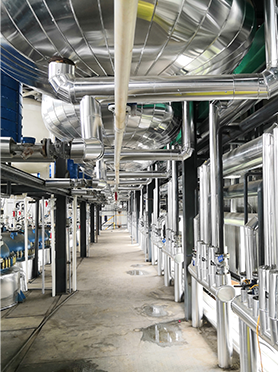
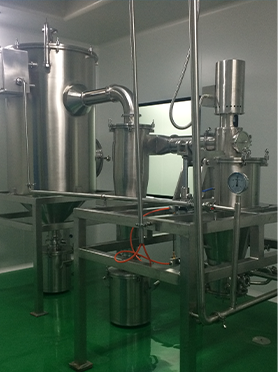
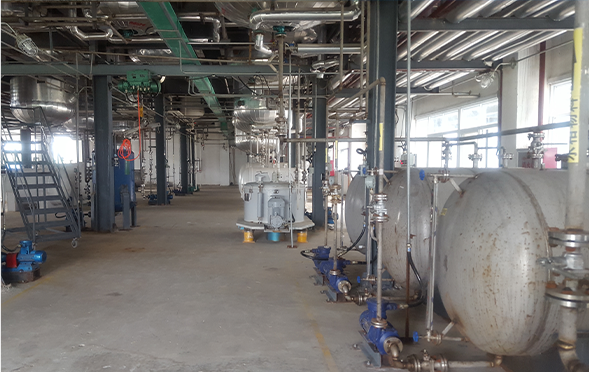
Manufacturing Facilities
Professional Export Experience
to Global Customers
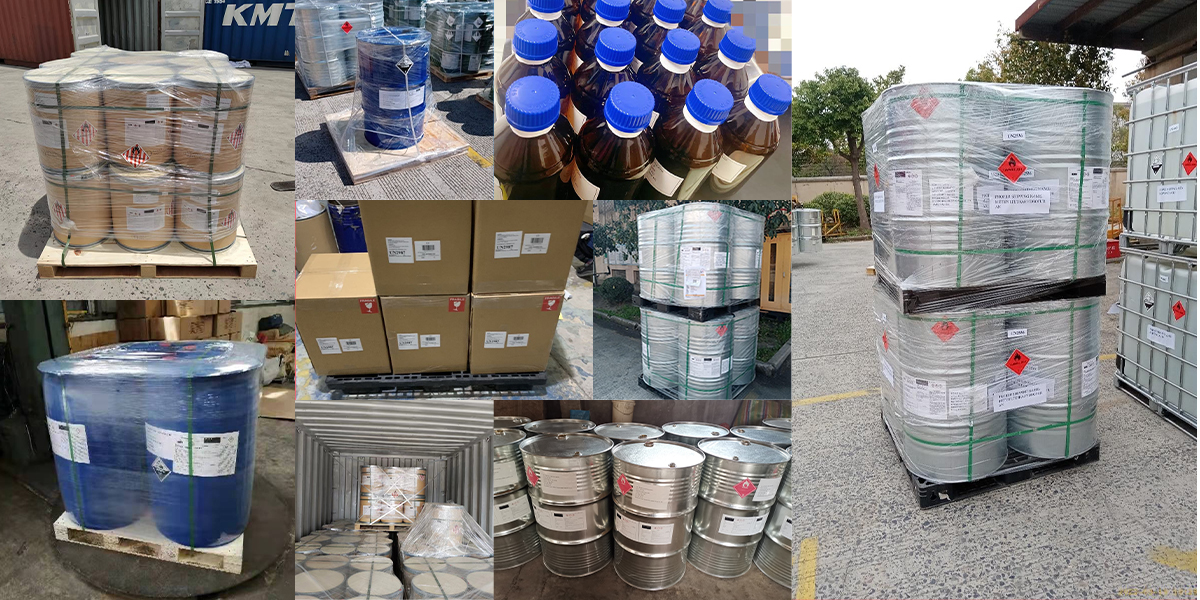
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.