Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
For businesses operating in the pharmaceutical, cosmetic, food, or animal nutrition sectors, securing a consistent and high-quality supply of Vitamin E (CAS 59-02-9) is a critical operational requirement. The selection of a Vitamin E manufacturer and supplier directly impacts product quality, cost-effectiveness, and supply chain reliability. This guide aims to help B2B buyers navigate the market and make informed sourcing decisions.
Understanding Product Specifications: Vitamin E exists in eight different forms, but alpha-Tocopherol is the most biologically active and commonly sought after for commercial applications. When sourcing, look for specifications that detail the purity (e.g., >99%), the specific isomer content (e.g., D-alpha-Tocopherol), and compliance with relevant pharmacopeias or food-grade standards. The CAS number 59-02-9 is your key identifier.
Choosing the Right Supplier: A reputable Vitamin E supplier will demonstrate a commitment to quality assurance, backed by certifications like ISO or GMP. They should offer comprehensive product documentation, including Certificates of Analysis (CoAs) for each batch, detailing critical parameters. Responsiveness to inquiries, transparent communication, and a robust quality control system are hallmarks of a reliable partner. Many leading manufacturers are located in China, known for their significant production capacity and competitive pricing.
Securing Competitive Pricing: To buy Vitamin E at competitive prices, consider purchasing in bulk. Establishing a long-term relationship with a preferred supplier can also lead to better pricing and preferential terms. Market research and obtaining multiple quotes from different manufacturers are essential steps in the procurement process. Factors influencing Vitamin E price include raw material costs, production volume, and global demand.
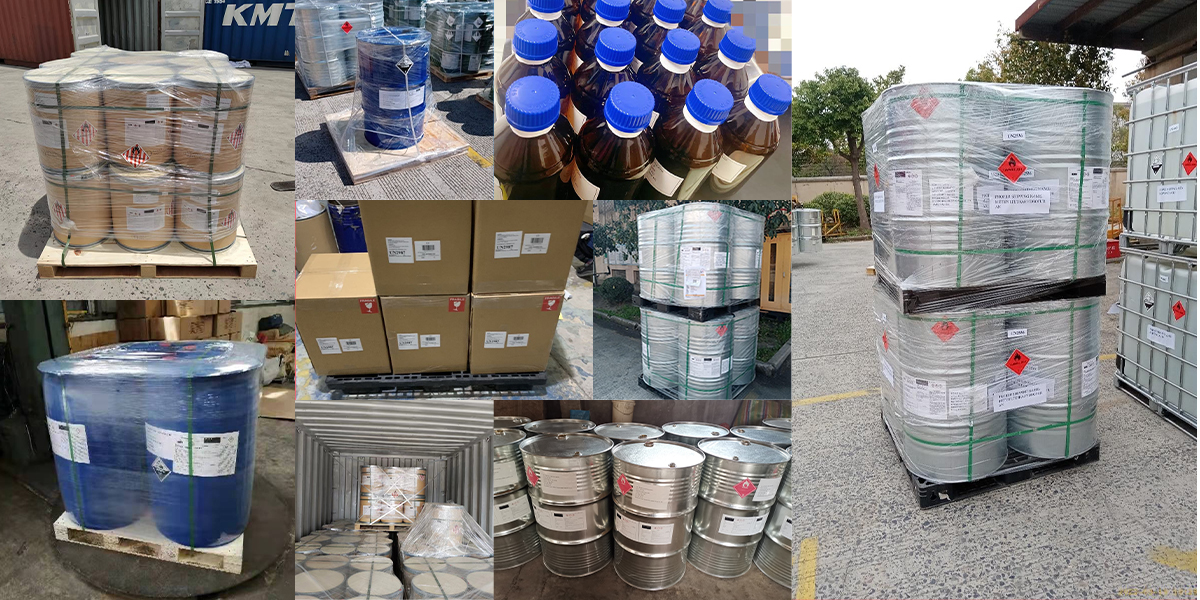
Navigating Logistics and Delivery: The timely delivery of Vitamin E is crucial for maintaining production schedules. Discuss shipping options, lead times, and packaging requirements with your chosen supplier. Whether you require small quantities for R&D or bulk shipments for manufacturing, a well-organized logistics network is vital.
In conclusion, selecting the right Vitamin E supplier is a strategic decision that influences product quality and business profitability. By focusing on purity, regulatory compliance, supplier reliability, and competitive pricing, procurement professionals can ensure a stable and high-quality supply of Vitamin E (CAS 59-02-9) for their diverse industrial needs. Engage with trusted Vitamin E manufacturers to build a strong and dependable supply chain.
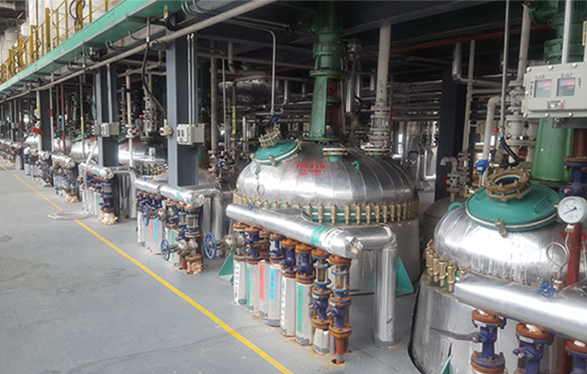
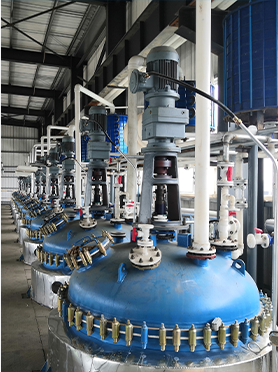
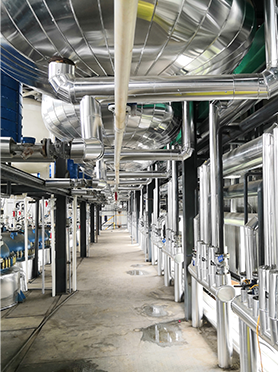
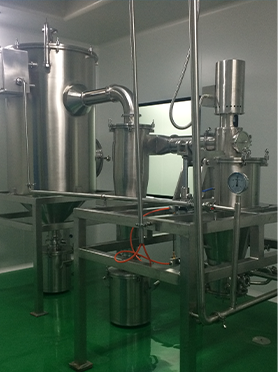
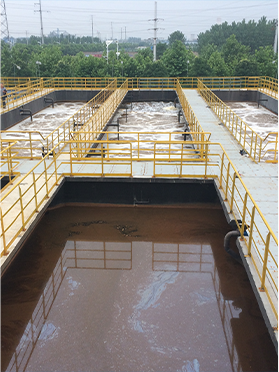
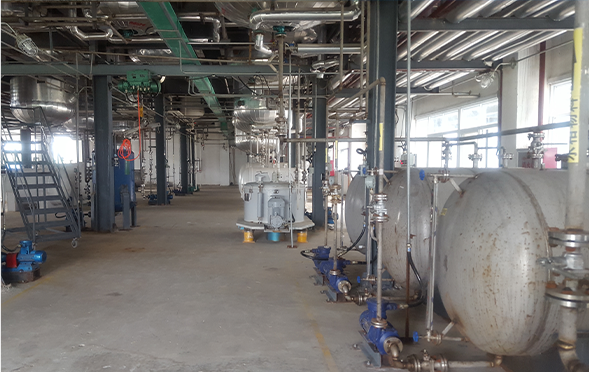
Manufacturing Facilities
Professional Export Experience
to Global Customers
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.