Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
In the demanding landscape of industrial operations, maintaining high water quality is paramount. From ensuring product integrity to meeting stringent environmental regulations, effective water treatment is non-negotiable. Among the array of solutions available, coal granular activated carbon (GAC) stands out as a highly effective and economical choice. As a leading manufacturer and supplier, we understand the critical role GAC plays, and this article delves into why it's indispensable for industrial water treatment.
Coal-based GAC is renowned for its robust physical and chemical properties. Derived from high-quality anthracite, it possesses a highly developed pore structure and an extensive specific surface area. These characteristics are fundamental to its superior adsorption capabilities, allowing it to efficiently capture a wide spectrum of contaminants from water. This makes it an attractive option for businesses looking to buy activated carbon that delivers consistent performance.
The primary advantage of coal GAC in industrial water treatment lies in its ability to remove dissolved organic matter, chlorine, and other impurities that can compromise water quality. Its effectiveness extends to treating wastewater streams, ensuring that discharged water meets environmental standards. For companies seeking reliable water purification chemical suppliers, our coal GAC offers a dependable solution.
Beyond water treatment, the versatility of coal GAC is evident in its applications in flue gas purification and organic solvent recycling. In industrial processes, capturing harmful emissions is as crucial as purifying water. The high adsorption capacity of GAC makes it ideal for removing toxic gases and volatile organic compounds (VOCs) from air streams, contributing to cleaner industrial environments.
Furthermore, the economic advantages of sourcing directly from a manufacturer in China cannot be overstated. By cutting out intermediaries, businesses can secure high-quality coal granular activated carbon at competitive prices. This cost-effectiveness, coupled with the material's inherent performance benefits, makes it a strategic procurement choice. We pride ourselves on being a trusted supplier that meets the needs of global industries.
When considering industrial water treatment chemicals, the choice of adsorbent significantly impacts operational efficiency and cost. Coal granular activated carbon, with its proven efficacy, durability, and economic viability, represents a smart investment. For businesses looking to buy activated carbon that ensures purity and compliance, partnering with a reputable manufacturer and supplier is key.
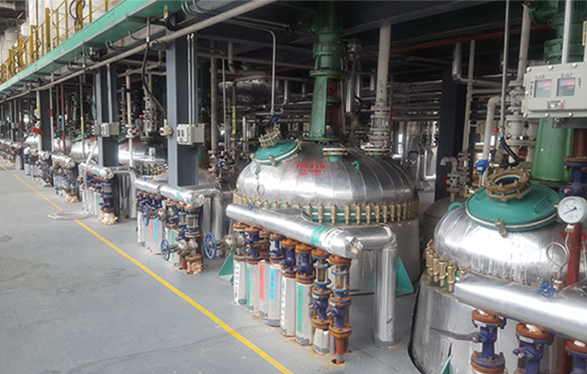
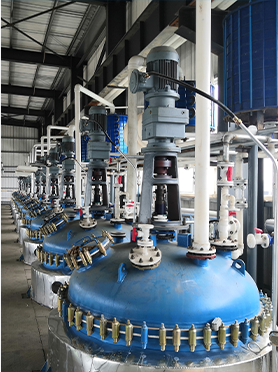
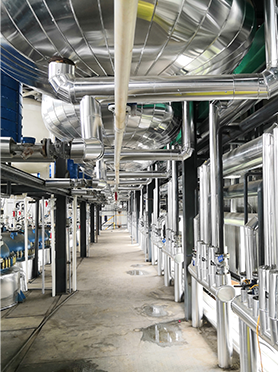
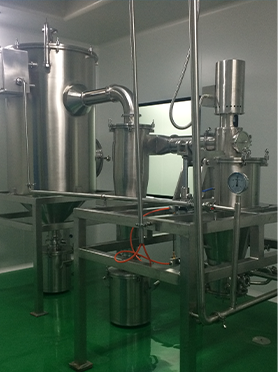
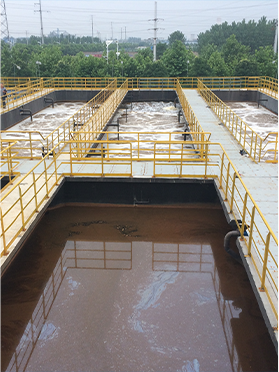
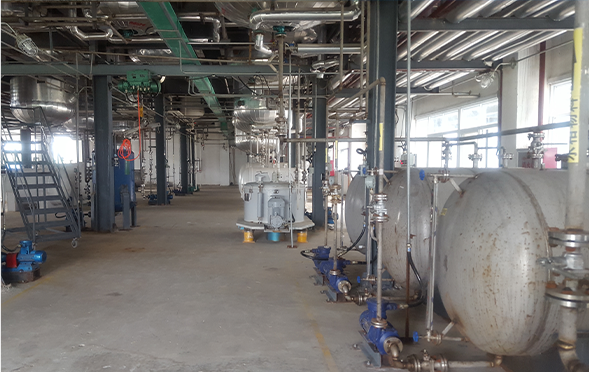
Manufacturing Facilities
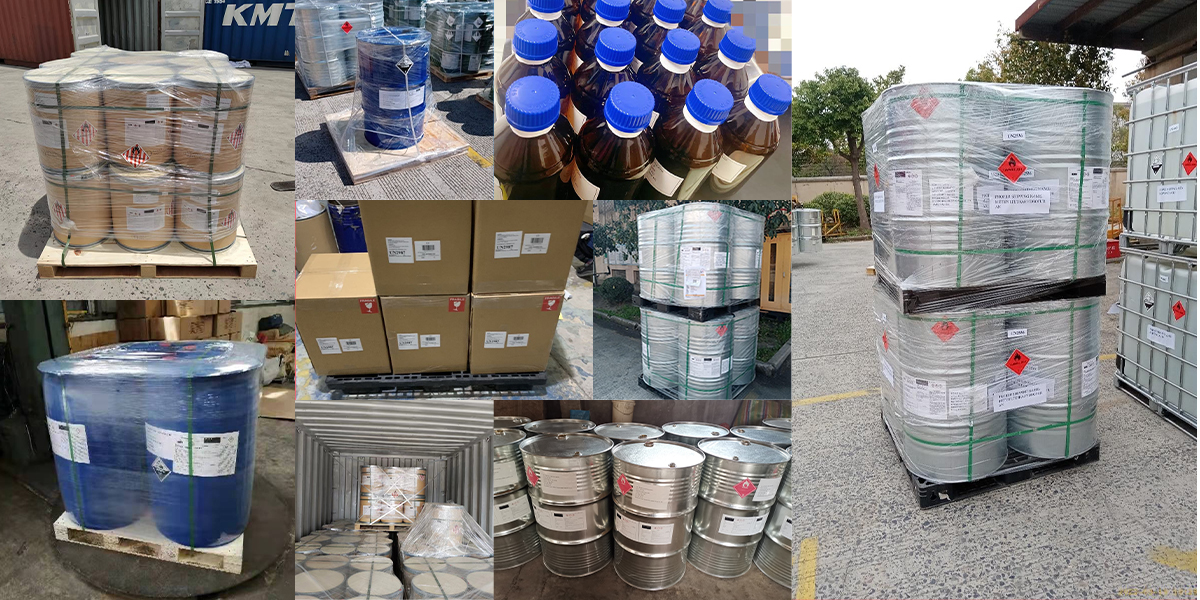
Professional Export Experience
to Global Customers
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.