Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
For product development engineers and procurement managers in the polymer industry, achieving stringent fire safety standards without compromising material performance or cost-effectiveness is a constant challenge. Traditional flame retardants often come with drawbacks, such as the release of toxic gases or a significant impact on material properties. This has led to a growing demand for advanced, safer alternatives. Zinc borate stands out as a highly effective and versatile additive that addresses these concerns, particularly for plastics and elastomers. As a dedicated supplier of specialty chemicals, we understand the critical role Zinc Borate plays in modern polymer formulations.
Understanding the Mechanism for Polymer Applications
Zinc borate (CAS: 1332-07-6) functions as a multi-purpose additive in polymers. Its primary role is as a flame retardant and smoke suppressant. When a polymer containing zinc borate is exposed to heat, the zinc borate undergoes decomposition. This process releases water vapor, which dilutes the flammable gases released by the decomposing polymer and also helps to cool the material. Simultaneously, the decomposition leaves behind a residue of boron oxide. This boron oxide forms a glassy, protective layer on the surface of the polymer. This layer acts as a barrier, preventing oxygen from reaching the polymer and hindering the escape of volatile combustible gases. Furthermore, zinc borate is recognized for its anti-dripping properties, preventing molten polymer from falling and spreading the fire. In applications like electrical insulation, it also helps to suppress arcing and tracking, which are electrical discharge phenomena that can lead to fires.
Synergy: The Power of Combination
A key advantage that makes Zinc Borate a preferred choice for many polymer manufacturers is its synergistic effect when combined with other flame retardant systems. It can be used in conjunction with halogen-containing flame retardants, often in combination with antimony trioxide, where it catalyzes the release of halogens and promotes char formation. More significantly, in the growing market for halogen-free solutions, zinc borate shows remarkable synergy with other inorganic flame retardants such as aluminum trihydrate (ATH), magnesium hydroxide (MH), and red phosphorus. By combining these additives, formulators can achieve superior flame retardancy, reduced smoke emission, and improved heat release characteristics, often at lower total additive loadings. This makes our Zinc Borate a cost-effective solution for achieving high-performance fire safety.
Benefits Beyond Flame Retardancy
Beyond its primary fire-retardant capabilities, Zinc Borate offers several other advantages for polymer applications:
Sourcing High-Quality Zinc Borate
For businesses looking to buy Zinc Borate, partnering with a reliable manufacturer and supplier is essential. We offer high-purity Zinc Borate, ensuring consistent performance and compliance with international standards. Our facility in China is equipped to produce Zinc Borate that meets the demanding specifications of the polymer industry. Whether you are working with PVC, polyolefins, polyamides, epoxy resins, or other polymer systems, our Zinc Borate can significantly enhance your product's fire safety profile. Contact us today to inquire about pricing, lead times, and to secure a dependable supply of this vital additive.
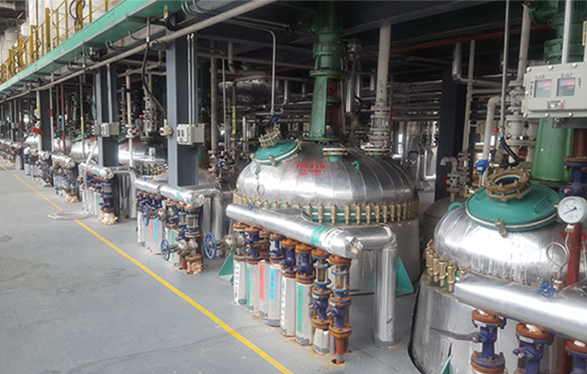
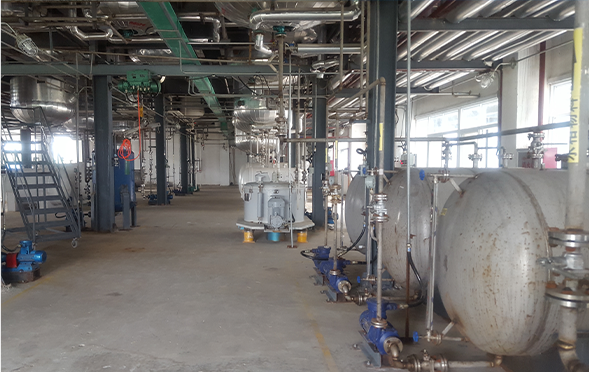
Manufacturing Facilities
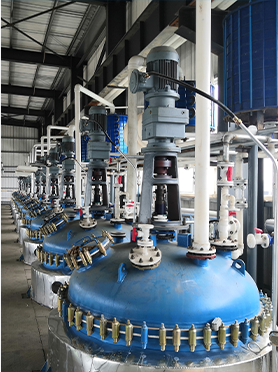
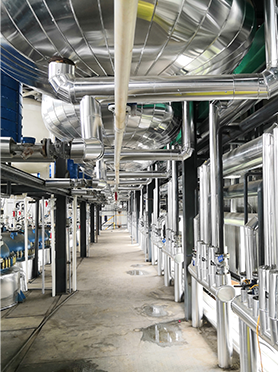
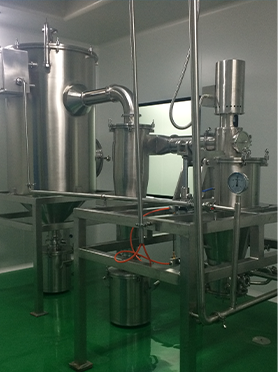
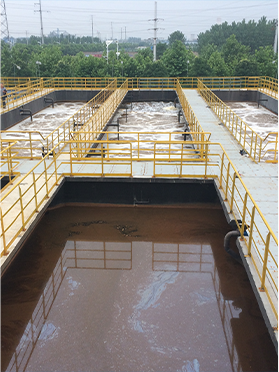
Professional Export Experience
to Global Customers
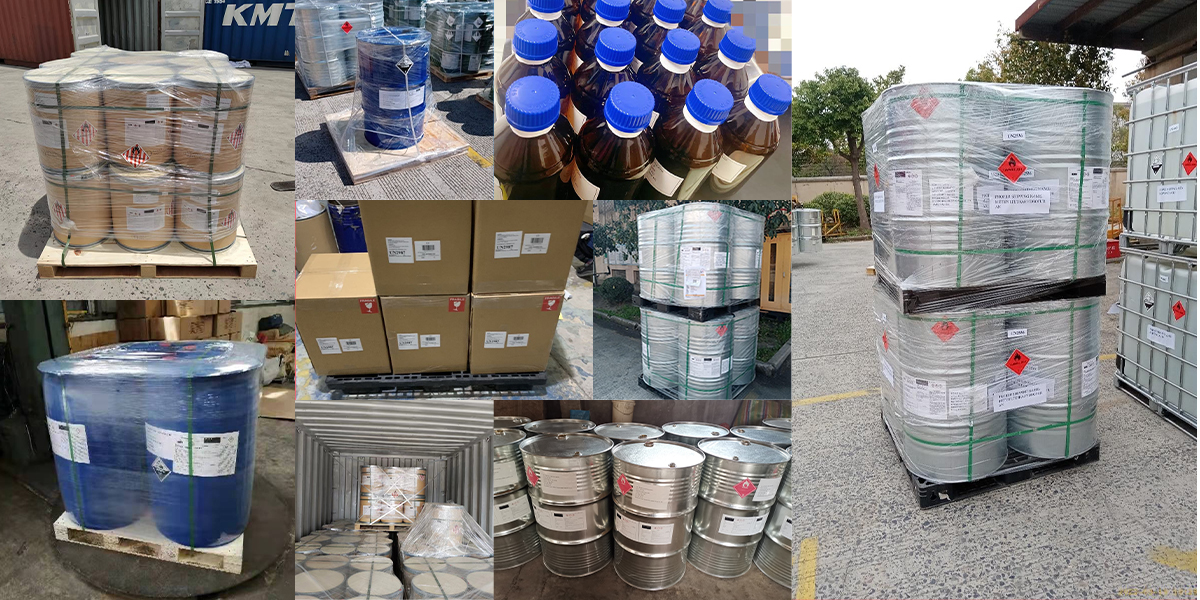
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.