Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
The selection of flame retardants is a critical decision for manufacturers across industries, impacting product safety, regulatory compliance, and environmental responsibility. While traditional flame retardants have served industries for decades, concerns regarding their toxicity and environmental persistence have spurred the development and adoption of advanced alternatives. Zinc borate has emerged as a leading example of such an alternative, offering a compelling blend of performance, safety, and environmental benefits. As a dedicated supplier of specialty chemicals, we aim to provide clarity on why Zinc Borate is often the superior choice for modern applications.
Traditional Flame Retardants: An Overview and Concerns
Historically, halogenated flame retardants (HFRs), particularly brominated compounds (BFRs) and chlorinated compounds, have been widely used due to their effectiveness in interrupting the combustion cycle. They work by releasing halogen radicals that scavenge highly reactive hydrogen and hydroxyl radicals in the flame zone, thus suppressing combustion. However, significant concerns have arisen:
Other traditional inorganic flame retardants, like antimony trioxide, are often used as synergists but also face scrutiny regarding toxicity and environmental impact.
The Advantages of Zinc Borate
Zinc borate, a white crystalline inorganic compound (CAS: 1332-07-6), presents a strong case as a superior alternative. Its advantages stem from its unique chemical structure and decomposition mechanism:
Performance Comparison: Zinc Borate vs. HFRs
While HFRs can be highly effective, their significant health and environmental drawbacks are increasingly outweighing their performance benefits in many applications. Zinc borate offers comparable or even superior flame retardancy and smoke suppression in many systems, particularly when used synergistically, without the associated toxic byproducts. For manufacturers seeking to comply with evolving regulations like RoHS and REACH, or simply aiming for more sustainable and safer product lines, Zinc Borate is the clear choice.
Why Buy Zinc Borate from a Trusted Supplier?
As a leading manufacturer and supplier of specialty chemicals, we ensure our Zinc Borate is produced to the highest purity standards. Choosing our Zinc Borate means opting for a product that delivers excellent fire and smoke performance while adhering to safety and environmental best practices. We provide competitive pricing and reliable supply chain management, making it easier for you to transition to safer, more effective flame retardant solutions. When comparing flame retardant options, make an informed decision based on safety, efficacy, and long-term sustainability. Invest in Zinc Borate for a brighter, safer future.
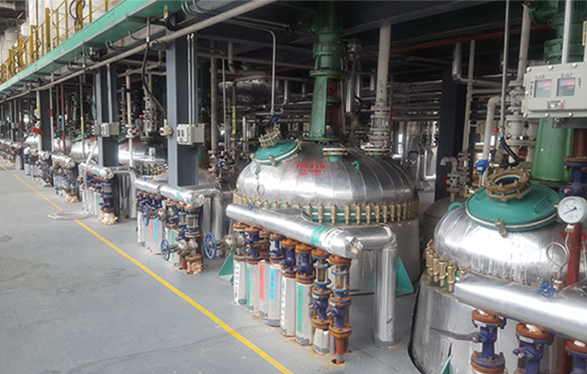
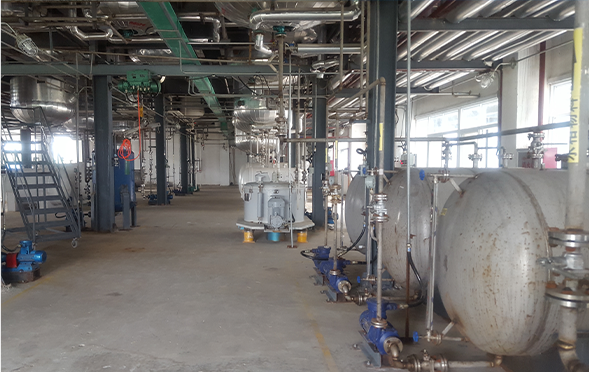
Manufacturing Facilities
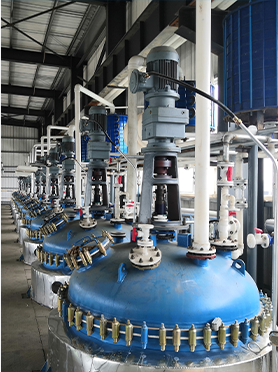
Professional Export Experience
to Global Customers
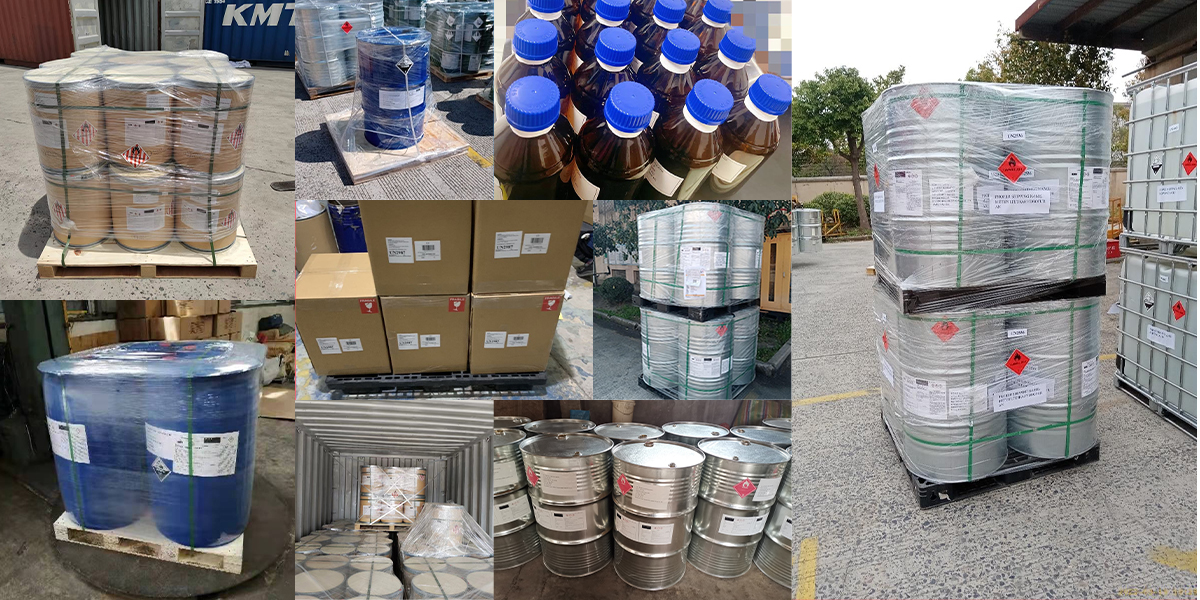
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.