Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
In the intricate world of chemical processing, the choice of materials for catalyst supports can profoundly impact catalyst lifespan, process efficiency, and the purity of the final products. Among the various support materials, high-purity alumina ceramics are highly regarded, largely due to their exceptional chemical inertness. This property ensures that the support material does not participate in or interfere with the desired catalytic reactions. As a dedicated manufacturer and supplier of these critical components, we understand the importance of this characteristic.
The Significance of Chemical Inertness in Catalysis
Chemical inertness refers to a material's resistance to chemical reactions. For catalyst carriers, this means the support should remain chemically unchanged under the specific operating conditions of the reactor. If a carrier is not inert, it can:
Alumina, particularly at high purity levels (e.g., 99% Al2O3), exhibits remarkable chemical inertness across a wide range of temperatures and in the presence of many common reactants and solvents. This makes it an ideal foundation for catalysts used in diverse applications.
How Inertness Enhances Catalyst Longevity and Process Purity
The chemical inertness of our alumina ceramic carriers directly contributes to:
These benefits are critical in applications such as petrochemical refining, gas processing, and the synthesis of high-value chemicals. When you are looking to buy these essential components, partnering with a reputable supplier that guarantees high purity is paramount. Our company, as a leading manufacturer, ensures that our alumina ceramic carriers meet the highest standards of inertness.
Sourcing Chemically Inert Carriers from a Trusted Manufacturer
We understand that the integrity of your catalytic processes depends on the quality of the materials you use. Our high-purity alumina ceramic balls are manufactured with stringent quality control to ensure maximum chemical inertness, mechanical strength, and thermal stability. We offer competitive price structures and reliable delivery to meet the demands of industrial operations worldwide. For businesses seeking to optimize catalyst performance and ensure process purity, our chemically inert alumina ceramic carriers are an excellent choice.
We invite you to contact us for detailed specifications, application guidance, and to request a quotation for our alumina ceramic catalyst carriers. Partner with us for reliable, high-performance solutions.
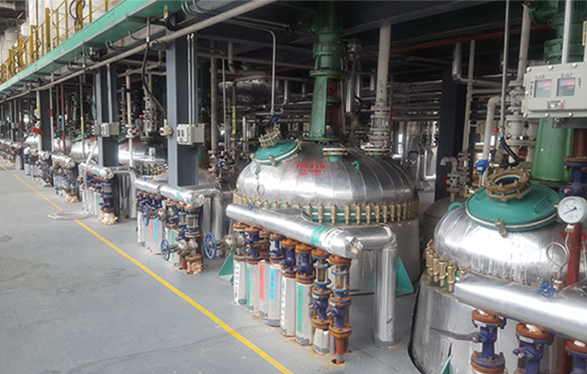
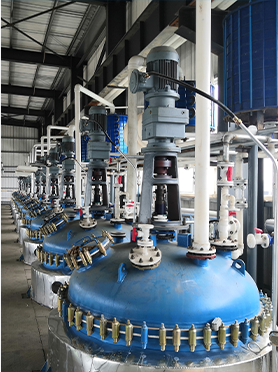
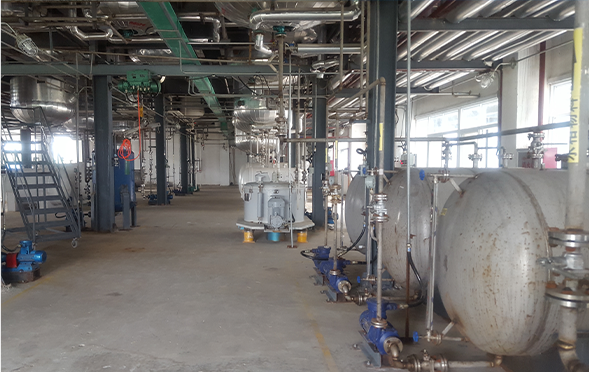
Manufacturing Facilities
Professional Export Experience
to Global Customers
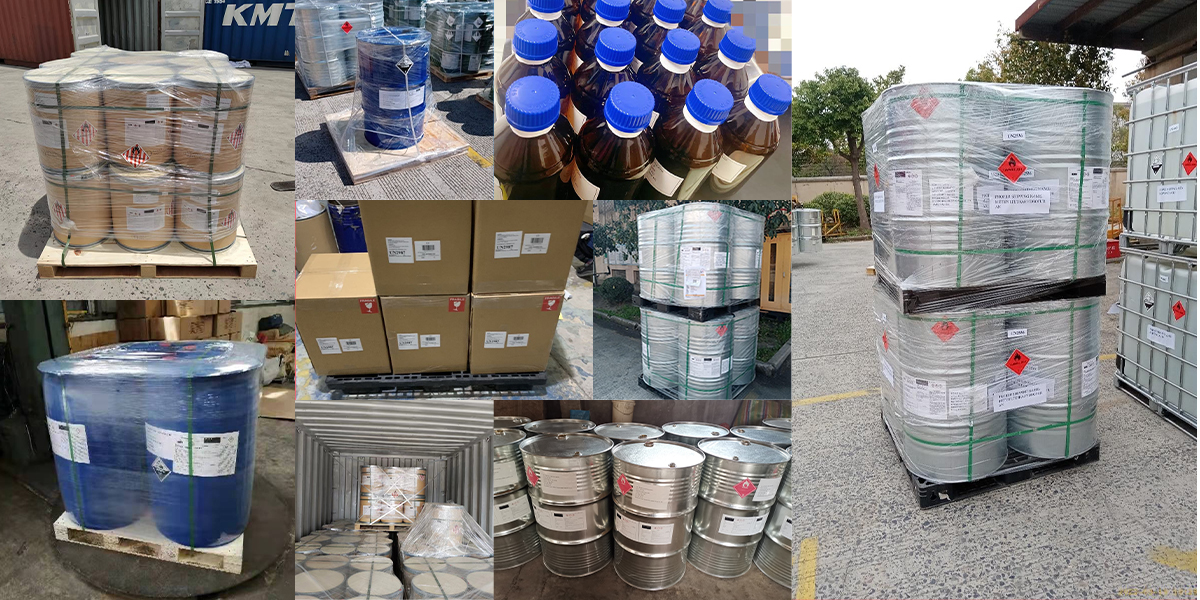
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.