Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
In the realm of industrial chemistry, particularly in catalysis, the physical structure of the support material plays a pivotal role in determining the overall efficiency and effectiveness of the catalyst. Porous ceramic catalyst carriers, such as those made from high-purity alumina, are engineered to provide an optimal environment for chemical reactions. Their unique porous structure offers significant advantages, making them indispensable in numerous applications. As a leading manufacturer and supplier of these specialized materials, we highlight their importance.
What Makes Porous Ceramics Ideal for Catalyst Carriers?
The defining characteristic of these carriers is their carefully controlled porous structure, which comprises interconnected pores. This intricate network provides several critical benefits:
Applications Driving Demand for Porous Carriers
The demand for porous ceramic catalyst carriers is driven by their application in critical industrial processes:
When considering to buy these materials, selecting a reliable supplier is crucial for ensuring the required pore size distribution, surface area, and mechanical integrity. Our company, as a dedicated manufacturer, focuses on producing porous alumina ceramic balls with precisely controlled properties to meet these stringent demands. We offer competitive price points and consistent quality.
Choosing the Right Porous Structure
The specific pore structure required will depend on the catalytic process. Factors such as pore size distribution, pore volume, and pore connectivity are tailored by manufacturers to optimize performance for specific reactions. As a knowledgeable supplier, we can assist you in selecting the most appropriate porous ceramic carrier for your application. Understanding these technical nuances is key for R&D scientists and engineers.
For businesses seeking to improve their catalytic process efficiency, investing in high-quality porous ceramic catalyst carriers is a wise decision. Contact us today to discuss your project needs and to obtain a quotation for our advanced porous ceramic solutions.
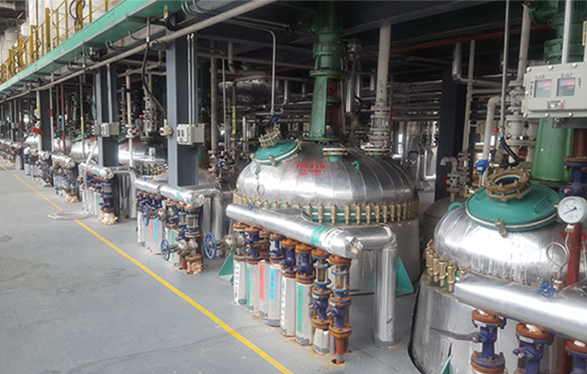
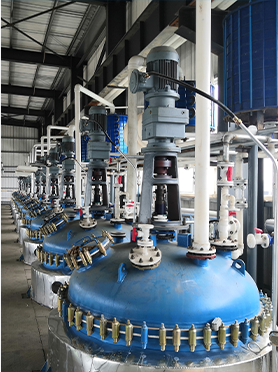
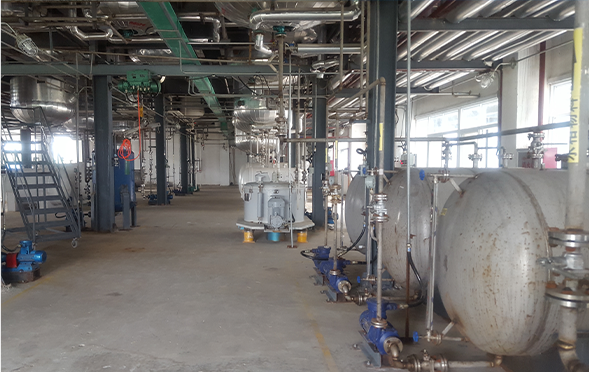
Manufacturing Facilities
Professional Export Experience
to Global Customers
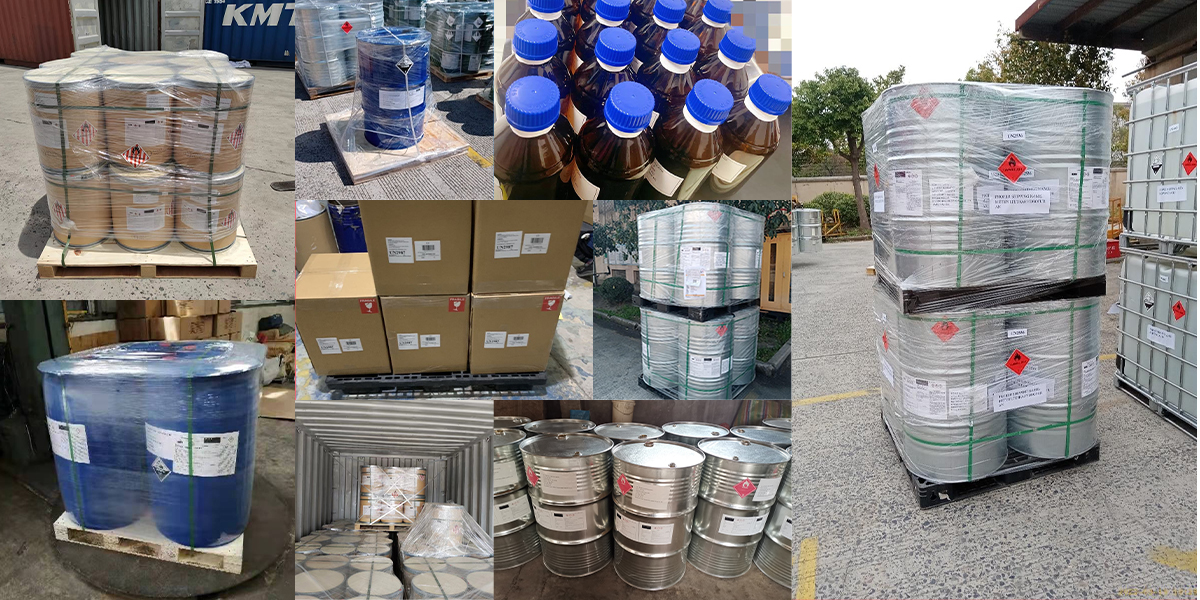
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.