Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
Zeolites, a remarkable group of microporous aluminosilicate minerals, have transitioned from being fascinating geological specimens to indispensable materials across a wide array of industrial applications. Their unique crystalline structure, characterized by a network of precisely sized pores and channels, imbues them with exceptional properties such as high surface area, ion-exchange capacity, and catalytic activity. These attributes make them highly sought after in sectors ranging from petrochemicals to environmental management.
Catalysis: The Engine of Chemical Transformation
One of the most significant industrial applications of zeolites is in catalysis, particularly within the petrochemical industry. Zeolites act as highly selective catalysts in processes like fluid catalytic cracking (FCC), isomerization, and alkylation. Their porous structure allows reactant molecules to enter and react within specific confined spaces, influencing reaction pathways and product selectivity. The ability to tune the pore size and acidity of zeolites by varying their silicon-to-aluminum ratio or through cation exchange allows manufacturers to optimize catalysts for specific chemical transformations, leading to increased yields of valuable products like gasoline and petrochemical feedstocks.
Gas Separation and Purification: Precision in Molecular Sieving
The precisely defined pore sizes of zeolites make them excellent molecular sieves, enabling the separation and purification of gases. This capability is utilized in several critical industrial processes:
The efficiency and selectivity of zeolites in these applications contribute significantly to process optimization and product quality.
Water Treatment and Environmental Remediation: Guardians of Purity
Zeolites are increasingly recognized for their role in environmental protection, particularly in water treatment and soil remediation. Their strong ion-exchange and adsorption capabilities allow them to effectively remove:
As a heavy metal removal solution, zeolites offer a sustainable and often regenerable alternative to chemical precipitation methods. Their application in eco-friendly water treatment aligns with growing environmental consciousness.
Other Notable Industrial Uses:
Sourcing High-Quality Zeolites for Industrial Needs
For industries looking to leverage the versatile properties of zeolites, sourcing from reliable manufacturers is crucial. Companies that specialize in adsorbent materials and have expertise in zeolite synthesis and modification can provide tailored solutions. When seeking to buy zeolites, consider suppliers who can offer:
Partnering with experienced chemical manufacturers, particularly those with robust production capabilities in regions like China, can provide access to a wide range of zeolite products. Understanding the specific needs of your industrial process and aligning them with the capabilities of different zeolite types will ensure successful implementation and optimal results.
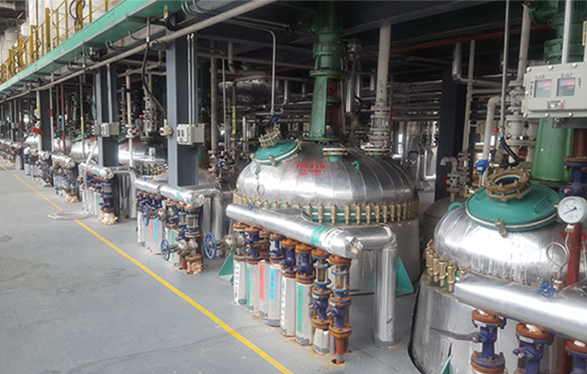
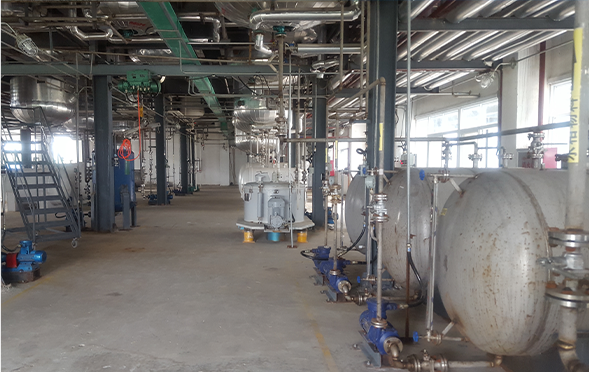
Manufacturing Facilities
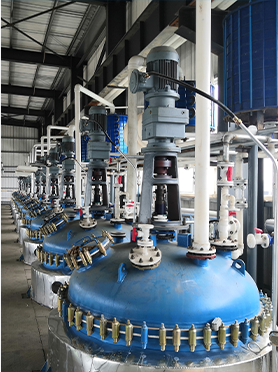
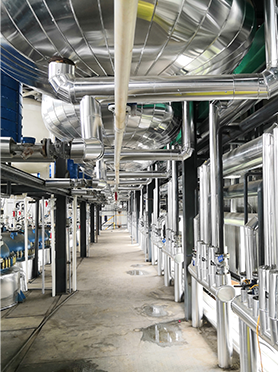
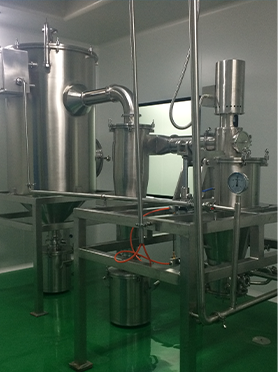
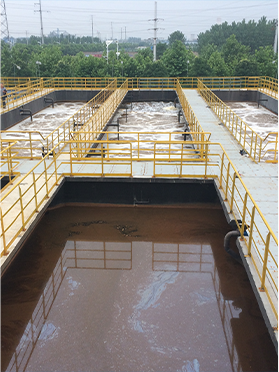
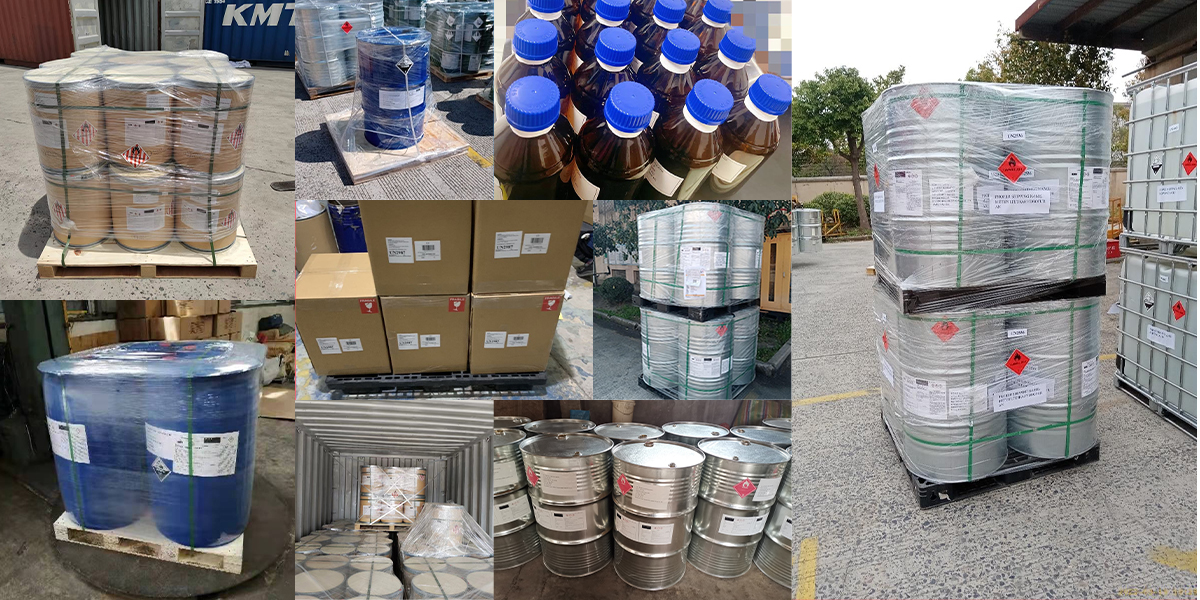
Professional Export Experience
to Global Customers
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.