Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
In the intricate supply chains of the pharmaceutical, agrochemical, and specialty chemical industries, high-purity fine chemical intermediates are foundational building blocks. Their quality, consistency, and reliable availability directly impact the success of downstream manufacturing processes, product efficacy, and regulatory compliance. For procurement managers, navigating the market to secure these essential materials requires a strategic approach focused on quality, cost-effectiveness, and supply chain robustness.
Understanding the Criticality of Fine Chemical Intermediates
Fine chemical intermediates are complex, single, pure chemical substances that are produced through sophisticated multi-step synthesis processes. They serve as precursors in the synthesis of Active Pharmaceutical Ingredients (APIs), pesticides, dyes, and other specialized chemicals. The purity and precise chemical structure of these intermediates are paramount. Even minor impurities can lead to:
Therefore, the procurement of these materials necessitates a deep understanding of chemical synthesis, quality control, and global sourcing best practices.
Key Factors in Procuring Fine Chemical Intermediates
When engaging in the procurement of fine chemical intermediates, several critical factors must be considered:
Navigating the Global Market: Sourcing Strategies
The global market for fine chemical intermediates is dynamic. Identifying and vetting potential suppliers is a continuous process. Key sourcing strategies include:
When you are ready to buy fine chemical intermediates, prioritize suppliers who demonstrate a commitment to quality, transparency, and customer service. Manufacturers who offer custom synthesis services can be invaluable for highly specific or novel intermediate requirements.
By implementing a rigorous procurement process that emphasizes technical due diligence, supplier reliability, and a strategic sourcing approach, organizations can secure the high-purity fine chemical intermediates necessary to drive innovation and maintain competitive advantage in their respective industries.
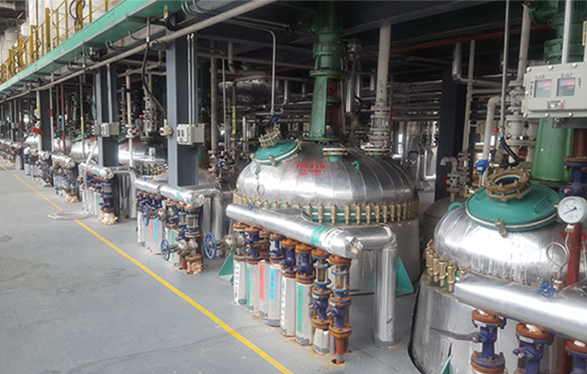
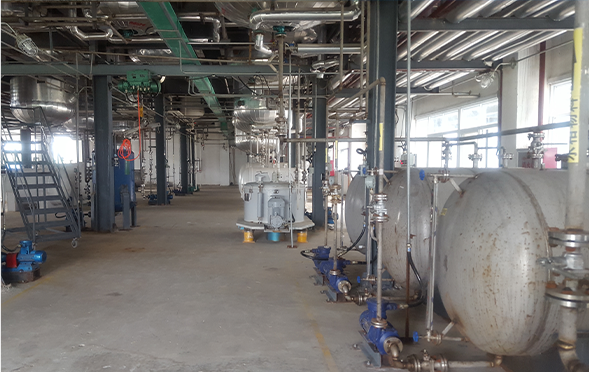
Manufacturing Facilities
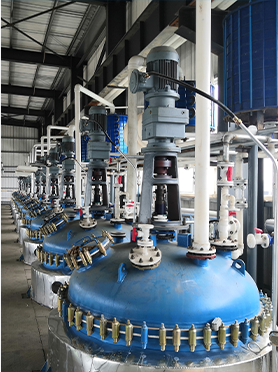
Professional Export Experience
to Global Customers
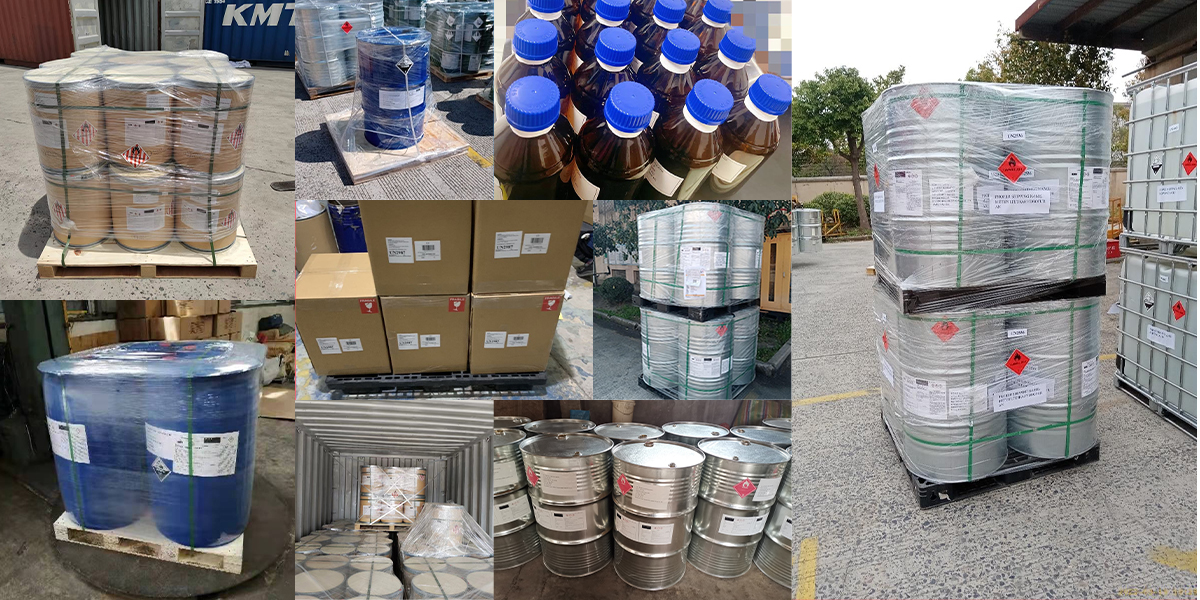
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.