Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
In the ongoing pursuit of safer and more sustainable materials, the chemical industry has increasingly focused on developing effective halogen-free flame retardant systems. Among the leading compounds in this field is zinc borate. As a premier supplier, NINGBO INNO PHARMCHEM CO.,LTD. recognizes the critical importance of this versatile additive. This article delves into the significant role zinc borate plays in creating robust halogen-free flame retardant solutions, essential for a wide array of applications.
Traditional flame retardants often rely on halogenated compounds, which, while effective, can release toxic and corrosive gases when exposed to fire. This poses significant risks to human health and the environment. Zinc borate, on the other hand, offers a compelling alternative. It is a non-toxic, inorganic compound that achieves flame retardancy through a unique mechanism. When materials containing zinc borate are heated, the compound releases water molecules. This endothermic process absorbs heat energy, cooling the material. Simultaneously, the released water vapor dilutes flammable gases in the vicinity of the flame, further suppressing combustion. The decomposition also leaves behind a protective char layer, often a glassy boron oxide matrix, which acts as a barrier against oxygen and heat, preventing the material from igniting or spreading flames. This makes zinc borate a cornerstone for manufacturers seeking to buy zinc borate for plastics and other polymers that require high safety standards.
Furthermore, zinc borate exhibits remarkable synergistic effects when combined with other flame retardant additives. For instance, it works exceptionally well with intumescent systems, ammonium polyphosphate, magnesium hydroxide, and alumina trihydrate. This synergy means that a lower overall loading of additives can be used to achieve desired fire performance, leading to cost efficiencies and minimal impact on the base material's mechanical properties. This enhances the overall value proposition for industries utilizing industrial grade zinc borate. The ability to achieve superior fire safety without compromising material integrity is a key advantage. For those looking to procure these advanced materials, understanding the zinc borate mechanism of action is paramount.
The application of zinc borate extends across numerous sectors. In the plastics industry, it is widely adopted in PVC, polyolefins, polyamides, and epoxy resins to enhance their fire resistance. It also finds utility in textiles, paper, rubber, and coatings, where its properties contribute to improved fire safety and reduced smoke emission. The compound’s efficacy as a zinc borate smoke suppressant is particularly valued in applications where visibility and air quality during a fire are critical. Moreover, beyond its primary role as a flame retardant, zinc borate also possesses fungicidal properties, making it beneficial for wood preservation and in certain plastics formulations requiring protection against microbial degradation. This dual functionality adds significant value for end-users.
At NINGBO INNO PHARMCHEM CO.,LTD., we are committed to providing high-quality zinc borate that meets the stringent demands of modern industries. Our product is a reliable solution for manufacturers aiming to develop safer, more sustainable products. By choosing our zinc borate, companies can ensure compliance with environmental regulations and enhance the fire performance of their materials. Exploring the benefits of zinc borate is a step towards achieving next-generation material safety. We offer competitive pricing and reliable supply, solidifying our position as a trusted flame retardant additive supplier.
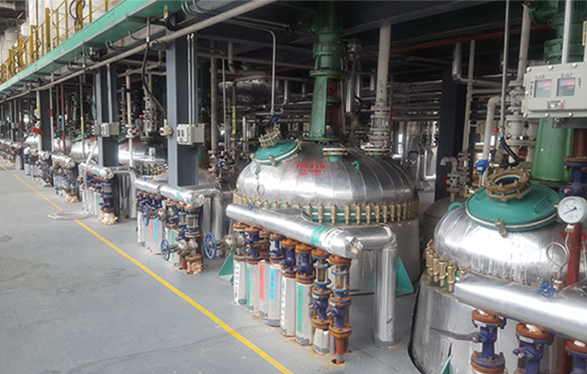
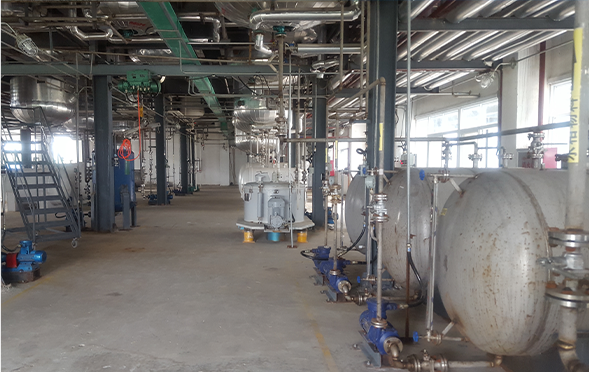
Manufacturing Facilities
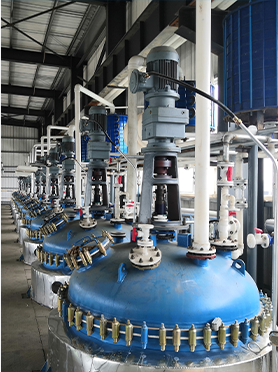
Professional Export Experience
to Global Customers
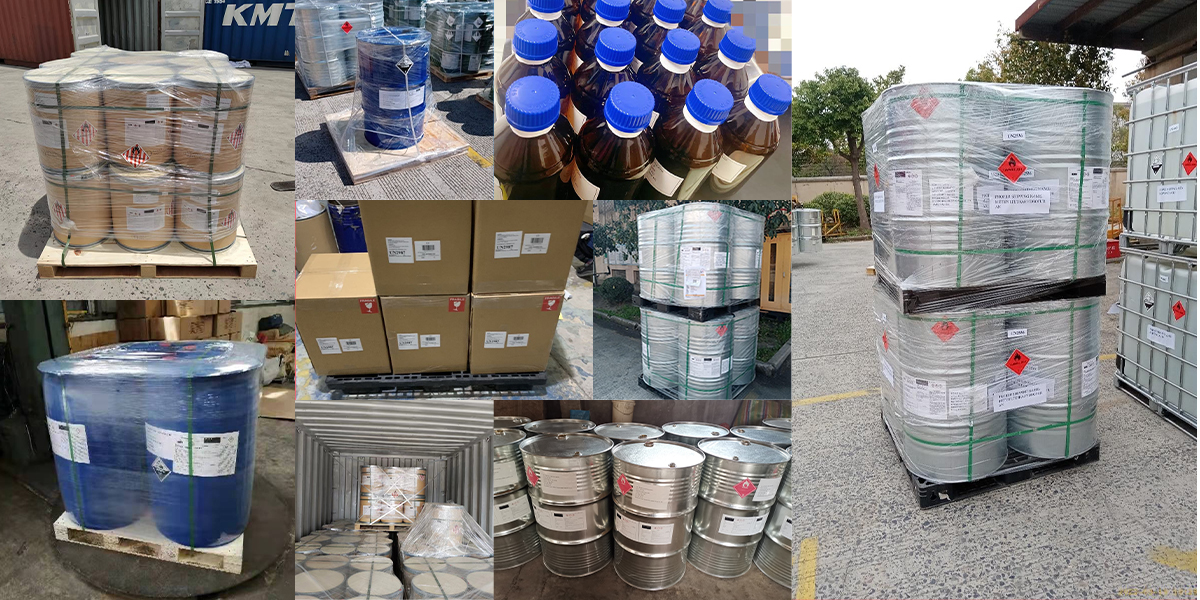
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.