Custom Manufacturing, Project Outsourcing, your Trusted Partner from China
Fire safety is a paramount concern across countless industries, and the selection of appropriate flame retardants is crucial for ensuring product integrity and protecting lives. Zinc borate has emerged as a highly effective and versatile additive, prized for its ability to enhance material resistance to fire and suppress smoke. NINGBO INNO PHARMCHEM CO.,LTD. is dedicated to providing advanced chemical solutions, and understanding the zinc borate mechanism of action is key to appreciating its value. This article explores the science behind zinc borate's efficacy as a flame retardant.
The primary mode of action for zinc borate as a flame retardant involves a multi-stage process triggered by heat. Initially, upon exposure to elevated temperatures, zinc borate undergoes dehydration. This process involves the release of water molecules. These molecules have a cooling effect on the substrate material by absorbing heat (endothermic reaction) and by diluting flammable gases in the vapor phase. The released water vapor also helps to reduce the concentration of oxygen available to the flame. As the dehydration progresses, zinc borate transforms into a glassy phase, primarily boron oxide. This glassy layer forms a protective barrier on the surface of the material. This barrier insulates the underlying polymer from heat and oxygen, preventing further degradation and combustion. This makes it an excellent choice for those looking to buy zinc borate for plastics and other polymer applications where fire resistance is critical.
One of the significant advantages of zinc borate is its synergistic capability. It can enhance the performance of other flame retardants, allowing for lower overall additive concentrations and improved cost-effectiveness. For instance, when combined with halogenated flame retardants, zinc borate can improve char formation and reduce smoke. In halogen-free systems, it synergizes effectively with compounds like ammonium polyphosphate (APP) and magnesium hydroxide (MDH). This synergistic effect is vital for formulating materials that meet stringent fire safety regulations without compromising mechanical properties or introducing unwanted side effects. Manufacturers seeking reliable industrial grade zinc borate often rely on this synergistic potential.
The impact of zinc borate extends beyond simple flame retardation. It also acts as an anti-dripping agent in some polymers, preventing molten material from dripping and spreading the fire. Furthermore, zinc borate is recognized for its smoke suppression properties. By promoting char formation and influencing the decomposition pathway of the polymer, it helps to reduce the amount of smoke generated during combustion. This is particularly important in applications where visibility and air quality are critical, such as in building materials and transportation. The ability to serve as a zinc borate smoke suppressant adds another layer of safety to its profile.
NINGBO INNO PHARMCHEM CO.,LTD. is a leading flame retardant additive supplier, offering high-purity zinc borate that delivers exceptional performance. Our commitment to quality ensures that our clients receive materials that meet the highest industry standards. By leveraging the unique properties and mechanisms of zinc borate, manufacturers can develop safer, more compliant, and environmentally responsible products. Understanding the intricate ways zinc borate works is the first step towards unlocking its full potential in material science and fire safety.
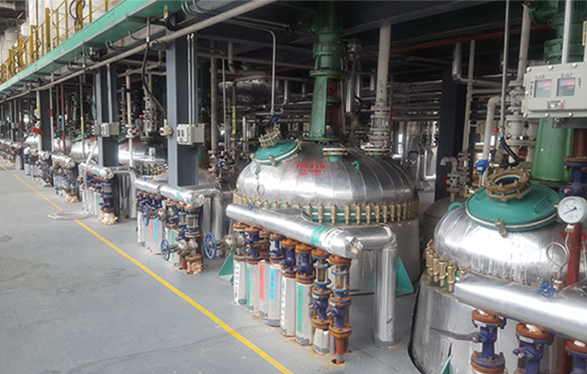
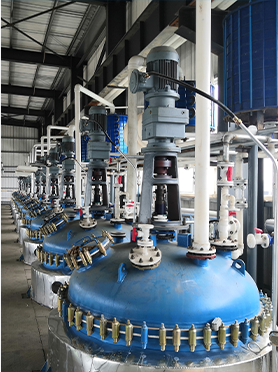
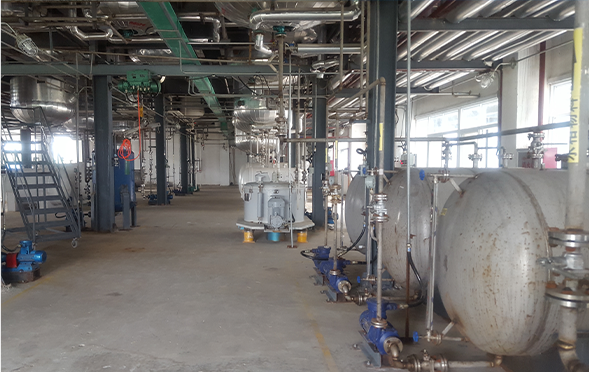
Manufacturing Facilities
Professional Export Experience
to Global Customers
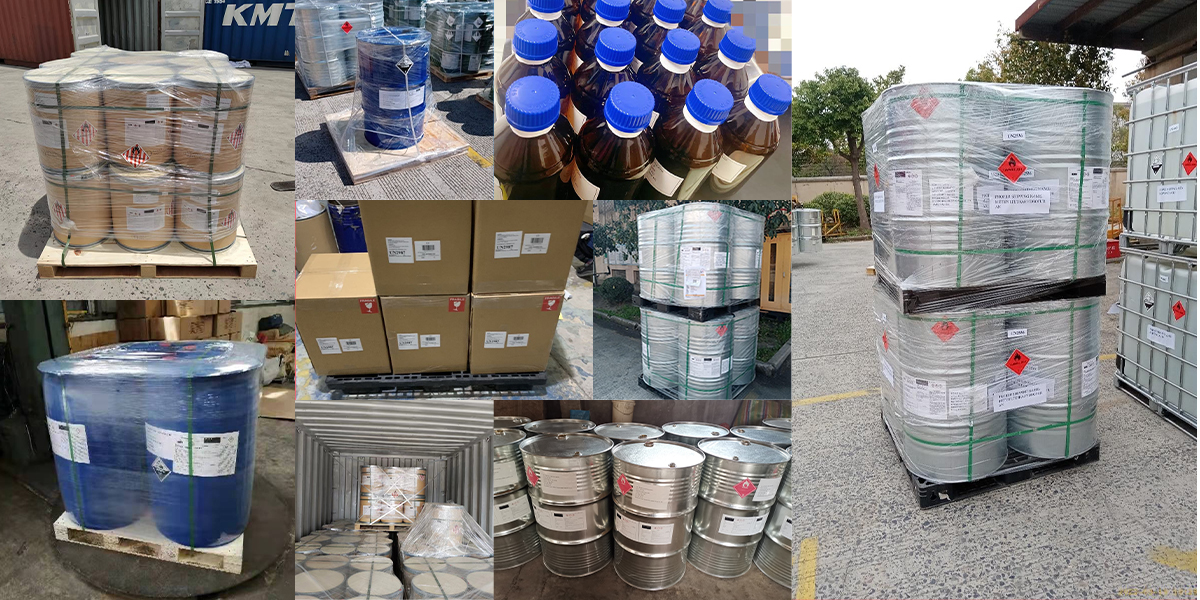
1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;
2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;
3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).
A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.
A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.
A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.