20 YEARS OF PROFESSIONAL & DEDICATED SERVICE TO GLOBAL CUSTOMERS

Custom Manufacturing, Project Outsourcing, your Trusted Partner from China

The Role of Zeolite as a Chemical Auxiliary Agent

In the realm of industrial chemistry and manufacturing, the selection of auxiliary agents can significantly impact process efficiency, product quality, and environmental compliance. Natural zeolite, with its unique physicochemical properties, has proven to be an invaluable chemical auxiliary agent across a spectrum of applications. As a specialized supplier of industrial raw materials, we highlight the diverse roles zeolite plays in enhancing chemical processes.

Zeolite: A Multifunctional Chemical Auxiliary

Zeolite's versatility stems from its distinctive structural and chemical characteristics:

  • Adsorbent: The porous nature of zeolite makes it an excellent adsorbent for various molecules. In chemical processes, it can be used to remove impurities, separate specific components from mixtures, or act as a drying agent. Its selectivity allows for targeted removal of unwanted substances, improving the purity of reaction products.
  • Catalyst and Catalyst Support: The high surface area and tunable acidity of zeolites make them effective catalysts or supports for catalysts in many chemical reactions, including petrochemical processes, organic synthesis, and environmental catalysis. They can facilitate reactions, increase reaction rates, and improve selectivity towards desired products.
  • Carrier Agent: Zeolite's porous structure can encapsulate and deliver active ingredients in a controlled manner. This property is utilized in applications such as slow-release fertilizers, controlled drug delivery systems, and the stabilization of sensitive chemical compounds.
  • Ion Exchanger: As previously discussed in the context of water treatment, zeolite's ion-exchange capability can be leveraged in chemical manufacturing to remove specific ions from process streams or to recover valuable metals.

Industrial Applications of Zeolite as an Auxiliary Agent

The utility of zeolite as a chemical auxiliary is broad:

  • Petrochemical Industry: Zeolites are critical in catalytic cracking and refining processes, breaking down crude oil into valuable gasoline and other products.
  • Gas Separation and Purification: They are used for separating gases, such as removing CO2 or water vapor from natural gas, and in air separation units for producing oxygen and nitrogen.
  • Environmental Catalysis: Zeolites are employed in catalytic converters in vehicles to reduce harmful emissions and in industrial settings for treating exhaust gases.
  • Detergent Manufacturing: As water softeners, they enable detergents to work effectively in hard water areas.
  • Adhesives and Coatings: Zeolites can be incorporated into formulations to control viscosity, improve adhesion, or act as functional fillers.

Reliable Supply for Your Industrial Needs

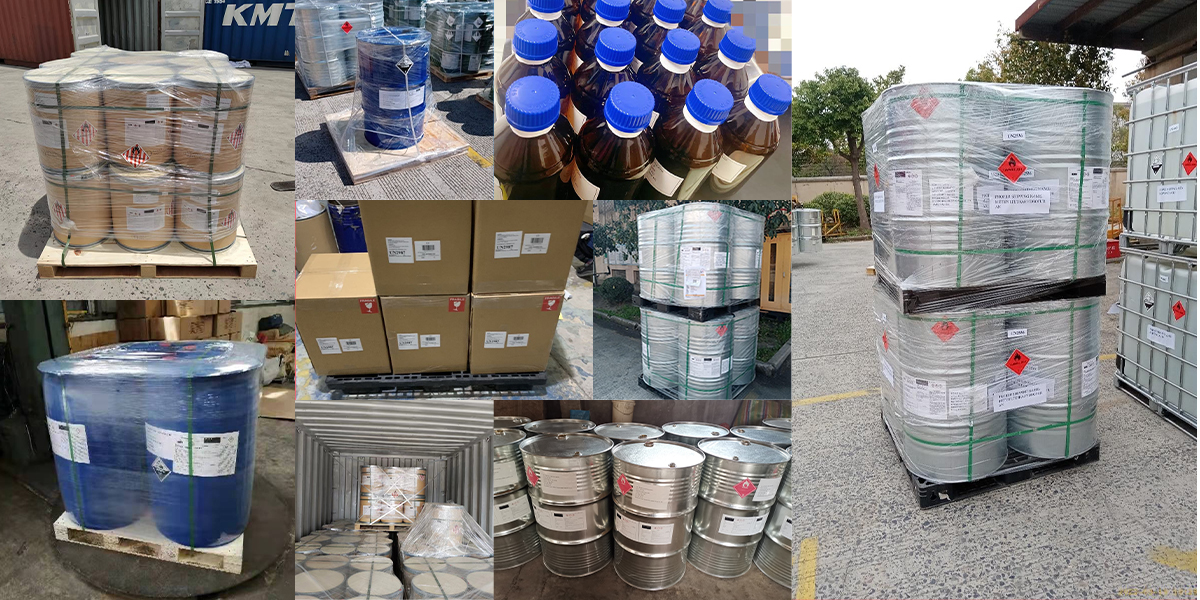
For businesses relying on chemical auxiliary agents, sourcing high-quality and consistent materials is essential. We offer natural zeolite powder that meets rigorous industrial standards, ensuring reliable performance in your manufacturing processes. Our commitment as a manufacturer in China means we can provide competitive pricing and dependable bulk supply. We welcome inquiries from purchasing managers and R&D scientists looking for advanced chemical solutions.

We encourage you to contact us to discuss your specific application requirements, request product samples, and obtain a quotation. Partner with us to integrate the benefits of zeolite into your chemical processes and achieve enhanced operational efficiency and product quality.

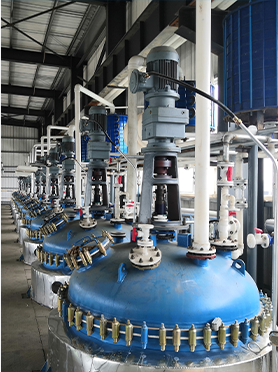
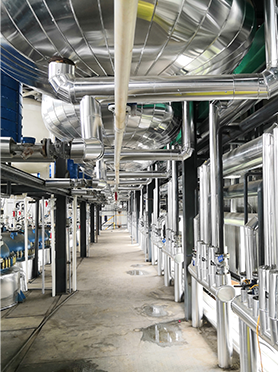
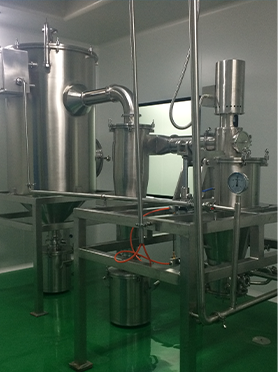
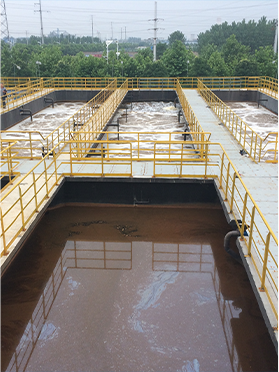
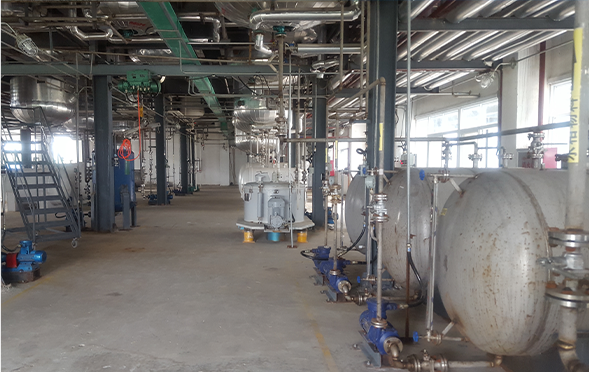
Manufacturing Facilities
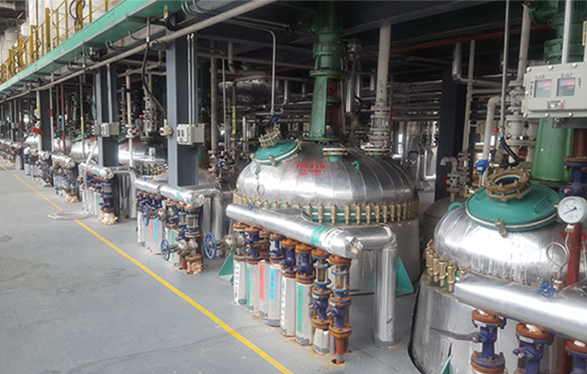
NINGBO INNO PHARMCHEM CO.,LTD. was established in 2007. It is committed to the R&D, production and sales of raw materials, pharmaceutical intermediates and fine chemicals. We striving to create a high-efficiency and high-quality integrated chemical service platform to better serve domestic and foreign customers.

Professional Export Experience

to Global Customers
WHY CHOSE US?

1. 20 years of R&D, manufacturing and sales experience, serving customers in 60 countries and regions around the world;

2. Own R&D laboratory, pilot platform and large-scale production workshop, which can meet the audit requirements of global customers;

3. We can satisfy customers' perfect transition from small scale lab requirements (gram level) to commercialization requirements (hundred tons level).

FAQ

  • A: We don't have Minimum Order Quantity, exact quantity should be provided before quotation for us to calculate the exact cost.

  • A: We don't provide free samples due to lots of request and expensive international courier's cost, we can deduct the sample charge after commercial order placed.

  • A: Our payment terms: Small or sample order: T/T IN ADVANCE. Commercial order: First order should be by T/T IN ADVANCE or L/C at sight, and following orders T/T 30~90days is acceptable subject to approval of credit application.
CONTACT US
Should you need to contact us; you may call during regular business hours, Monday through Friday, 8am – 6 pm.
NINGBO INNO PHARMCHEM CO.,LTD.
Address: No.163 Ruiqing Rd.,Ningbo 315000 China
Phone: 86-574-87319282
Fax: 86-574-27912196
SEND US AN EMAIL

NAME*

EMAIL*

COMPANY

COUNTRY*

MESSAGE*

Previous: Zeolite for Agriculture: Enhancing Soil and Crops

Next: Comparing Zeolite and Activated Carbon in Water Filtration

All Rights Reserved